Metering bin pumps are specialized equipment used in bulk material handling systems to accurately measure and transport powders or granular materials. These devices play a crucial role in industries such as cement, chemical, and food processing, where precise control over material flow is essential for efficiency and product quality. Understanding the fundamental concepts of metering bin pump material handling, along with its underlying design principles, is vital for engineers and operators seeking to optimize their processes.
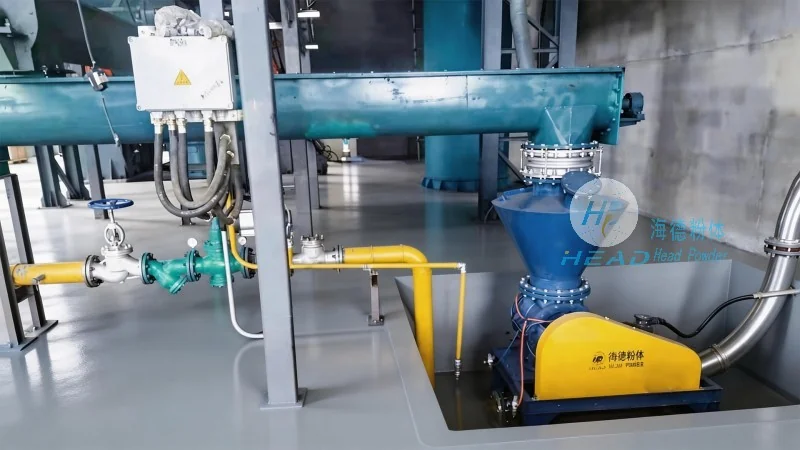
Metering bin pumps, also known as bin activators or feeder pumps, are designed to transfer bulk materials from storage silos or hoppers into processing equipment. The core function of these systems is to provide a controlled, consistent flow of material, ensuring that downstream processes receive the exact quantity needed. This is achieved through a combination of mechanical components, including a hopper, a discharge valve, and a metering mechanism. The metering mechanism typically operates by rotating or vibrating the material, which allows for precise control over the rate of discharge. This technology is particularly valuable in applications where overfeeding or underfeeding can lead to significant operational issues, such as equipment damage or product defects.
The design of metering bin pumps is based on several key principles to ensure reliable and accurate material handling. First, the equipment must maintain a consistent pressure within the hopper to prevent material bridging or caking, which can disrupt the flow. This is often achieved through the use of a pressure relief valve or a venting system. Second, the metering mechanism must be capable of handling a wide range of material properties, including different particle sizes, densities, and flow characteristics. This flexibility is critical for accommodating various materials, from fine powders to coarse granules. Third, the system must be designed for easy maintenance and cleaning to prevent contamination and ensure long-term performance. Regular maintenance, such as checking the condition of the discharge valve and the integrity of the hopper lining, is essential to maintain optimal operation.
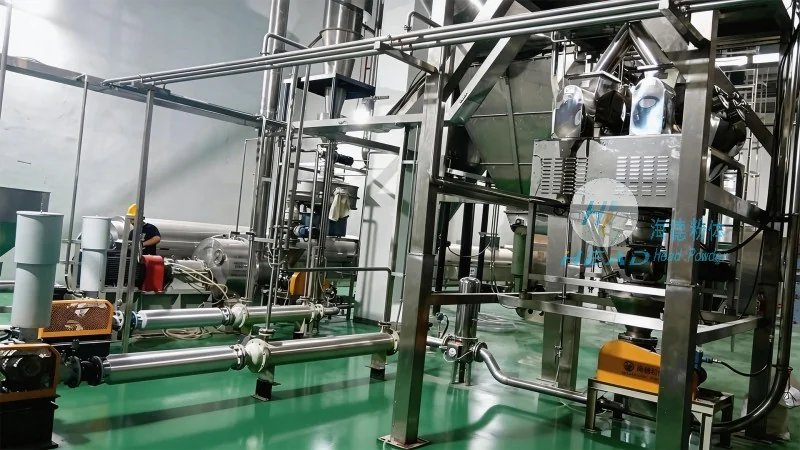
Several key components work together to enable the effective operation of metering bin pumps. The hopper is the primary container for the bulk material and is typically designed with a conical or rectangular shape to facilitate material flow. The discharge valve, often a rotary or slide valve, controls the opening and closing of the outlet, regulating the flow rate. The metering mechanism, which may include a screw, paddle, or vibrating mechanism, ensures that the material is discharged at a controlled rate. Additionally, a level sensor or a weight indicator may be integrated to monitor the material level in the hopper, providing feedback to the control system. This feedback loop allows for automatic adjustment of the discharge rate, ensuring that the system operates efficiently and consistently.
Metering bin pumps are widely used in various industries due to their ability to handle a diverse range of materials. In the cement industry, these systems are used to feed raw materials and clinker into rotary kilns, ensuring a steady supply for production. In the chemical industry, they are employed to transport powders and granules for mixing, reactions, or packaging. The food processing industry also benefits from metering bin pumps, as they can handle ingredients like flour, sugar, and spices with precision, maintaining product quality and safety standards. Additionally, in the pharmaceutical industry, these systems are used to transport raw materials and finished products with high accuracy, meeting stringent regulatory requirements.
Implementing metering bin pump systems offers several advantages over traditional material handling methods. First, they provide precise control over material flow, reducing the risk of overfeeding or underfeeding, which can lead to equipment wear and product defects. Second, these systems improve process efficiency by ensuring a consistent supply of materials, minimizing downtime and increasing production throughput. Third, metering bin pumps are designed for durability and reliability, with components that can withstand harsh operating conditions, such as high temperatures or corrosive environments. This reduces maintenance costs and extends the lifespan of the equipment. Finally, the ability to integrate with automated control systems allows for real-time monitoring and adjustment, enhancing overall process control and safety.
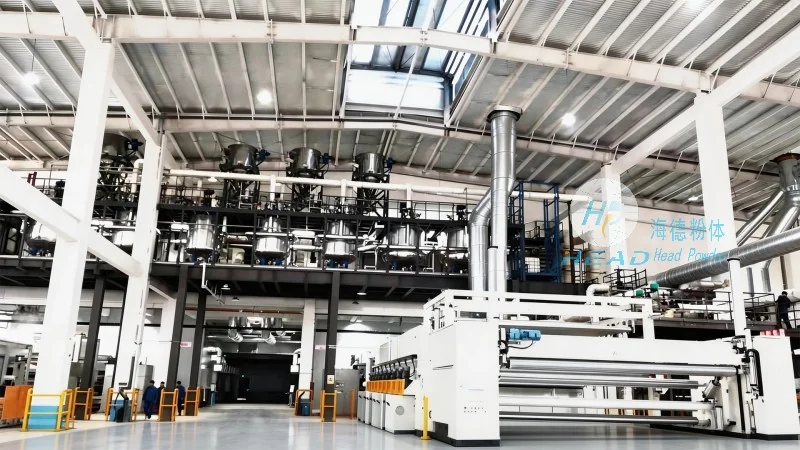
When selecting a metering bin pump system, several factors must be considered to ensure optimal performance. First, the material properties, including particle size, density, and flowability, must be evaluated to determine the appropriate type of metering mechanism. For example, cohesive or sticky materials may require a vibrating mechanism to prevent bridging, while free-flowing materials may use a screw or paddle mechanism. Second, the system must be sized to handle the required flow rate and material volume, ensuring that it can meet production demands without overloading. Third, the operating environment, such as temperature and humidity, should be considered to select materials that are resistant to corrosion or wear. Additionally, the integration with existing equipment and control systems should be evaluated to ensure compatibility and ease of operation.
Metering bin pump material handling is a critical technology in bulk material processing, offering precise control and efficient operation. The design principles behind these systems, including consistent pressure maintenance, material flexibility, and easy maintenance, ensure reliable performance across various industries. By understanding the components and applications of metering bin pumps, engineers and operators can optimize their processes, improve product quality, and reduce operational costs. As a leading manufacturer in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in providing high-quality metering bin pump systems tailored to the specific needs of different industries, ensuring that clients achieve their material handling goals with precision and efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top