For businesses in the malt processing industry, efficient material handling is critical to maintaining production flow and ensuring product quality. Malt pneumatic conveying systems offer a reliable solution for transporting malt from storage silos to processing equipment, such as mashing tanks or drying ovens. These systems use air or gas to move the material through a network of pipes, eliminating the need for mechanical components like conveyor belts or buckets. This approach not only reduces maintenance costs but also minimizes product contamination and degradation, making it an ideal choice for handling delicate malt.
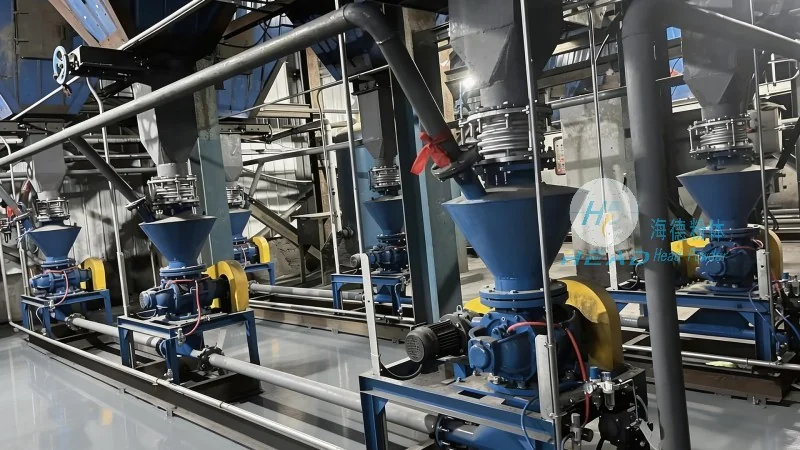
HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is a leading engineering company based in Shandong, China. With a strong focus on the malt processing sector, HeadPowder specializes in designing, manufacturing, and installing pneumatic conveying systems tailored to the unique requirements of malt production. The company’s team of experienced engineers and technicians leverages advanced technology and industry best practices to deliver high-quality solutions that meet or exceed client expectations. HeadPowder’s commitment to quality and customer satisfaction has established it as a trusted partner in the industry.
The successful design of a malt pneumatic conveying system involves careful consideration of several technical and operational factors. The first step is selecting the appropriate conveying method. Malt is typically a dry, free-flowing material with a particle size ranging from 2 to 10 millimeters. Positive pressure systems, which use a blower to force air and material through the pipeline, are commonly used for malt due to their ability to handle abrasive particles and prevent product degradation. Negative pressure systems, on the other hand, are suitable for applications where dust control and environmental compliance are priorities, as they draw material into the system and filter the air before release.
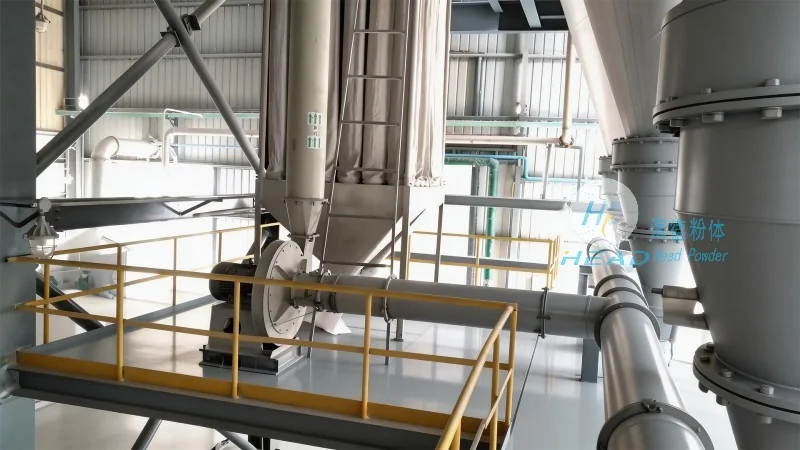
Material selection for the system components is another critical design aspect. Malt is a food product, and the conveying system must be constructed from materials that are non-toxic, corrosion-resistant, and easy to clean. Stainless steel (specifically 304 or 316 grade) is the preferred material for the hopper, pipeline, and other components, as it provides durability, resistance to chemical attack, and excellent hygiene properties. The use of stainless steel also facilitates compliance with food safety regulations, such as those set by the FDA and EU. Additionally, the selection of appropriate valves, such as rotary airlocks and check valves, is essential to prevent backflow and maintain consistent flow rates.
System layout and integration are vital to ensuring efficient operation. The placement of the storage silo, hopper, and processing equipment must be optimized to minimize material handling distances and reduce energy consumption. For example, positioning the hopper near the processing equipment can reduce the length of the pipeline, which in turn lowers the required air pressure and energy usage. Proper sealing of the system is also crucial to prevent dust emissions and maintain a clean working environment. HeadPowder’s engineers use computational fluid dynamics (CFD) and other simulation tools to model the system and identify potential areas of high pressure drop or dust leakage, allowing for adjustments to be made during the design phase.
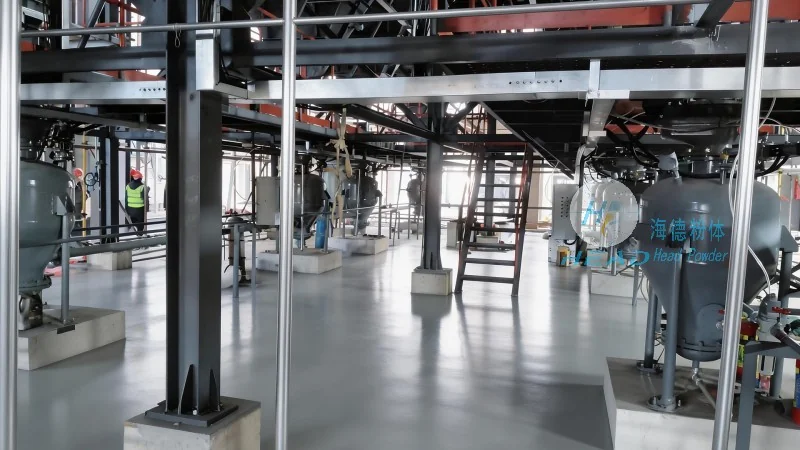
Control systems play a significant role in the operation and maintenance of malt pneumatic conveying systems. Modern systems often incorporate advanced control technology, including PLCs (Programmable Logic Controllers) and SCADA (Supervisory Control and Data Acquisition) systems. These systems allow for real-time monitoring of key parameters such as pressure, flow rate, and temperature, enabling operators to make adjustments quickly and respond to any issues that may arise. The integration of sensors, such as pressure transducers and flow meters, provides accurate data for process optimization and troubleshooting. Additionally, automated alarm systems can be implemented to alert operators of potential problems, such as blockages or pressure drops, ensuring timely intervention and minimizing downtime.
Energy efficiency is a key consideration in the design of any pneumatic conveying system. HeadPowder focuses on optimizing system design to minimize energy consumption while maintaining performance. This includes selecting the appropriate air compressor, which should be sized to meet the system’s demand without excess capacity. The use of variable frequency drives (VFDs) for the blower motor allows for adjustable speed control, enabling the system to operate at lower speeds when lower flow rates are required, thus reducing energy consumption. Proper pipeline sizing is also critical; oversized pipelines can lead to unnecessary energy waste, while undersized pipelines may cause excessive pressure drop and reduced flow. HeadPowder’s engineers use detailed calculations and simulations to determine the optimal pipeline diameter and length for each application.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top