Light Calcium Carbonate Powder Conveying System Equipment: Understanding the Equipment and Its Desig
Release time:2026-09-15 19:01:15
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Manager Zhang
Light calcium carbonate powder conveying systems are essential in industrial applications where the efficient handling and transportation of fine powders like light calcium carbonate are required. These systems are designed to ensure reliable, safe, and efficient material transport, which is crucial for maintaining production efficiency and product quality in various industries.
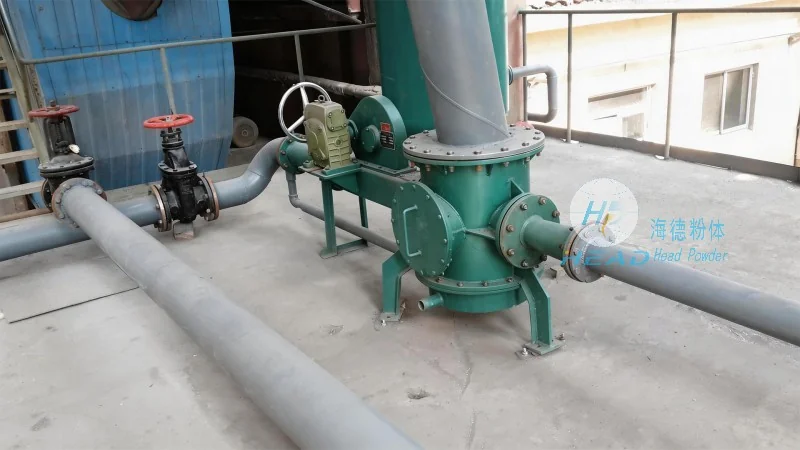
What is a Light Calcium Carbonate Powder Conveying System Equipment?
A light calcium carbonate powder conveying system equipment typically refers to a set of machinery and components used to transport light calcium carbonate powder from one location to another within a production facility or between different stages of a manufacturing process. The equipment may include components such as feeders, conveyors, dust collectors, and control systems, all working together to ensure the smooth and continuous movement of the powder. The primary goal of such a system is to minimize material loss, prevent contamination, and maintain consistent flow rates, which are critical for downstream processes that rely on the uniform handling of light calcium carbonate.
Key Components of the Light Calcium Carbonate Powder Conveying System
The light calcium carbonate powder conveying system consists of several key components that work in tandem to achieve efficient material transport. These components include:
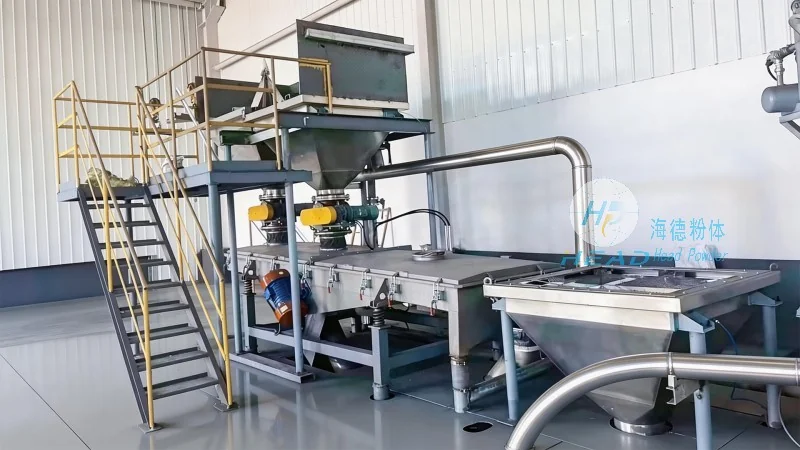
- Feeders: Feeders are used to control the flow rate of the light calcium carbonate powder from the storage hopper or silo into the conveying system. They ensure a consistent and controlled feed, preventing overloading or underloading of the conveyor.
- Conveyors: Conveyors are the core of the system, responsible for moving the light calcium carbonate powder through the system. Common types include pneumatic conveyors (air-powered) and mechanical conveyors (belt or screw conveyors), each with its own advantages depending on the specific application requirements.
- Dust Collectors: Dust collectors are essential for maintaining a clean and safe working environment by capturing and filtering airborne particles of light calcium carbonate. They help prevent dust accumulation, which can be a fire hazard and reduce the efficiency of the conveying system.
- Control Systems: Modern light calcium carbonate powder conveying systems often include advanced control systems that monitor and regulate the operation of the equipment. These systems can adjust flow rates, detect blockages, and alert operators to potential issues, ensuring optimal performance and minimizing downtime.
Design Principles for Light Calcium Carbonate Powder Conveying Systems
The design of a light calcium carbonate powder conveying system is based on several fundamental principles aimed at maximizing efficiency, safety, and reliability. The key design principles include:
- Material Compatibility: The system components must be compatible with light calcium carbonate powder to prevent chemical reactions or material degradation. Materials such as stainless steel, polyethylene, or special coatings are often used to ensure durability and resistance to the powder's properties.
- Flow Optimization: The design focuses on optimizing the flow of light calcium carbonate powder to minimize friction and pressure losses. This involves selecting appropriate conveyor types, maintaining proper incline angles, and ensuring smooth transitions between components to prevent material buildup or blockages.
- Airflow Management: For pneumatic conveying systems, proper airflow management is critical. The system must be designed to provide sufficient air pressure and volume to move the powder efficiently while minimizing energy consumption. This involves calculating the required air velocity and pressure based on the powder's properties and system length.
- Prevention of Agglomeration: Light calcium carbonate powder can tend to agglomerate, which can cause blockages in the conveying system. Design measures such as using agitators, vibration devices, or air knives are incorporated to break up agglomerates and maintain a free-flowing powder.
- Environmental and Safety Considerations: The design must adhere to environmental and safety regulations. This includes incorporating dust collection systems to control emissions, ensuring proper ventilation, and using explosion-proof components where necessary to prevent fire or explosion hazards.
Applications of Light Calcium Carbonate Powder Conveying Systems
Light calcium carbonate powder conveying systems are widely used in various industries that utilize light calcium carbonate as a raw material. Some common applications include:
- Paper and Pulp Industry: Light calcium carbonate is used as a filler in paper production, and conveying systems are used to transport it from storage to the papermaking process.
- Plastics and Rubber Industry: In the production of plastics and rubber products, light calcium carbonate is used as a filler to improve mechanical properties and reduce costs. Conveying systems ensure the consistent addition of the powder to the mixing process.
- Paint and Coatings Industry: Light calcium carbonate is used as a pigment and extender in paints and coatings. The conveying system ensures the accurate and uniform addition of the powder to the manufacturing process.
- Food and Pharmaceutical Industry: In some applications, light calcium carbonate is used as a food additive or in pharmaceutical formulations. Conveying systems are used to transport the powder safely and hygienically to the production lines.
Benefits of Using a Light Calcium Carbonate Powder Conveying System
Implementing a light calcium carbonate powder conveying system offers several benefits for industrial operations:
- Increased Efficiency: The system ensures consistent and continuous material flow, reducing downtime and increasing overall production efficiency.
- Improved Product Quality: By maintaining uniform flow rates and preventing material contamination, the system helps ensure consistent product quality.
- Enhanced Safety: The inclusion of dust collection systems and explosion-proof components reduces the risk of accidents and improves workplace safety.
- Reduced Maintenance Costs: Well-designed systems with proper maintenance protocols minimize the need for frequent repairs and replacements, leading to lower long-term maintenance costs.
- Environmental Compliance: The system helps meet environmental regulations by controlling dust emissions and reducing waste.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer and supplier of light calcium carbonate powder conveying system equipment. With years of experience in the industry, the company specializes in designing and manufacturing high-quality conveying systems tailored to the specific needs of various industries. HeadPowder's products are known for their reliability, efficiency, and durability, ensuring that customers receive the best possible solution for their material handling requirements. The company's headquarters is located in Shandong, China, where it continues to innovate and provide cutting-edge solutions for the powder handling industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China
