Understanding the material handling of potassium sulfate is crucial for industries that rely on this essential fertilizer. Potassium sulfate, a key component in modern agriculture, requires efficient and reliable systems to ensure safe and effective transportation from production sites to end-users. This article explores the fundamental aspects of potassium sulfate material handling and the core design principles that underpin such systems.
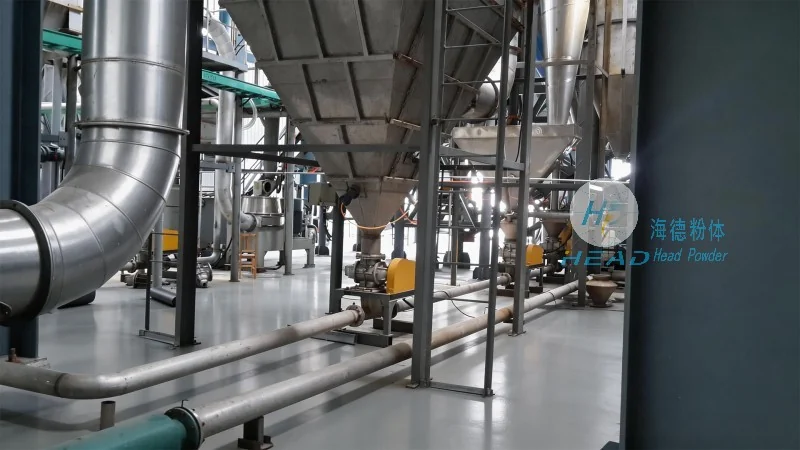
Potassium sulfate (K₂SO₄) is a widely used potassium fertilizer, prized for its high solubility and minimal environmental impact compared to other potassium sources. In industrial settings, handling this material involves moving it through various stages, from bulk storage to packaging or direct application. The efficiency of the material handling system directly impacts operational costs, safety, and overall productivity. For companies like Shandong HeadPowder Engineering Co., Ltd., based in China, developing robust material handling solutions is a critical focus to meet the growing demand for high-quality fertilizer products.
A typical potassium sulfate material handling system comprises several interconnected components designed to optimize flow and minimize risks. These components include bulk storage silos or hoppers, conveyor systems (such as belt conveyors or screw conveyors), feeding mechanisms, and transfer equipment. Each component must be carefully selected and integrated to ensure compatibility with the material's physical properties, such as its granular size and flow characteristics. For instance, the choice of conveyor type depends on the material's bulk density and abrasiveness, which can affect wear and tear on equipment. HeadPowder, as a specialized engineering firm, emphasizes the importance of material testing and analysis before designing a system to guarantee optimal performance.
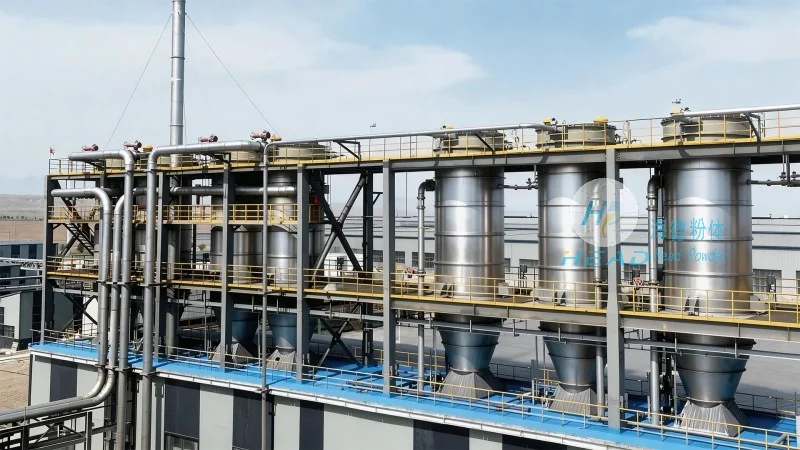
The design of a potassium sulfate material handling system follows several key principles aimed at maximizing efficiency, safety, and durability. First, the principle of gravity flow is often utilized to reduce energy consumption and mechanical stress on components. By arranging storage and processing equipment at appropriate elevations, materials can move through the system with minimal reliance on powered equipment. Second, the principle of continuous flow is critical to prevent material buildup and blockages, which can lead to safety hazards and production delays. This is achieved through proper sizing of conveyors, hoppers, and chutes, ensuring that the material's flow rate matches the system's capacity. Third, the principle of modular design allows for flexibility and scalability. HeadPowder's engineering approach often involves modular components that can be easily adjusted or expanded as production needs change, providing long-term value to clients.
When designing potassium sulfate material handling systems, safety and environmental protection are paramount. Potassium sulfate is generally considered non-toxic, but proper handling procedures are still essential to prevent dust generation and material spillage. Dust control measures, such as enclosed conveyor systems and dust collection equipment, are standard in modern designs to protect both personnel and the environment. Additionally, the system must be designed to prevent leaks or spills, which could lead to contamination of soil or water sources. HeadPowder adheres to strict safety and environmental standards, incorporating features like sealed hoppers, leak detection systems, and regular maintenance protocols to ensure compliance and operational safety.
Modern potassium sulfate material handling systems increasingly incorporate advanced technologies to enhance performance and reduce operational costs. Automation and control systems, such as programmable logic controllers (PLCs) and sensors, allow for real-time monitoring of flow rates, pressure, and temperature. This data-driven approach enables proactive maintenance and immediate response to system anomalies, minimizing downtime. Additionally, the use of variable frequency drives (VFDs) in conveyor systems optimizes energy consumption by adjusting motor speed based on the material load. HeadPowder leverages these technologies to provide clients with intelligent, efficient material handling solutions that adapt to changing operational conditions.
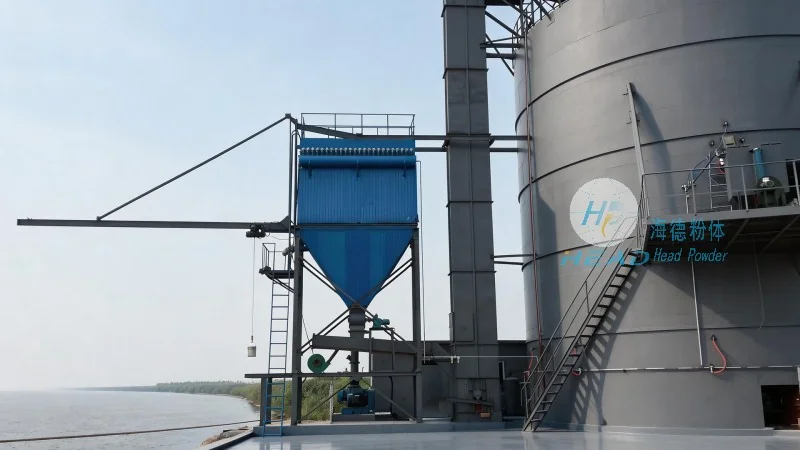
Consider a project undertaken by Shandong HeadPowder Engineering Co., Ltd. for a large fertilizer manufacturer. The client required a system to handle 10,000 tons of potassium sulfate per month, from bulk storage to packaging. HeadPowder's engineers conducted a thorough site assessment, analyzing the material's properties and the client's operational needs. The design included a 50-ton bulk storage silo, a belt conveyor system with VFD control, and a feeding mechanism integrated with a packaging line. The system was designed to operate continuously, with automated monitoring and alarm systems to detect any deviations from normal operation. The project was completed within the scheduled timeline and met all safety and environmental standards, resulting in a 15% reduction in operational costs and improved overall efficiency for the client.
Potassium sulfate material handling is a complex process that requires careful consideration of material properties, operational efficiency, and safety. The design principles outlined above, combined with advanced technologies and expert engineering, are essential for creating effective and reliable systems. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in developing these solutions, ensuring that industries can meet the growing demand for high-quality fertilizer products while maintaining operational excellence. By prioritizing modular design, safety, and technological integration, material handling systems can deliver long-term value and support sustainable agricultural practices.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top