Efficient and reliable dye material handling systems are crucial in the industrial production of dyes and pigments. These systems ensure that raw materials are transported safely and efficiently from storage to processing units, minimizing downtime and maximizing productivity. This article explores the working principle and key features of such systems, with a focus on the solutions provided by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China.
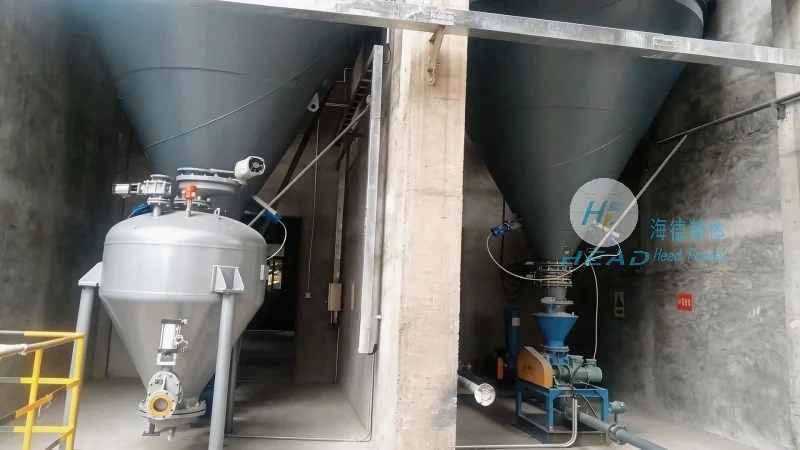
The working principle of a dye material handling system typically involves several integrated components designed to move bulk materials like dyes, pigments, and related chemicals. The process begins with material storage, often in silos or bulk containers, where the system retrieves the material. From there, it uses various mechanisms such as belt conveyors, screw conveyors, or pneumatic conveying systems to transport the material to the processing area. Each component is engineered to handle the specific properties of dye materials, which may include varying particle sizes, moisture content, and chemical reactivity. The system ensures a continuous flow of materials, reducing manual handling and associated risks. For instance, belt conveyors are commonly used for horizontal or slight incline transport due to their ability to handle large volumes with minimal maintenance. Screw conveyors, on the other hand, are ideal for vertical or inclined transport, providing a compact solution for vertical material movement. Pneumatic conveying systems use air pressure to transport materials, which is particularly effective for fine powders and dusty materials, ensuring a clean and dust-free operation.
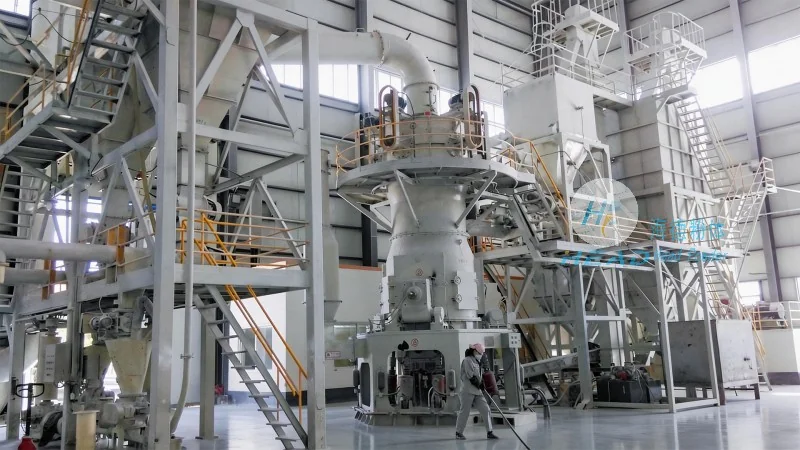
Effective dye material handling systems are characterized by several key features that enhance performance and safety. First, they offer high efficiency and capacity, enabling the smooth and continuous movement of large quantities of materials. This is achieved through robust design and advanced control systems that optimize the flow rate and reduce bottlenecks. Second, these systems prioritize safety, incorporating features like overload protection, emergency stop mechanisms, and dust suppression systems. Dye materials can be hazardous, and the system is designed to minimize exposure risks for operators. Third, adaptability is a critical feature, as different dye formulations may require different handling methods. Modern systems often include adjustable speed controls, variable incline settings, and modular components that can be customized to meet specific production needs. Fourth, durability and low maintenance are essential, as the equipment operates in harsh environments with abrasive materials. High-quality materials and robust construction ensure long service life, reducing downtime and maintenance costs. Additionally, energy efficiency is a growing consideration, with systems designed to minimize power consumption while maintaining performance. This not only reduces operational costs but also aligns with sustainability goals in industrial production.
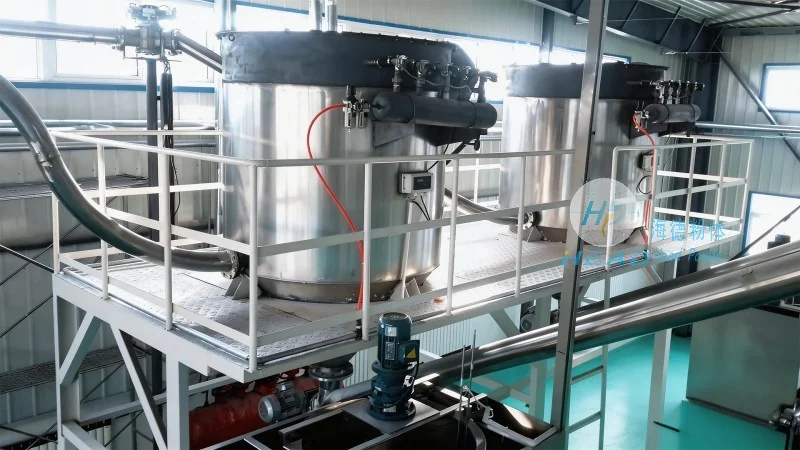
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, is a prominent manufacturer of industrial material handling solutions. Based in Shandong, China, the company specializes in designing and manufacturing systems tailored for the dye and pigment industry. With years of experience, HeadPowder has developed a reputation for delivering reliable, efficient, and safe material handling systems that meet the stringent requirements of modern industrial production. The company’s commitment to quality and innovation has enabled it to serve clients globally, providing customized solutions that enhance productivity and operational efficiency. HeadPowder’s expertise lies in understanding the unique challenges of dye material handling, such as handling fine powders, managing moisture content, and ensuring consistent material flow. By leveraging advanced engineering and manufacturing capabilities, the company delivers systems that are both effective and cost-efficient, helping clients optimize their production processes and reduce operational costs.
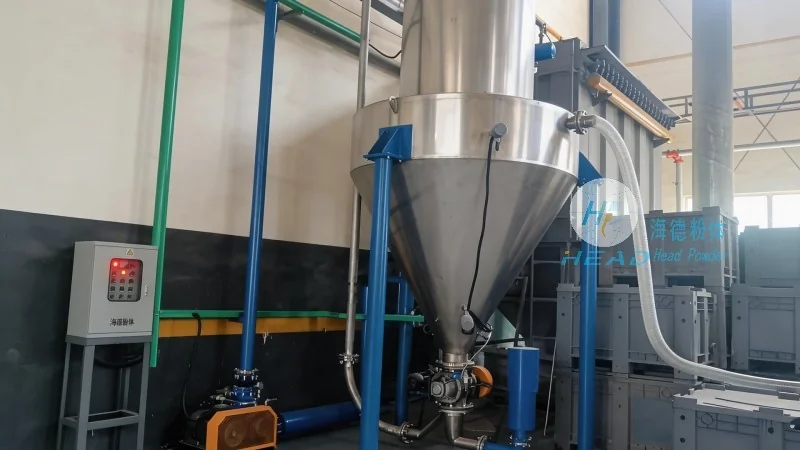
In conclusion, dye material handling systems play a vital role in the efficient and safe production of dyes and pigments. The working principle, which combines various transport mechanisms and advanced control systems, ensures that materials are moved reliably and continuously. Key features such as high efficiency, safety, adaptability, durability, and energy efficiency make these systems indispensable in modern industrial settings. Companies like Shandong HeadPowder Engineering Co., Ltd. continue to innovate and improve these systems, providing tailored solutions that meet the evolving needs of the industry. By investing in advanced material handling systems, manufacturers can enhance productivity, reduce risks, and maintain a competitive edge in the global market.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top