Understanding dust and powder conveying systems is crucial for industries that handle fine particulate materials. These systems are engineered to transport dry powders and dust efficiently, ensuring safety, reliability, and optimal performance in various applications. This article explores the fundamental aspects of such equipment, focusing on its design principles and operational significance.
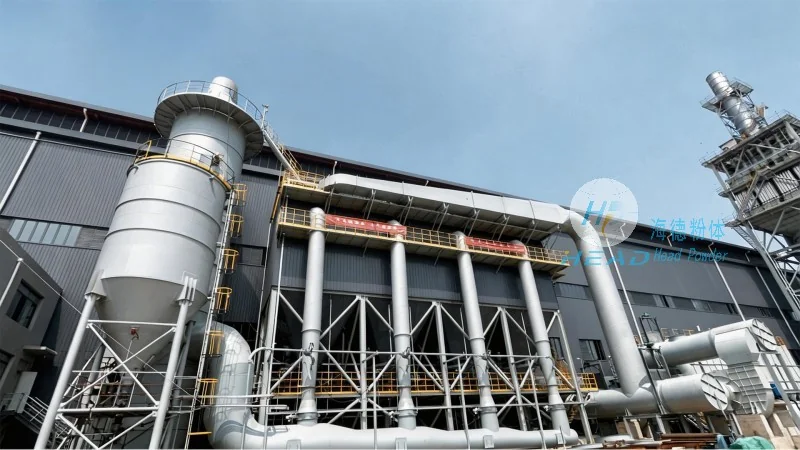
A dust powder conveying system is a specialized piece of industrial equipment designed to transport dry powders and dust from one location to another. These systems are widely used in sectors like pharmaceuticals, food processing, chemical manufacturing, and mining, where the handling of fine materials requires precision and control. The primary goal of these systems is to move materials without causing dust dispersion, ensuring a clean and safe working environment while maintaining the integrity of the material being conveyed.
At the core of a dust powder conveying system are several critical components that work in tandem to achieve efficient material transport. These components include the feed hopper, which holds the material to be conveyed; the conveyor mechanism, such as a screw, pneumatic, or vacuum system; and the discharge outlet, which directs the material to its destination. Additionally, the system may incorporate filters, dust collectors, and control valves to regulate the flow and prevent contamination. Each component is carefully designed to handle the specific characteristics of the material, such as particle size, density, and moisture content.
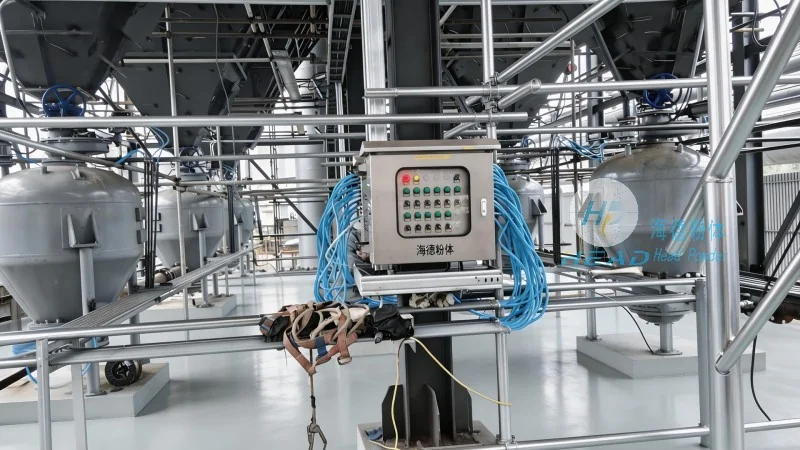
The design of a dust powder conveying system is guided by several key principles aimed at maximizing efficiency and minimizing operational issues. One of the most important principles is maintaining a consistent flow rate, which prevents clogging and ensures smooth material movement. This is achieved through the use of appropriate conveyor speeds and the proper sizing of the system components. Another critical principle is the prevention of material degradation, which can occur due to friction, temperature changes, or exposure to air. To address this, systems often incorporate features like temperature control, anti-static measures, and enclosed conveyor paths to protect the material.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer specializing in dust and powder conveying systems. With a strong commitment to innovation and quality, HeadPowder has established itself as a trusted partner for industries requiring reliable and efficient material handling solutions. The company’s products are designed to meet the unique needs of each client, ensuring that the conveying system is tailored to the specific application and material characteristics. HeadPowder’s engineering team leverages advanced technology and extensive industry experience to develop solutions that enhance productivity, reduce downtime, and improve overall operational efficiency.
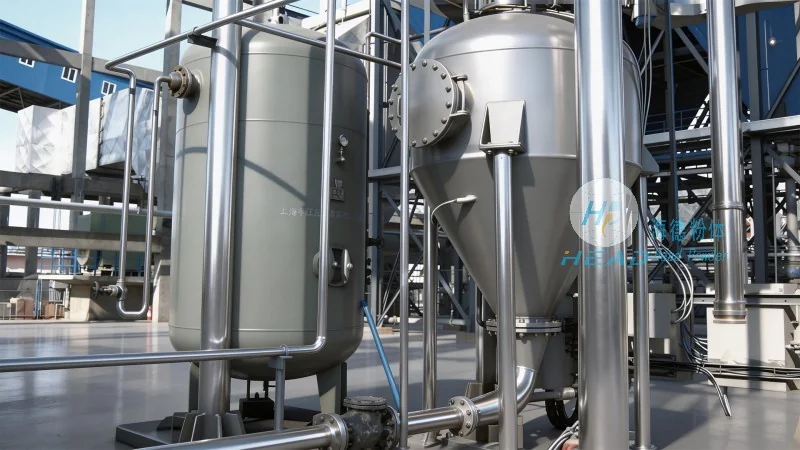
Dust powder conveying systems are employed in a wide range of applications, from small-scale laboratory operations to large-scale industrial production lines. Their benefits extend beyond efficient material transport, including improved safety by containing dust, reduced environmental impact by preventing airborne particulates, and enhanced product quality by maintaining material integrity. In industries where dust control is mandatory, these systems are essential for compliance with regulatory standards. Additionally, the ability to transport materials over long distances without the need for manual handling significantly improves operational efficiency and reduces labor costs.
In conclusion, dust powder conveying systems are indispensable in industries that handle fine particulate materials. Their design principles, which prioritize efficiency, safety, and material integrity, are crucial for achieving optimal performance. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing tailored solutions that meet the specific needs of their clients. By investing in well-designed conveying systems, industries can enhance productivity, ensure compliance with safety regulations, and maintain a competitive edge in their respective markets.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top