For those in the coffee processing and distribution industry, understanding the technology behind efficient coffee powder handling is crucial. A coffee powder pneumatic conveying system is a specialized piece of equipment designed to transport coffee powder from one location to another using air pressure or suction. This method offers a clean, efficient, and hygienic way to move the fine particles without direct contact with mechanical parts, which is essential for maintaining product quality and safety standards.
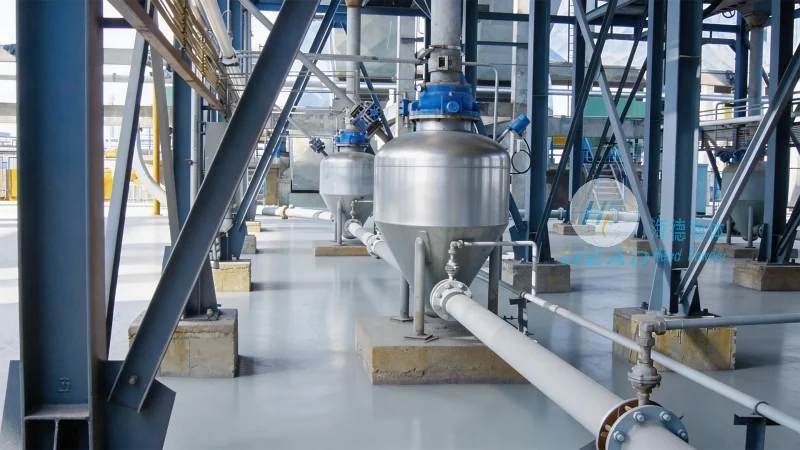
The primary function of a coffee powder pneumatic conveying system is to transport coffee powder in a sealed system, preventing contamination and dust dispersion. Unlike traditional belt or bucket conveyors, pneumatic systems use air to move the material, which is particularly advantageous for delicate products like coffee powder that can be easily damaged or contaminated by physical contact. The system typically operates by creating a pressure differential—either by blowing air (positive pressure) or sucking air (negative pressure)—to move the powder through a network of pipes.
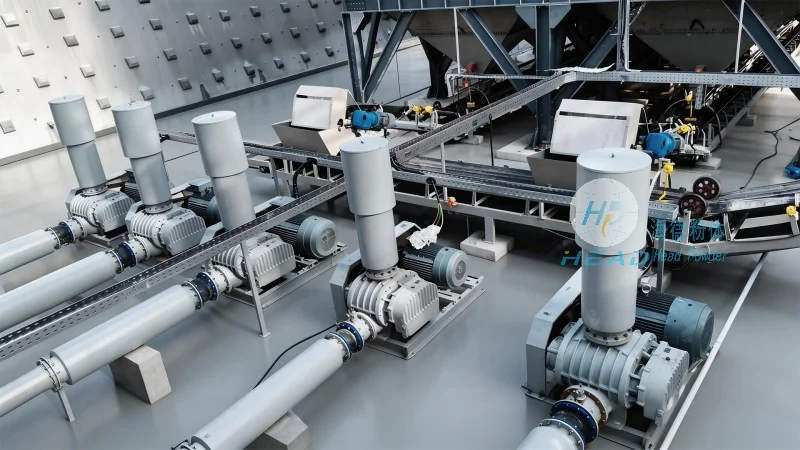
The design of a coffee powder pneumatic conveying system is governed by several critical principles to ensure optimal performance and reliability. First, the system must maintain a consistent air flow rate to prevent clogging or uneven material transport. This involves precise control of air pressure and flow velocity, which are tailored to the specific characteristics of coffee powder—such as particle size, density, and moisture content. Second, the system’s components, including the hopper, feeder, and pipeline, are constructed from materials that are resistant to corrosion and compatible with food-grade standards, ensuring long-term durability and compliance with industry regulations. Third, the design incorporates features like pulse jets or rotary valves to prevent material buildup and maintain smooth operation, which is vital for continuous production processes.
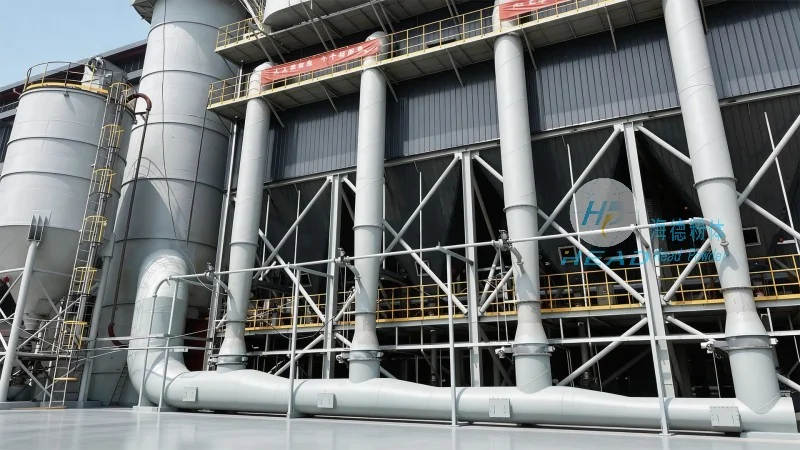
A typical coffee powder pneumatic conveying system consists of several key components that work in tandem to achieve efficient transport. The main components include a hopper for storing the coffee powder, a feeder (often a rotary valve or screw feeder) to control the flow rate, a blower or vacuum pump to generate the air pressure, and a network of stainless steel pipes to guide the powder. The working mechanism begins when the feeder releases a controlled amount of coffee powder into the pipe. Simultaneously, the blower introduces air into the pipe, creating a high-velocity air stream that carries the powder particles forward. The mixture of powder and air travels through the pipeline, reaching the destination point, such as a storage silo or processing unit. At the end of the pipeline, a separator (like a cyclone or filter) separates the coffee powder from the air, allowing the powder to be collected while the air is either vented or recirculated, depending on the system design.
Coffee powder pneumatic conveying systems are widely used in various stages of coffee processing and distribution. In coffee roasting facilities, these systems efficiently transport freshly roasted coffee beans to grinding units, ensuring a consistent supply of raw material. In coffee powder packaging plants, they move the ground coffee from storage to packaging machines, maintaining product integrity and preventing cross-contamination. The benefits of using pneumatic conveying for coffee powder are significant: it reduces labor costs by automating the material handling process, minimizes product damage due to gentle handling, and improves hygiene by keeping the powder enclosed in a sealed system. Additionally, the system’s flexibility allows for easy integration into existing production lines, adapting to changes in production volume or product types without major modifications.
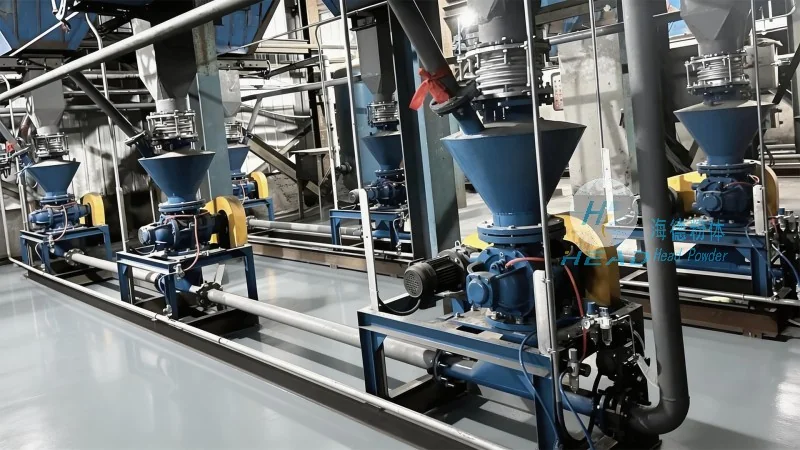
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer specializing in pneumatic conveying systems for the food and powder processing industries. With a focus on innovation and quality, HeadPowder designs and produces coffee powder pneumatic conveying systems that meet the highest standards of efficiency, reliability, and hygiene. The company’s headquarters is located in Shandong, China, where it leverages advanced engineering capabilities and extensive industry experience to develop tailored solutions for coffee processing facilities worldwide. HeadPowder’s commitment to customer satisfaction and product excellence has made it a trusted partner for businesses seeking to optimize their coffee powder handling processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top