An ABS granular pneumatic conveying system is a specialized industrial equipment designed to transport granular materials like plastic pellets, powders, or other fine particles through a pipeline using compressed air or other gas as the conveying medium. This technology offers a dust-free, efficient, and flexible method for material handling, making it ideal for various industries including plastics manufacturing, chemical processing, and food processing. The system's design integrates several key components that work in tandem to ensure reliable and consistent material transport.
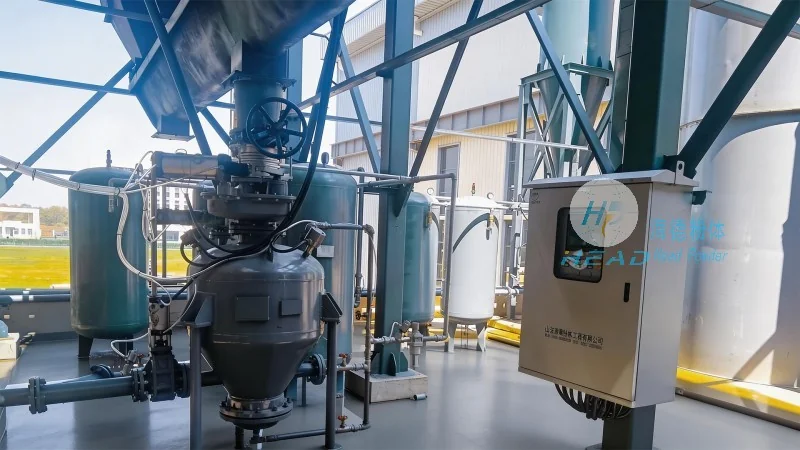
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems. With years of experience in the industry, HeadPowder has established itself as a trusted partner for businesses seeking efficient material handling solutions. The company's commitment to quality and innovation has enabled it to deliver systems that meet the diverse needs of clients across different sectors. HeadPowder's team of experts leverages cutting-edge technology and engineering expertise to develop customized solutions that optimize material transport processes, reduce operational costs, and enhance overall productivity.
The design of an ABS granular pneumatic conveying system is based on several fundamental principles that ensure effective material transport. The primary design principle is the use of differential pressure to move the material through the pipeline. Compressed air is introduced into the system, creating a pressure differential that propels the granular material forward. The system typically consists of a hopper for material storage, a feeder to control the flow rate, a pipeline network, and a receiver for the discharged material. The design must consider factors such as material properties (e.g., particle size, density, moisture content), conveying distance, and required flow rate to ensure optimal performance.
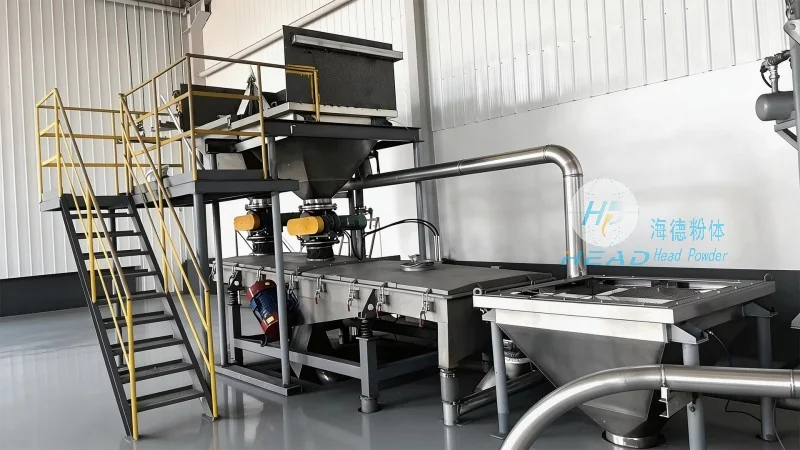
Several critical components are integral to the operation of an ABS granular pneumatic conveying system. The hopper serves as the storage vessel, holding the granular material before it is fed into the system. The feeder, often a rotary valve or a screw feeder, regulates the material flow rate to maintain a consistent pressure and prevent blockages. The pipeline network, made of materials resistant to the conveyed material and pressure, transports the material from the feeder to the receiver. The receiver collects the material after it has been conveyed and may include features like a dust collection system to ensure environmental compliance. Additionally, the system may include control valves and sensors to monitor and adjust the conveying process in real-time, ensuring efficient operation and preventing system failures.
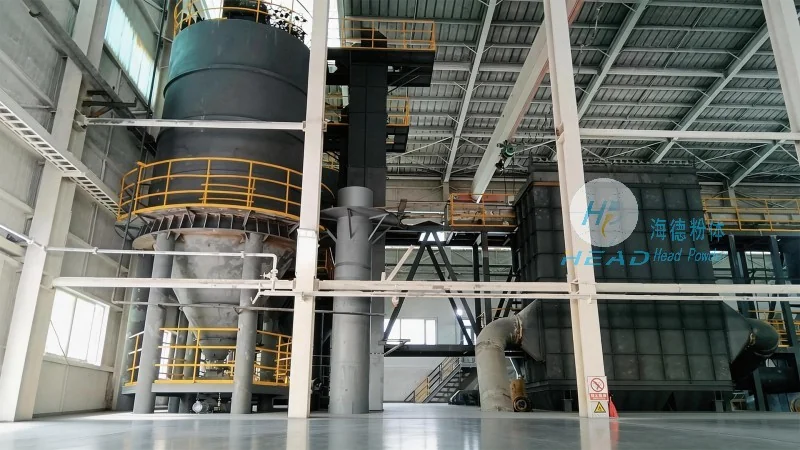
ABS granular pneumatic conveying systems offer numerous advantages over traditional material handling methods. One of the key benefits is the ability to transport materials in a dust-free environment, which enhances workplace safety and reduces the risk of contamination. The system is also highly flexible, allowing for changes in material flow rates and conveying distances without significant modifications. Additionally, the enclosed pipeline design minimizes material loss and improves overall material recovery rates. The system's compact design and low maintenance requirements make it an economical choice for businesses looking to optimize their material handling processes. Furthermore, the use of compressed air as the conveying medium allows for easy integration with existing production lines and reduces the need for additional equipment.
ABS granular pneumatic conveying systems are widely used in various industries due to their versatility and efficiency. In the plastics industry, these systems are commonly used to transport ABS pellets from storage to processing equipment, ensuring a continuous and clean supply of material. In chemical processing, they are used to handle powders and granules, preventing dust exposure and maintaining product purity. The food processing industry also benefits from these systems, as they can handle food-grade materials while maintaining hygiene standards. Other applications include pharmaceuticals, where the enclosed design prevents contamination, and mining, where they are used to transport bulk materials over long distances.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top