Denitrifier pneumatic conveying systems are critical components in modern industrial processes, particularly in facilities that handle nitrogen oxide reduction agents. These systems are engineered to transport denitrification agents efficiently and safely, ensuring optimal performance in environmental control applications. Understanding the functionality and design principles of such systems is essential for industries aiming to maintain compliance with environmental regulations while enhancing operational efficiency.
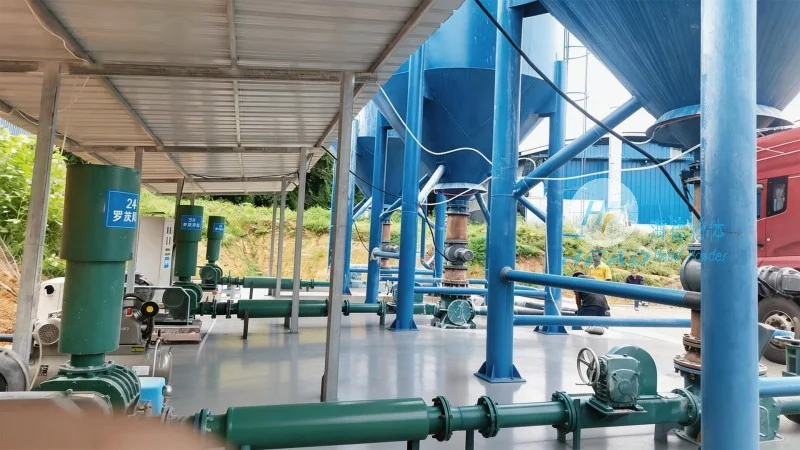
A denitrifier pneumatic conveying system is a specialized equipment setup designed to transport denitrification agents, typically in powder or granular form, from storage silos or hoppers to the point of use, such as in a selective catalytic reduction (SCR) system. The primary goal of these systems is to deliver the denitrifier material with precision, minimizing material loss and ensuring consistent flow rates. This is crucial for maintaining the efficiency of the denitrification process, which is vital for reducing nitrogen oxide emissions from industrial sources.
The design of a denitrifier pneumatic conveying system is based on several key principles that ensure reliable operation and material integrity. These principles include the selection of appropriate conveying air pressure, the choice of suitable pipeline materials, and the optimization of system layout to minimize pressure drops and material degradation. The system typically consists of a blower or compressor to generate the conveying air, a hopper or silo for material storage, a conveying line with appropriate fittings and valves, and a discharge point where the material is released into the downstream process.
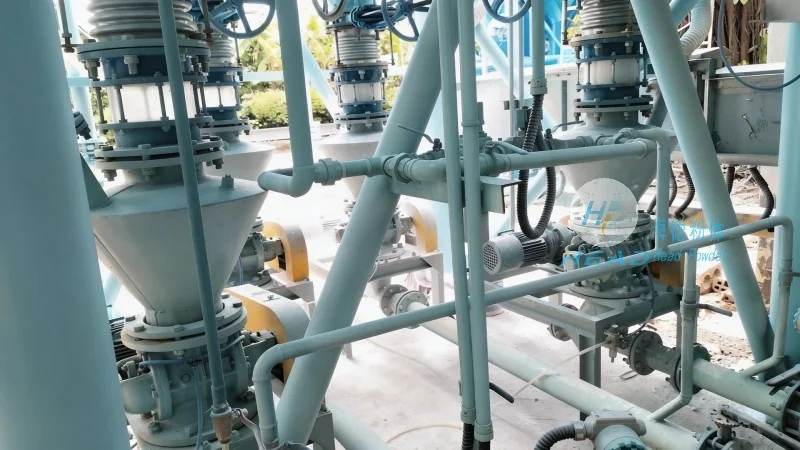
Several critical components make up a denitrifier pneumatic conveying system. The blower or compressor is responsible for generating the necessary air pressure to move the material through the pipeline. The hopper or silo stores the denitrification agent, providing a controlled feed to the system. The conveying line, often made of stainless steel or other corrosion-resistant materials, ensures the material is transported without degradation. Valves and control mechanisms regulate the flow rate and direction of the material, while filters and cyclones separate the material from the air at the discharge point, preventing dust contamination and ensuring clean operation.
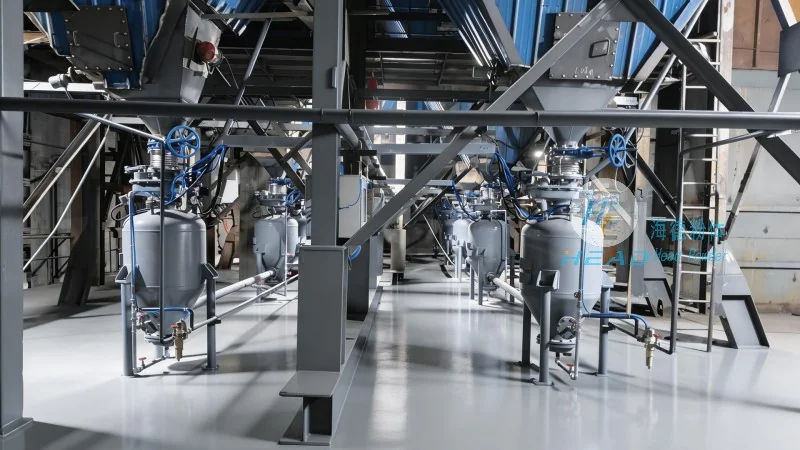
Implementing a denitrifier pneumatic conveying system offers numerous benefits for industrial operations. These include improved material handling efficiency, reduced labor costs associated with manual handling, and enhanced safety by minimizing exposure to powders. The system also contributes to better environmental performance by ensuring consistent delivery of denitrification agents, which helps maintain the effectiveness of the nitrogen oxide reduction process. Additionally, the automated nature of these systems reduces the risk of human error and improves overall process reliability.
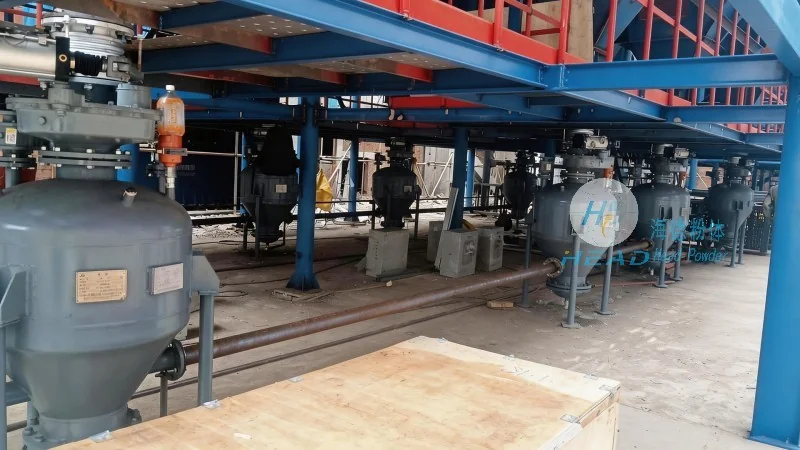
Denitrifier pneumatic conveying systems are widely used in power plants, refineries, and other industrial facilities where nitrogen oxide emissions need to be controlled. In power plants, for example, these systems are integrated with selective catalytic reduction (SCR) systems to deliver the necessary denitrification agent to the catalyst bed. The consistent and reliable delivery of the agent is crucial for maintaining the SCR system's performance, which directly impacts the plant's compliance with environmental regulations. Similarly, in refineries, these systems help manage the flow of denitrification agents to the combustion control systems, ensuring optimal emissions reduction.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading provider of specialized engineering solutions for industrial material handling. With a focus on innovation and quality, the company has developed advanced denitrifier pneumatic conveying systems tailored to meet the specific needs of various industrial applications. Headpowder's expertise lies in designing and manufacturing systems that ensure efficient, safe, and reliable transport of denitrification agents, contributing to the environmental sustainability and operational efficiency of its clients. The company's facilities are located in Shandong, China, where it leverages local resources and expertise to deliver high-quality products and services to the global market.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top