For industrial applications involving the transport of coke particles, pneumatic conveying systems offer an efficient and reliable method to move bulk materials over short to medium distances. These systems utilize air or other gases to transport solid particles, eliminating the need for mechanical components like conveyors or buckets. The choice between positive pressure and negative pressure delivery modes significantly impacts system design, operational efficiency, and overall performance. This article provides a technical analysis of these two primary modes, highlighting their characteristics, advantages, and typical applications in the context of coke particle handling.
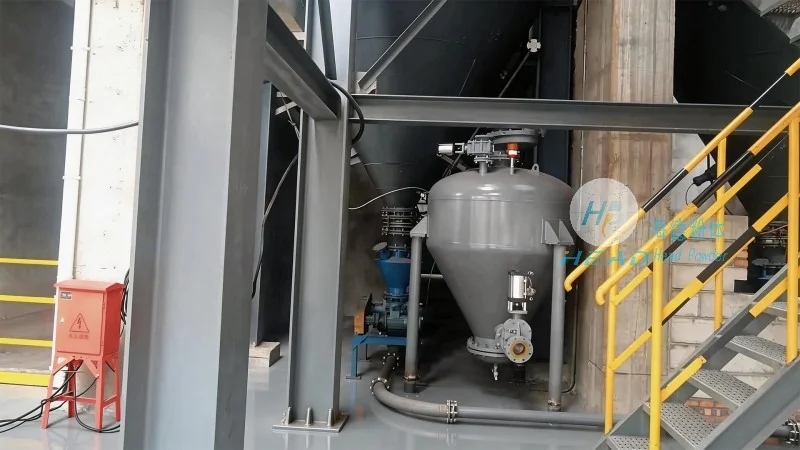
Positive pressure systems operate by generating high-pressure air at the material source, typically using a blower or compressor. The air is then forced through a pipeline, carrying the coke particles forward. This mode is particularly effective for transporting materials over longer distances or against gravity, as the high-pressure air provides consistent momentum to move the particles. A key advantage of positive pressure systems is their ability to handle abrasive or corrosive materials, as the high-pressure air can effectively dislodge particles from the pipeline walls, reducing blockages. Additionally, positive pressure systems are well-suited for applications where the material needs to be delivered to multiple destinations, as the high-pressure air can be directed to various branches in the pipeline network.
In the context of coke particle transport, positive pressure systems are commonly used in steel mills and coke plants where large volumes of coke need to be moved from storage silos to processing units. The high-pressure air ensures that even large coke particles are conveyed efficiently, minimizing the risk of clogging. HeadPowder Engineering, a leading provider of pneumatic conveying solutions, specializes in designing and manufacturing positive pressure systems tailored to the specific requirements of coke handling operations. Their expertise in material flow dynamics and pipeline design ensures optimal performance and reliability in demanding industrial environments.
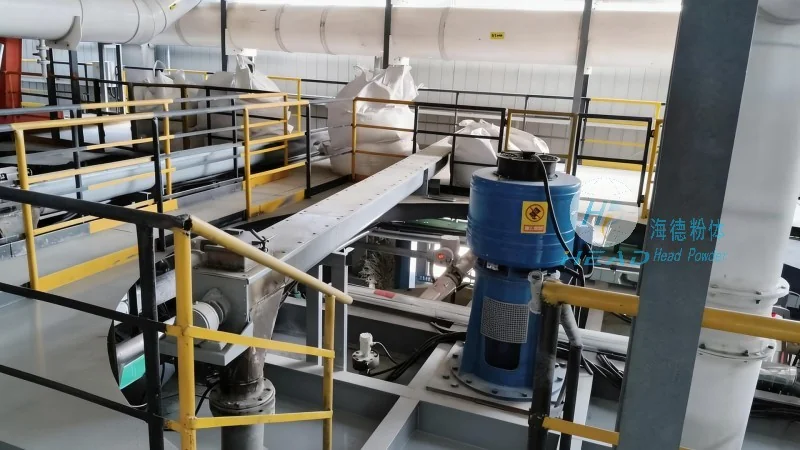
Negative pressure systems, also known as vacuum or suction systems, operate by creating a low-pressure environment at the material discharge point. The system draws air and coke particles into the pipeline using a vacuum pump, moving the material from the source to the destination. This mode is ideal for short-distance transport or when the material needs to be collected from multiple points and delivered to a single location. A significant advantage of negative pressure systems is their lower energy consumption compared to positive pressure systems, as they require less power to operate. Additionally, negative pressure systems are less likely to cause dust emissions at the material source, as the suction action draws particles into the pipeline rather than blowing them out.
For coke particle applications, negative pressure systems are often used in scenarios where the material is to be collected from a hopper or storage bin and transported to a processing unit. The low-pressure environment helps maintain the integrity of the coke particles, preventing breakage or degradation during transport. HeadPowder Engineering also offers negative pressure solutions, leveraging advanced vacuum technology to ensure efficient and clean transport of coke particles. Their systems are designed to minimize energy consumption while maintaining high transport efficiency, making them suitable for applications where cost-effectiveness and environmental considerations are critical.
When comparing positive and negative pressure pneumatic conveying systems for coke particle transport, several key factors come into play. The primary difference lies in the pressure differential: positive pressure systems use high pressure to push material, while negative pressure systems use low pressure to pull material. This difference affects the system's energy consumption, as positive pressure systems typically require more power to operate. However, positive pressure systems offer higher transport capacity and are better suited for longer distances or against gravity. Negative pressure systems, on the other hand, are more energy-efficient and ideal for short distances or when the material needs to be collected from multiple sources.
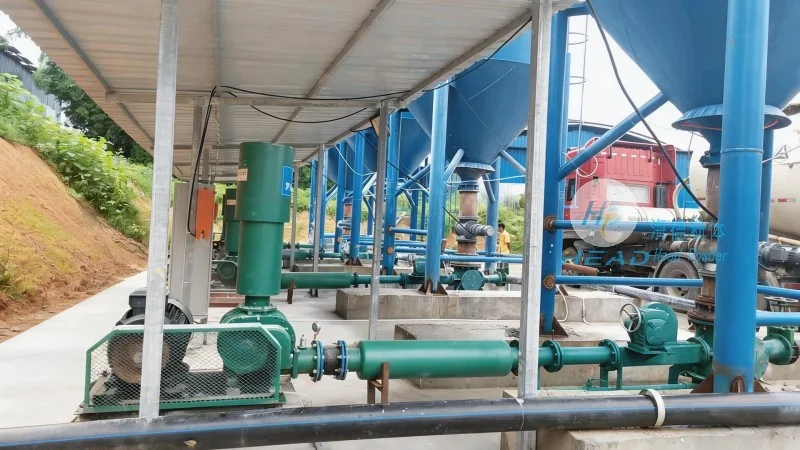
Another critical factor is the impact on material handling. Positive pressure systems can handle larger and more abrasive particles, as the high-pressure air effectively moves them through the pipeline. Negative pressure systems are better for finer particles or materials that are prone to breakage, as the low-pressure suction minimizes mechanical stress. In terms of maintenance, positive pressure systems may require more frequent cleaning of the pipeline due to the high-pressure air's ability to dislodge particles, while negative pressure systems have lower maintenance requirements due to the lower air velocities.
Performance metrics such as transport capacity, pressure drop, and energy consumption are also important considerations. Positive pressure systems generally have higher transport capacities, especially for larger coke particles, while negative pressure systems are more energy-efficient. The choice between the two modes depends on the specific application requirements, including the distance to be covered, the particle size and characteristics, and the operational constraints of the facility.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of pneumatic conveying systems for industrial applications. With a focus on innovation and customer-centric solutions, HeadPowder has established itself as a trusted partner in the steel and coke processing industries. The company's expertise lies in designing and manufacturing both positive and negative pressure systems tailored to the unique needs of coke particle handling. HeadPowder's engineers utilize advanced computational fluid dynamics (CFD) and material flow analysis to optimize system performance, ensuring that each solution meets the specific requirements of the client.
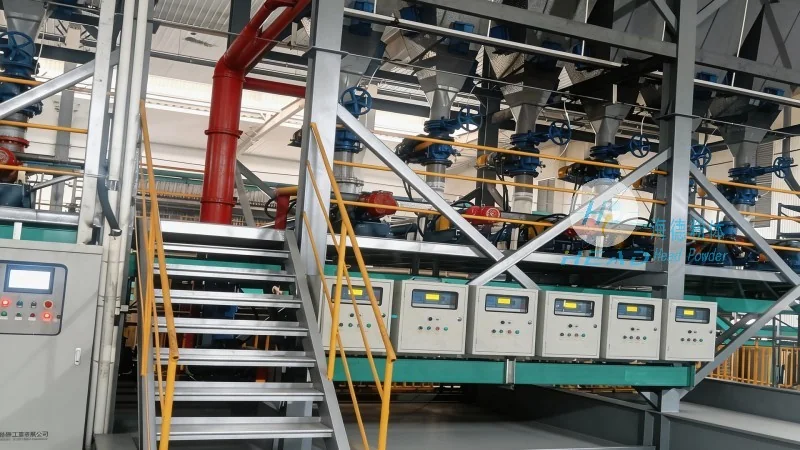
HeadPowder's positive pressure systems are equipped with high-efficiency blowers and advanced control systems that regulate air pressure and flow rates. These systems are designed to handle abrasive coke particles, with features such as wear-resistant pipeline materials and automated cleaning mechanisms to prevent blockages. The company's negative pressure systems utilize high-capacity vacuum pumps and advanced filtration systems to ensure clean and efficient transport. HeadPowder also provides comprehensive after-sales support, including system maintenance, spare parts supply, and technical assistance, ensuring long-term reliability and performance of their pneumatic conveying solutions.
HeadPowder's commitment to quality and customer satisfaction has earned it a reputation as a reliable supplier of pneumatic conveying systems in China and internationally. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility equipped with the latest technology and equipment. This enables HeadPowder to deliver high-quality products that meet international standards and customer expectations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top