High-Calcium powder pneumatic conveying equipment is a specialized system designed to transport high-calcium powder materials efficiently and reliably. This equipment is widely used in industrial applications where the safe and effective movement of bulk powders is critical. The core principle of this system involves using compressed air or other gases to create a flow that propels the powder through a pipeline network.
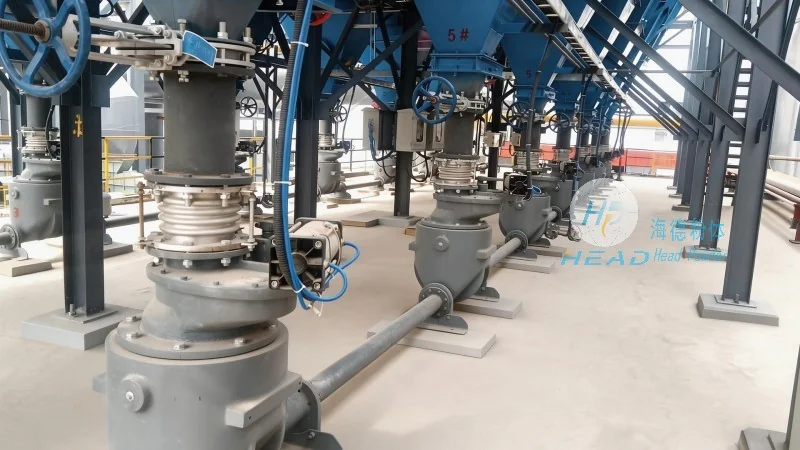
The operation of high-calcium powder pneumatic conveying equipment is based on the fundamental principle of fluidization and pneumatic transport. The system typically consists of a powder feeder, a conveying line, a control system, and a dust collection unit. The process begins when the high-calcium powder is fed into the system. Compressed air is then introduced into the conveying line, creating a low-pressure zone that draws the powder particles into the air stream. As the air flows through the pipeline, it carries the powder particles along, ensuring a continuous and controlled transport. The control system manages the air pressure and flow rate to maintain optimal conveying conditions, preventing issues such as clogging or uneven flow. The dust collection unit at the end of the line captures any fine particles that may escape, ensuring environmental compliance and product purity.
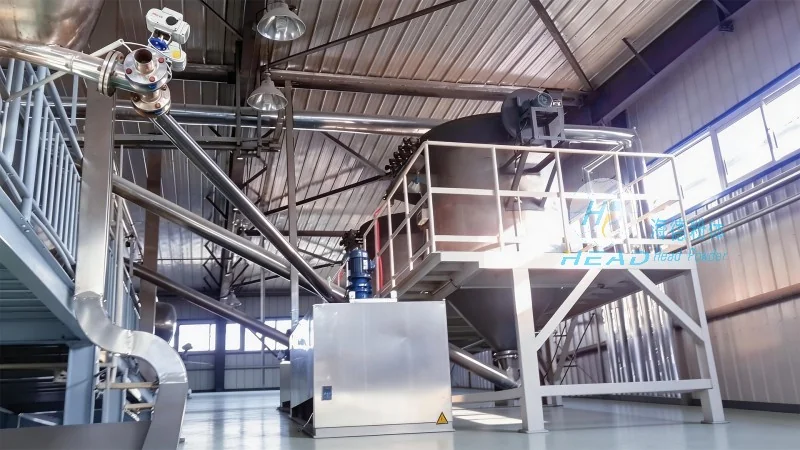
Several key components work together to ensure the smooth operation of high-calcium powder pneumatic conveying equipment. The powder feeder is responsible for accurately measuring and feeding the powder into the system, maintaining a consistent flow rate. The conveying line, often made of stainless steel or other corrosion-resistant materials, is designed to withstand the abrasive nature of high-calcium powder. The control system, equipped with sensors and valves, monitors and adjusts the air pressure and flow to adapt to varying powder characteristics and system demands. The dust collection unit, typically a bag filter or cyclone separator, captures residual powder particles, preventing air pollution and maintaining a clean working environment. Each component plays a crucial role in the overall efficiency and reliability of the conveying process.
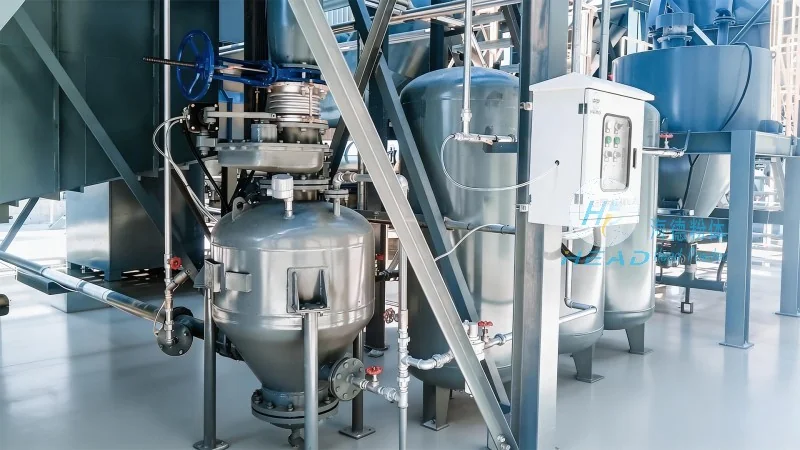
Implementing high-calcium powder pneumatic conveying equipment offers several significant advantages for industrial operations. First, it provides a dust-free and hygienic conveying method, which is essential for maintaining product quality and compliance with environmental regulations. Unlike traditional mechanical conveying systems, pneumatic conveying eliminates the need for moving parts in contact with the powder, reducing wear and tear and minimizing the risk of contamination. Second, the system offers high flexibility in terms of layout and installation, as the conveying lines can be easily routed around obstacles and adapted to different production layouts. This flexibility allows for efficient integration into existing facilities or new plant designs. Third, the equipment enables precise control over the powder flow rate and pressure, ensuring consistent product delivery and preventing overloading or underloading of downstream processes. Additionally, the system can handle a wide range of powder characteristics, including varying particle sizes, moisture content, and bulk density, making it suitable for diverse industrial applications.
High-calcium powder pneumatic conveying equipment is widely utilized in various industrial sectors that require the handling of bulk powders. In the cement industry, it is used to transport raw materials such as limestone and gypsum to production lines. In the food and beverage industry, it facilitates the transport of calcium-rich ingredients like calcium carbonate or calcium phosphate in food processing facilities. The pharmaceutical industry also benefits from this equipment for conveying active pharmaceutical ingredients (APIs) and excipients, ensuring a sterile and controlled environment. Additionally, in the chemical and mineral processing industries, it is employed to move high-calcium powders used in the production of fertilizers, coatings, and other chemical products. The versatility of the system makes it suitable for a broad spectrum of applications, where efficient and reliable powder transport is essential for operational success.
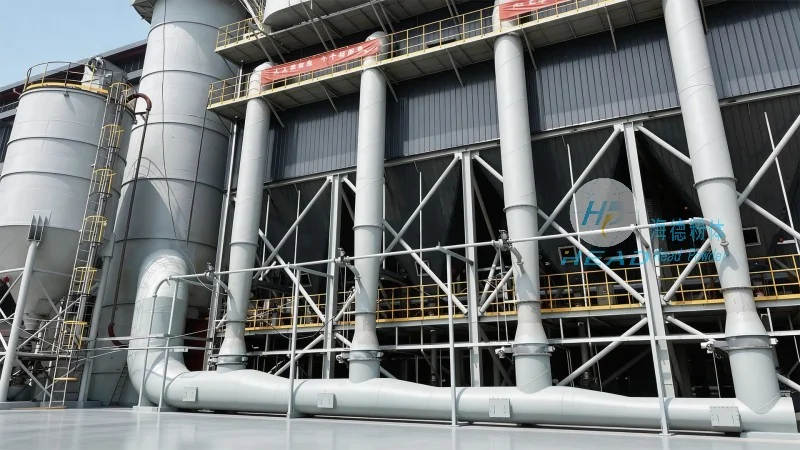
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer and supplier of high-quality pneumatic conveying equipment. With a strong commitment to innovation and customer satisfaction, the company specializes in designing and manufacturing customized solutions tailored to the specific needs of industrial clients. Headpowder's team of experienced engineers and technicians leverages advanced technology and rigorous quality control processes to ensure that each piece of equipment meets the highest standards of performance and reliability. The company's products are widely recognized for their durability, efficiency, and adaptability, making them a trusted choice for businesses in various industries. Headpowder's headquarters is located in Shandong, China, where the company maintains state-of-the-art manufacturing facilities and a dedicated customer support team. By focusing on continuous improvement and customer-centric approaches, headpowder aims to provide sustainable and effective solutions for the efficient handling of bulk powders, supporting the growth and success of its clients in the global market.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top