When it comes to handling and transporting sulfur tablets, the use of pneumatic conveying systems has become increasingly common in industrial applications. These systems offer an efficient and reliable method for moving bulk materials like sulfur tablets from one location to another, ensuring smooth operations in various production processes. In this article, we will explore the components, working principles, and key features of a sulfur tablet pneumatic conveying equipment, along with an overview of the general structure and principles of powder conveying systems.
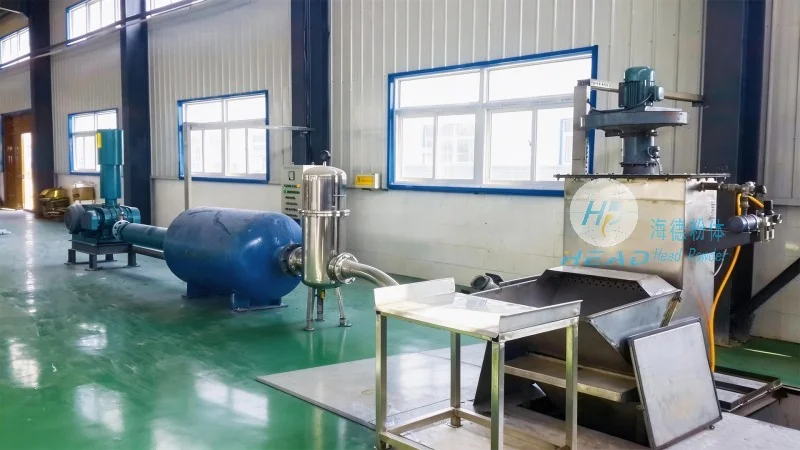
Pneumatic conveying systems are designed to transport solid materials, such as powders and granules, using a stream of air or gas. These systems are widely used in industries like chemical processing, pharmaceuticals, and food processing due to their ability to handle a wide range of materials with minimal product degradation. The core of a pneumatic conveying system is the ability to create a pressure or vacuum environment that moves the material through a pipeline.
The sulfur tablet pneumatic conveying equipment typically consists of several key components that work together to ensure efficient material transport. These components include the material hopper, the feeder, the conveying pipeline, the air compressor or vacuum pump, and the control system. Each component plays a crucial role in the overall operation of the system.
The material hopper is the storage container where sulfur tablets are loaded before being conveyed. It is designed to hold a sufficient quantity of material to maintain a consistent flow to the feeder. The feeder, often a rotary valve or a screw feeder, regulates the flow of sulfur tablets from the hopper into the conveying pipeline. This component ensures that the material is fed at a controlled rate, preventing blockages and maintaining a steady flow.
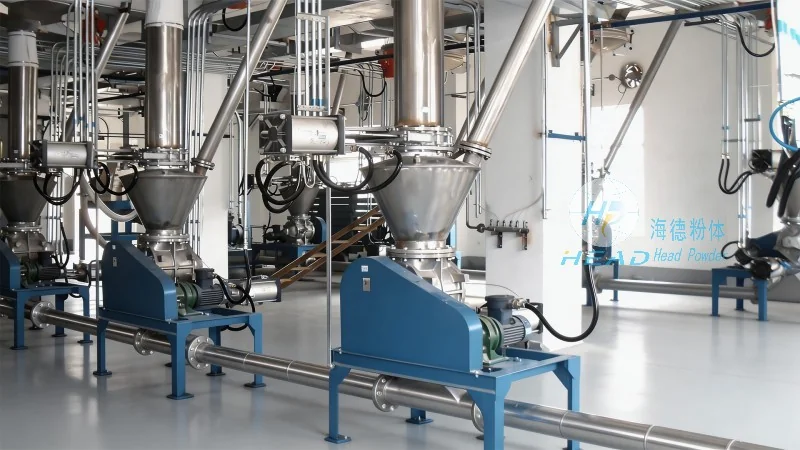
The conveying pipeline is the main channel through which sulfur tablets are transported. It is typically made of stainless steel or other corrosion-resistant materials to handle the chemical properties of sulfur. The air flow, generated by an air compressor or a vacuum pump, creates the necessary pressure or vacuum to move the material through the pipeline. The design of the pipeline, including the use of bends, elbows, and expansion joints, is critical to minimize pressure losses and ensure smooth material transport.
The control system of the pneumatic conveying equipment monitors and regulates the operation of the system. It includes sensors to detect material levels in the hopper, pressure in the pipeline, and air flow rates. The system can be programmed to adjust the feeding rate or air pressure as needed to maintain optimal performance. Additionally, safety features such as pressure relief valves and emergency shut-off switches are integrated to prevent accidents and ensure safe operation.
The working principle of a sulfur tablet pneumatic conveying system involves the creation of a flow of air that entrains the sulfur tablets and moves them through the pipeline. In a pressure system, the air compressor increases the air pressure, which forces the material through the pipeline. In a vacuum system, the vacuum pump creates a low-pressure environment that draws the material into the pipeline. The material is carried by the air stream and deposited at the destination point, where it is collected in a receiving hopper.
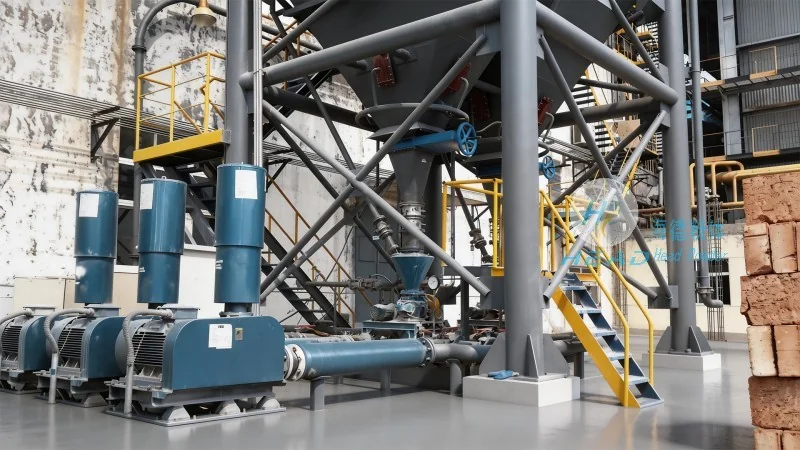
Sulfur tablet pneumatic conveying equipment is widely used in various industrial applications, including chemical manufacturing, pharmaceutical production, and food processing. The benefits of using such systems include improved safety by eliminating manual handling of bulk materials, reduced product contamination due to enclosed systems, and increased efficiency through automated operation. Additionally, these systems can handle a wide range of material sizes and shapes, making them versatile for different production needs.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of powder handling equipment, specializes in designing and manufacturing high-quality pneumatic conveying systems for various industrial applications. With years of experience in the industry, the company has developed advanced solutions tailored to meet the specific needs of its clients. HeadPowder's products are known for their durability, efficiency, and reliability, ensuring long-term performance and minimal maintenance costs.
In conclusion, a sulfur tablet pneumatic conveying equipment is a sophisticated system designed to efficiently transport bulk materials like sulfur tablets. By understanding the structure and working principles of such systems, industries can optimize their material handling processes, improve productivity, and enhance safety. With the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., businesses can access reliable and efficient solutions to meet their material transport needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top