Phenolic powder, also known as phenolic resin powder, is a widely used material in various industrial applications due to its excellent mechanical properties, electrical insulation, and chemical resistance. The efficient handling and transportation of phenolic powder are crucial for maintaining production efficiency and product quality. Pneumatic conveying systems have emerged as a reliable solution for transporting such powders, offering advantages like dust-free operation, low maintenance, and the ability to handle a wide range of materials.
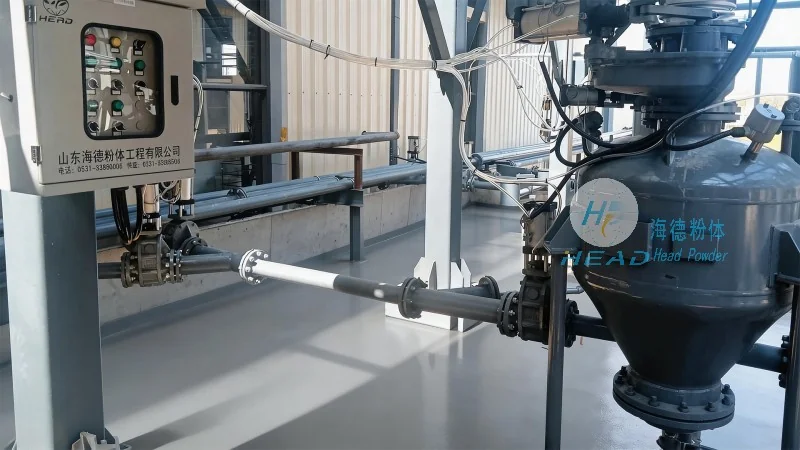
Pneumatic conveying systems are designed to transport bulk materials, including powders and granules, using a gas stream, typically air or other gases. These systems are categorized into two main types: dilute-phase and dense-phase conveying. Dilute-phase systems use high-velocity air to suspend the material particles, while dense-phase systems use lower velocities and higher pressure to push the material through the pipeline.
The working principle of a pneumatic conveying system for phenolic powder involves several key components and processes. The system typically includes a hopper, a feeder, a conveying line, and a receiver. The process begins with the phenolic powder being fed from the hopper into the conveying line via a feeder. The feeder controls the flow rate of the powder to ensure consistent and controlled transportation. As the powder enters the conveying line, a high-velocity air stream is introduced, which suspends the powder particles and propels them through the pipeline to the receiver. The receiver then collects the powder, and the air is filtered and returned to the system or released to the atmosphere.
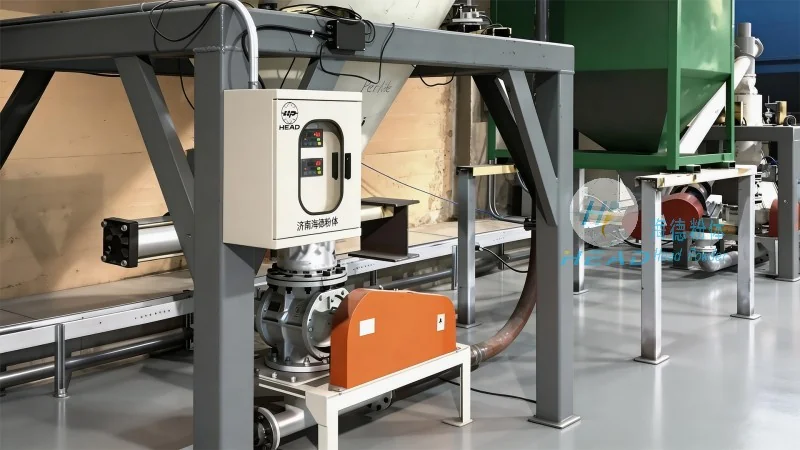
Implementing a pneumatic conveying system for phenolic powder offers numerous benefits. Firstly, it provides a dust-free environment, which is essential for maintaining product purity and ensuring workplace safety. Unlike mechanical conveying methods, which can generate dust and cause contamination, pneumatic systems keep the material enclosed, reducing the risk of exposure to airborne particles. Secondly, these systems are highly efficient in terms of energy consumption and operational costs. The use of air as the conveying medium is cost-effective and reduces the need for additional equipment like conveyor belts or buckets. Additionally, pneumatic conveying systems are versatile and can handle various particle sizes and shapes, making them suitable for different production requirements.
In the production of phenolic powder, pneumatic conveying systems are widely used in various stages, such as raw material handling, mixing, and packaging. For instance, during the raw material preparation stage, phenolic resin powders are often stored in bulk and need to be transported to the mixing equipment. Pneumatic conveying allows for seamless and continuous transfer of the powder, ensuring that the mixing process is not interrupted. Similarly, in the packaging stage, the powder is conveyed from the production line to the packaging machines, maintaining a clean and efficient workflow. The ability to handle large volumes of phenolic powder quickly and reliably makes pneumatic conveying an indispensable part of modern phenolic powder production facilities.
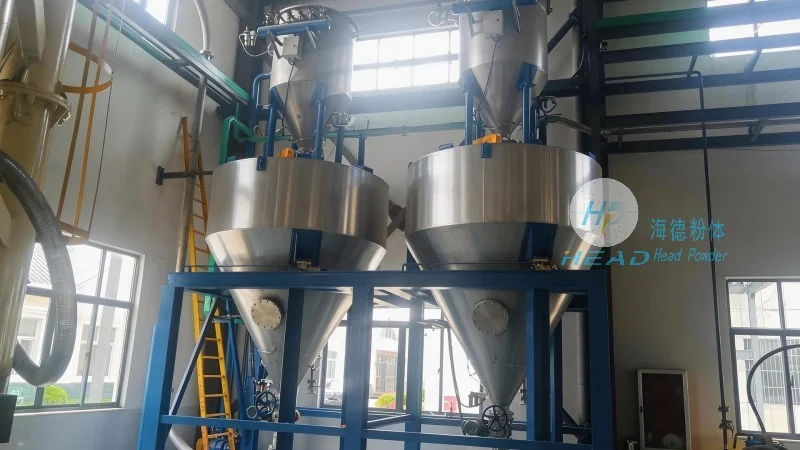
Shandong HeadPowder Engineering Co., Ltd., a leading provider of pneumatic conveying solutions, specializes in designing and manufacturing customized systems tailored to the specific needs of phenolic powder handling. With years of experience in the industry, the company understands the unique challenges associated with transporting phenolic powder, such as its tendency to agglomerate or stick to surfaces. To address these issues, HeadPowder engineers develop innovative solutions, including specialized feeders, airlocks, and pipeline designs that ensure smooth and efficient conveying. The company's team of experts works closely with clients to assess their production requirements, material characteristics, and operational constraints to deliver optimal pneumatic conveying systems. By leveraging advanced technology and a deep understanding of material handling, HeadPowder ensures that its systems are not only efficient but also durable and low-maintenance.
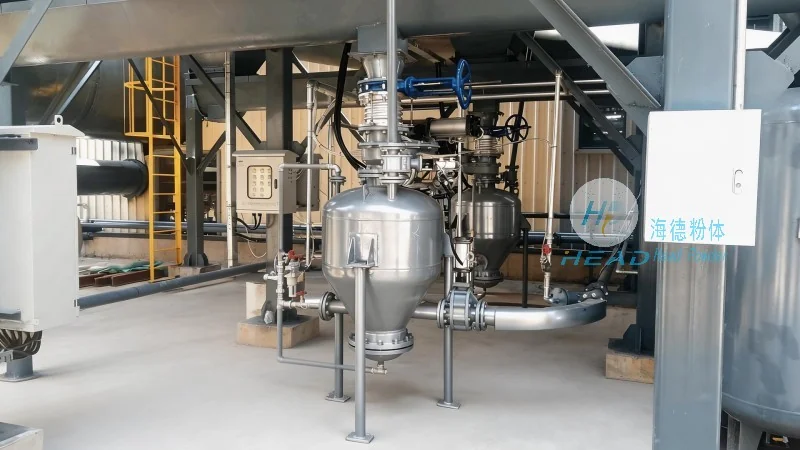
At Shandong HeadPowder Engineering Co., Ltd., quality is a top priority. The company adheres to strict quality control measures throughout the design, manufacturing, and installation of its pneumatic conveying systems. Each component is carefully selected and tested to ensure it meets the highest standards of performance and reliability. Additionally, HeadPowder provides comprehensive technical support to its clients, including installation guidance, maintenance training, and ongoing system optimization. The company's commitment to customer satisfaction is reflected in its responsive service and dedication to resolving any issues that may arise during the operation of the conveying system. By partnering with HeadPowder, clients can be confident that their phenolic powder handling needs are in capable hands, ensuring smooth and efficient production processes.
In conclusion, pneumatic conveying systems play a vital role in the efficient and safe handling of phenolic powder. The working principle of these systems, combined with their advantages in dust control, energy efficiency, and versatility, makes them an ideal choice for modern industrial applications. Shandong HeadPowder Engineering Co., Ltd. stands out as a trusted partner in providing customized pneumatic conveying solutions that meet the specific requirements of phenolic powder production. With its expertise and commitment to quality, HeadPowder helps clients optimize their production processes, enhance product quality, and improve overall operational efficiency. For businesses dealing with phenolic powder, investing in a reliable pneumatic conveying system is not just a choice but a necessity to stay competitive and maintain high standards in their operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top