When it comes to efficient material handling in industrial settings, the tote bag packed pneumatic conveying machine has emerged as a highly effective solution. This equipment is designed to transport bulk materials from one location to another using air pressure, offering a flexible and reliable method for various applications. In this article, we will explore what a tote bag packed pneumatic conveying machine is and delve into its fundamental design principles that make it a preferred choice in many industries.
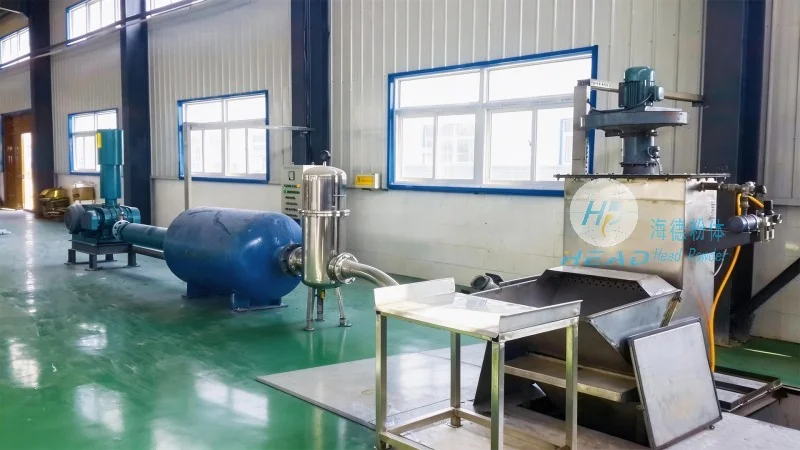
The tote bag packed pneumatic conveying machine, often referred to as a bulk bag or super sack pneumatic conveyor, is a system that utilizes air to move materials contained within a flexible tote bag. These tote bags are typically made of durable materials like polypropylene or other synthetic fabrics, capable of holding large quantities of bulk materials such as powders, granules, or even liquids in some cases. The machine operates by creating a pressure differential between the inlet and outlet, which draws the material from the tote bag into the conveying line and transports it to the desired destination.
At the core of a tote bag packed pneumatic conveying machine are several key components that work in harmony to ensure efficient material transport. The primary components include the inlet hopper, which connects to the tote bag and allows material to enter the system; the air compressor or blower, which generates the necessary air pressure; the conveying line, which transports the material and air mixture; and the discharge unit, which delivers the material to the target location. Additionally, the system may incorporate filters, cyclones, or other separation devices to ensure that the conveyed material remains clean and free from contaminants. The design of each component is critical to the overall performance and efficiency of the machine.
The design principles of a tote bag packed pneumatic conveying machine are centered around optimizing material flow, minimizing pressure drop, and ensuring the durability of the system. One of the fundamental principles is the use of a pressure or vacuum system to move materials. In a pressure system, the air compressor pushes air into the conveying line, creating positive pressure that forces the material out of the tote bag. In a vacuum system, a vacuum pump creates negative pressure, drawing material from the tote bag. The choice between pressure and vacuum depends on the specific application and the characteristics of the material being conveyed.
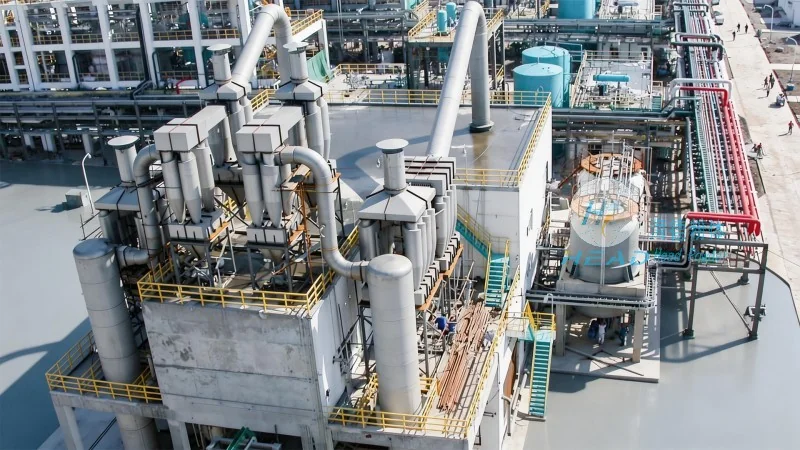
Another crucial design principle is the selection of the appropriate conveying velocity. The velocity of the air flow must be sufficient to lift and transport the material particles without causing excessive wear on the equipment or damaging the material. This is often determined by the size, shape, and density of the particles. Engineers use various formulas and empirical data to calculate the optimal conveying velocity for different materials, ensuring that the system operates efficiently and economically.
There are several advantages to using a tote bag packed pneumatic conveying machine in industrial applications. One of the most significant benefits is the flexibility it offers. Tote bags can be easily replaced or reused, allowing for the transport of different materials without the need for extensive system modifications. This makes the system ideal for applications where material types may change frequently or where bulk material storage is required. Additionally, the system is relatively compact and can be installed in various locations, making it suitable for both new and existing facilities.
Another advantage is the ability to handle a wide range of materials, from fine powders to coarse granules. The flexible tote bags can accommodate different particle sizes and shapes, while the pneumatic conveying system can be adjusted to suit the specific material characteristics. This versatility makes the machine a popular choice in industries such as food processing, pharmaceuticals, chemicals, and mining. Furthermore, the system is generally low maintenance, with fewer moving parts compared to other material handling equipment, reducing downtime and operational costs.
The tote bag packed pneumatic conveying machine is widely used across various industries due to its adaptability and efficiency. In the food and beverage industry, it is commonly used to transport ingredients like flour, sugar, and spices from storage to processing areas. The system ensures that the materials remain clean and free from contamination, which is critical in food processing. In the pharmaceutical industry, the machine is used to convey active pharmaceutical ingredients (APIs) and other sensitive materials, where maintaining purity and sterility is paramount.
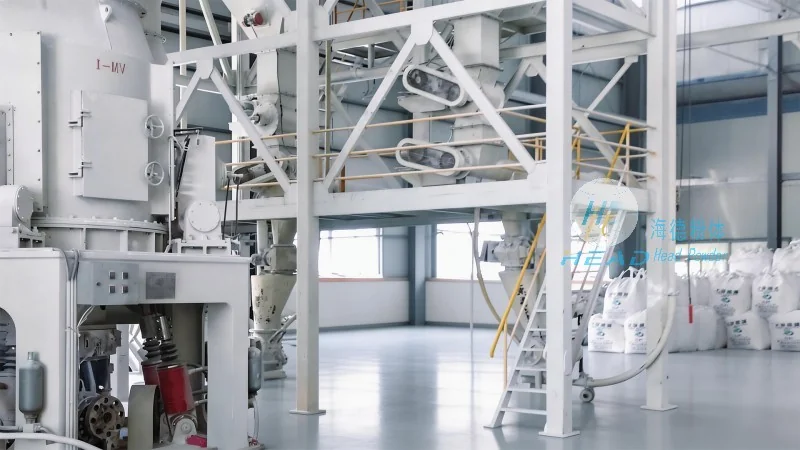
In the chemical industry, the system is employed to transport powders and granules such as fertilizers, pigments, and catalysts. The ability to handle abrasive materials without causing excessive wear on the equipment makes it a preferred choice. Similarly, in the mining and mineral processing industry, the machine is used to transport raw materials from storage to processing plants. The system's ability to handle large quantities of material efficiently makes it ideal for high-volume operations.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of material handling equipment, offers customized tote bag packed pneumatic conveying machines tailored to the specific needs of their clients. The company, based in Shandong, China, understands that each industrial application has unique requirements, and their design team works closely with customers to develop solutions that meet their operational and budgetary constraints. The machines can be integrated with existing systems, such as storage silos, processing lines, or packaging equipment, ensuring seamless material flow from start to finish.
Customization options include the selection of different tote bag materials, conveying line diameters, and air pressure levels. The company also provides after-sales support, including maintenance services and spare parts, to ensure that the equipment operates at peak efficiency throughout its lifespan. By partnering with Shandong HeadPowder Engineering Co., Ltd., businesses can benefit from a reliable and efficient material handling solution that enhances productivity and reduces operational costs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top