White sugar pneumatic conveying systems are critical in the sugar processing industry for efficiently transporting granulated sugar from storage to processing units. The design and components of these systems are tailored to handle the unique properties of white sugar, ensuring minimal product degradation and optimal operational efficiency. Understanding the key structural elements is essential for both system design and maintenance.
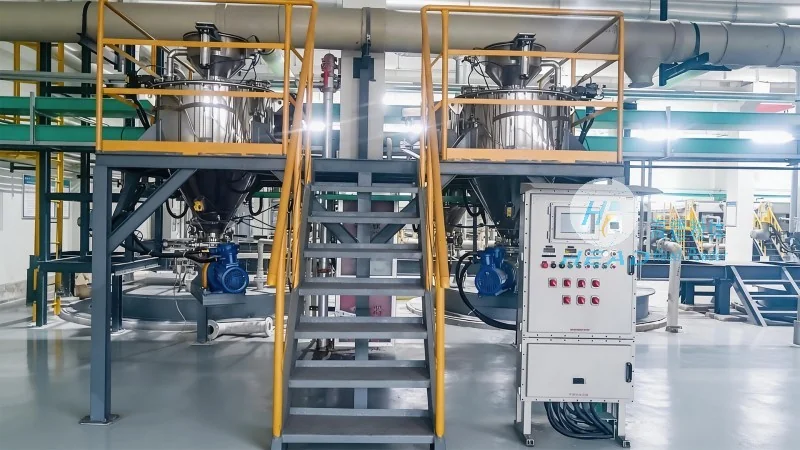
White sugar, with its fine granular structure and hygroscopic nature, requires specialized pneumatic conveying solutions to maintain quality and prevent caking or bridging. Pneumatic conveying systems use air to move sugar through a network of pipes, valves, and other components. The primary goal is to achieve high-velocity air flow that can lift and transport the sugar particles without causing excessive friction or pressure drops.
The headpowder, a leading manufacturer in the field, emphasizes that the main components of a white sugar pneumatic conveying system include the following: the air compressor or blower, which generates the necessary air pressure; the feed hopper, where sugar is loaded and metered; the conveying line, which consists of stainless steel pipes to prevent contamination and corrosion; and the control valves, which regulate the flow of air and sugar. Each component plays a vital role in the system's overall performance.
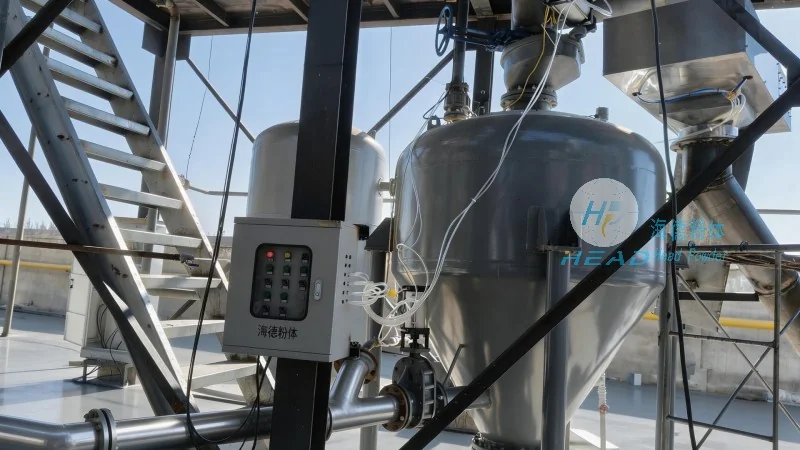
The feed hopper is a critical component for controlling the flow of white sugar into the conveying system. It is typically designed with a conical or rectangular shape to ensure uniform feeding. For white sugar, which can be prone to bridging, the hopper may include agitators or vibrators to prevent material from sticking to the walls. Metering devices, such as rotary valves or screw feeders, are used to regulate the amount of sugar entering the system, ensuring consistent flow rates. These devices help maintain the system's efficiency and prevent overloading or underloading of the conveying line.
The conveying line is the backbone of the pneumatic system, responsible for transporting the sugar particles through the air stream. Stainless steel pipes are commonly used due to their resistance to corrosion and ability to maintain product purity. The pipe diameter and length are carefully selected based on the sugar's flow characteristics and the required conveying distance. The system may include bends, elbows, and expansion joints to accommodate changes in direction and accommodate thermal expansion. Proper pipe design is crucial to minimize pressure losses and ensure the air-sugar mixture travels efficiently to the destination.
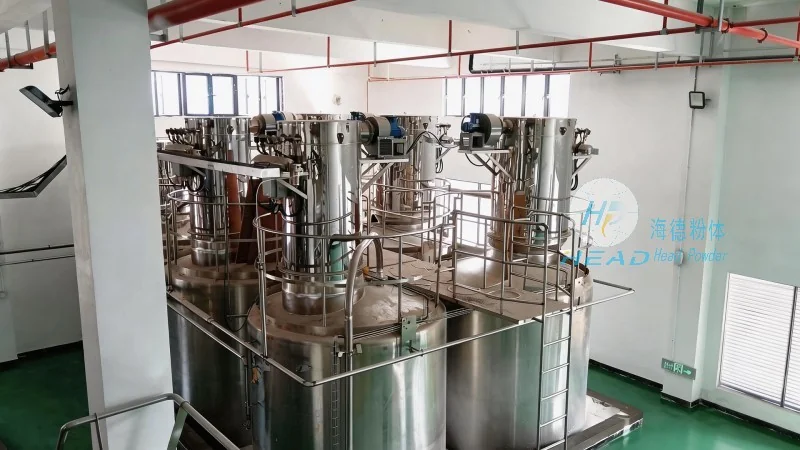
The air compressor or blower is the power source for the pneumatic conveying system. It generates the high-pressure air needed to lift and move the sugar particles. For white sugar applications, the blower is often chosen for its ability to provide a consistent, low-noise air flow. The unit is typically equipped with filters to remove moisture and particulates from the air, preventing contamination of the sugar. The compressor's capacity is matched to the system's requirements to ensure sufficient air pressure without excessive energy consumption. Regular maintenance of the blower, including filter replacement and lubrication, is essential to maintain optimal performance.
Control valves are integral to managing the flow of air and sugar within the system. These valves regulate the pressure and flow rate, ensuring the system operates within safe and efficient parameters. For white sugar, which can be sensitive to pressure changes, precise control is necessary to prevent product degradation. The system may include pressure relief valves to protect against overpressure and vacuum valves to maintain consistent suction. The control system, often integrated with sensors and automation, allows for real-time monitoring and adjustment of the conveying process. This ensures that the system can adapt to changes in feed rate or demand, maintaining consistent performance.
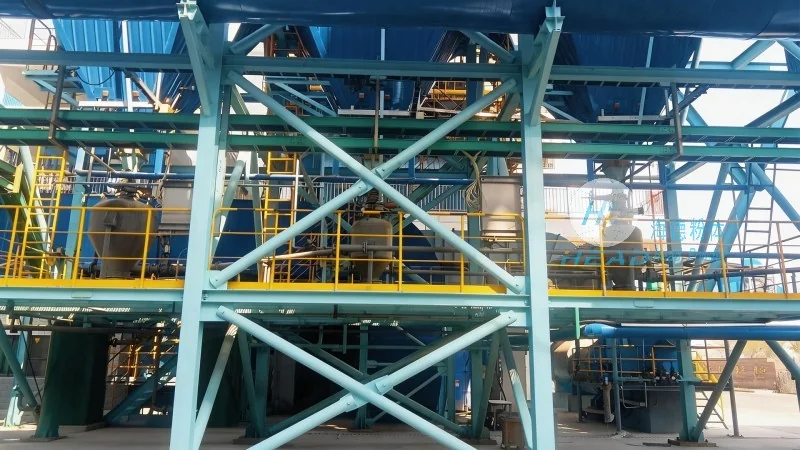
The final components of the pneumatic conveying system are the collection and discharge equipment. The receiving hopper or silo is designed to collect the sugar as it is conveyed to the processing unit. It may include a level indicator to monitor the sugar level and a discharge valve to control the flow out of the system. For white sugar, which can be prone to caking, the hopper may include a agitator or a rotary valve to prevent material from sticking to the walls. The discharge equipment is typically connected to the processing line, ensuring a smooth transition from the conveying system to the next stage of production. Proper design of the collection and discharge equipment is crucial to prevent product loss and maintain system efficiency.
Proper maintenance of the white sugar pneumatic conveying system is essential to ensure long-term performance and product quality. Regular cleaning of the feed hopper, conveying line, and collection hopper is necessary to prevent sugar buildup and contamination. The air compressor and blower should be inspected regularly for wear and tear, with filters replaced as needed. The control valves and sensors should be checked for proper operation to ensure accurate flow control. Additionally, the system should be monitored for pressure and flow variations, as these can indicate potential issues with the components. By following a regular maintenance schedule, the system can operate efficiently and minimize downtime.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top