Efficient and reliable material handling is a critical aspect of industrial operations, particularly when dealing with bulk materials like anhydrous sodium sulfate. Pneumatic conveying systems offer a versatile solution for transporting such materials, and understanding the nuances of negative pressure versus positive pressure systems is essential for optimizing performance and ensuring operational efficiency. This article delves into the technical aspects of anhydrous sodium sulfate pneumatic conveying, providing a comprehensive analysis of both negative and positive pressure systems and their practical applications.
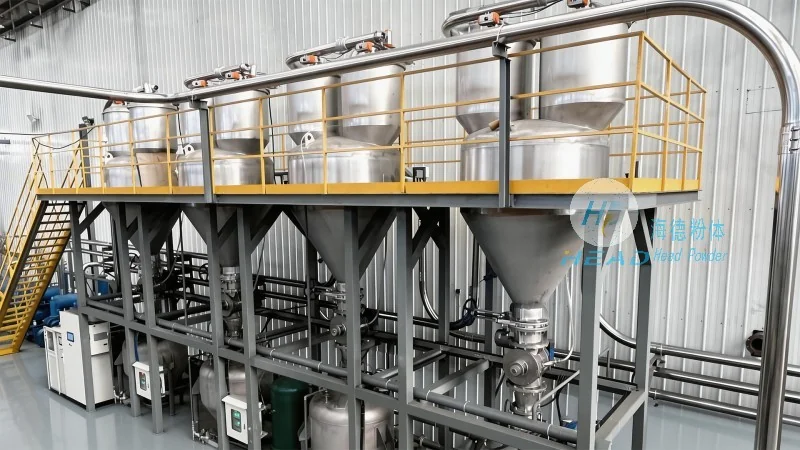
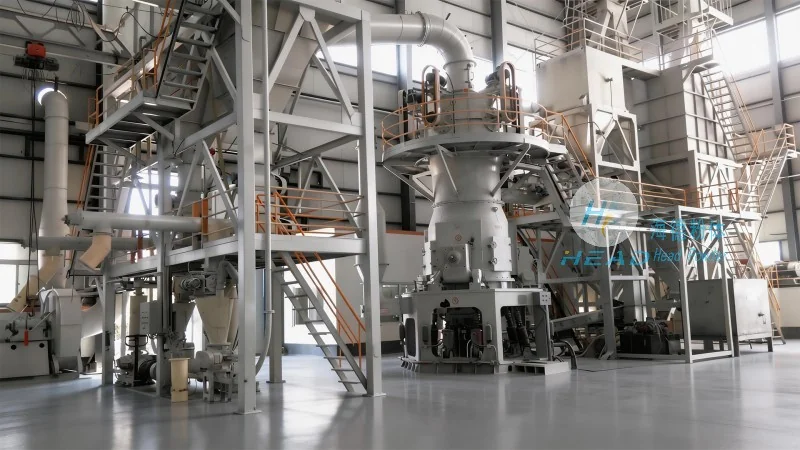
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying solutions. With a strong commitment to innovation and customer satisfaction, HeadPowder has established itself as a trusted partner in the chemical and material handling industries. The company's expertise lies in tailoring pneumatic conveying systems to meet the specific needs of clients, ensuring optimal performance and cost-effectiveness.
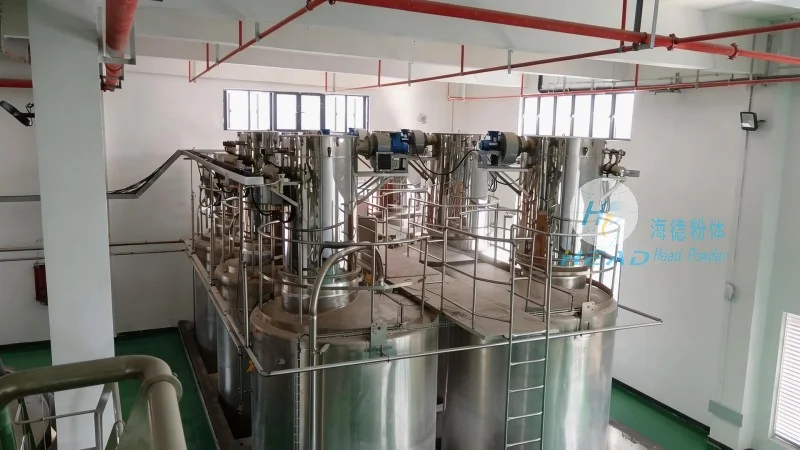
Negative pressure, or vacuum, pneumatic conveying systems are widely used for transporting anhydrous sodium sulfate due to their ability to handle materials over long distances and through complex piping networks. These systems operate by creating a vacuum at the receiving end, which draws the material from the source into the conveying line. The primary components of a negative pressure system include a vacuum pump, a material feed hopper, a conveying pipe, and a dust collector. The vacuum pump generates the necessary suction force, while the feed hopper ensures a consistent flow of material into the system. The conveying pipe transports the material from the source to the destination, and the dust collector captures any fine particles that may be present, preventing contamination and ensuring environmental compliance.
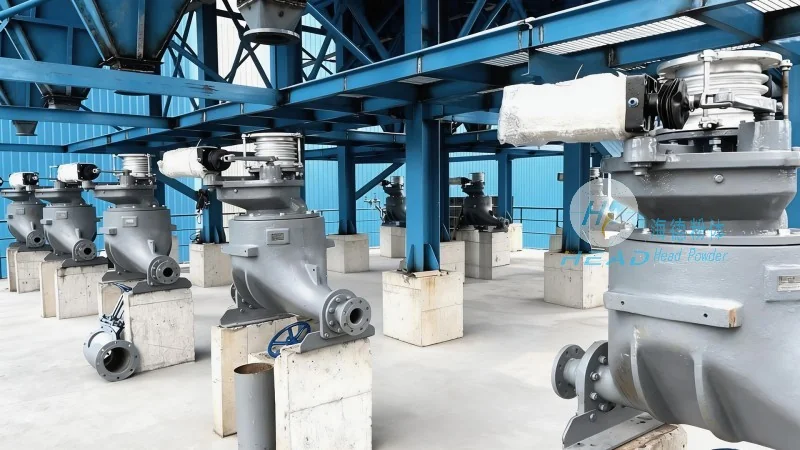
One of the key advantages of negative pressure systems is their ability to handle materials with high moisture content or those that are prone to caking. The vacuum environment helps to keep the material in a dry state, reducing the risk of blockages and ensuring smooth operation. Additionally, negative pressure systems are often more cost-effective for short to medium-distance conveying applications, as they require less energy compared to positive pressure systems. However, they may be less suitable for long-distance or high-capacity applications, as the vacuum pump's capacity and the system's overall efficiency can be limiting factors.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top