Pneumatic conveying systems have become a critical component in the logistics and material handling processes for sodium carbonate, a widely used chemical in various industrial applications. As a key player in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and implementing efficient solutions that leverage pneumatic technology to optimize the transportation of sodium carbonate. This approach not only enhances operational efficiency but also ensures the integrity and quality of the material throughout the supply chain.
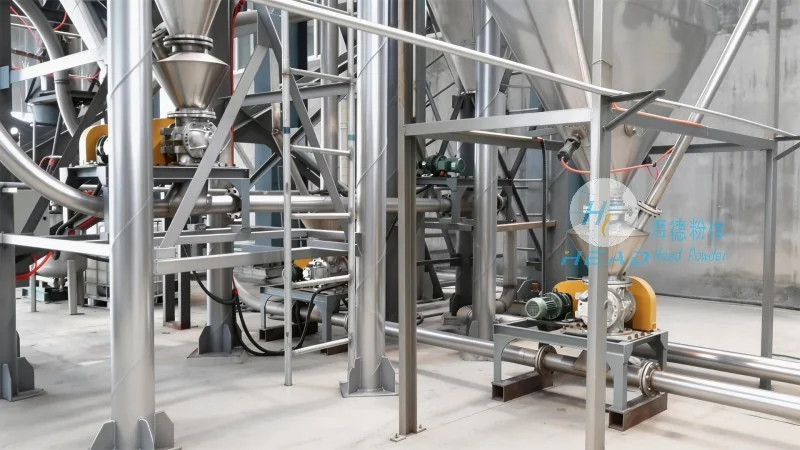
When compared to traditional bulk material handling methods such as belt conveyors or screw conveyors, pneumatic conveying offers several distinct advantages for sodium carbonate transportation. The primary benefit is the ability to transport the material over long distances with minimal maintenance requirements. This is particularly valuable in industrial settings where sodium carbonate is processed and distributed across large facilities or between different locations. Additionally, pneumatic systems can handle varying particle sizes and moisture content, making them versatile for different production stages. The enclosed nature of the system also helps in controlling dust and preventing contamination, which is crucial for maintaining the purity of sodium carbonate, especially in applications like glass manufacturing, detergents, and water treatment.
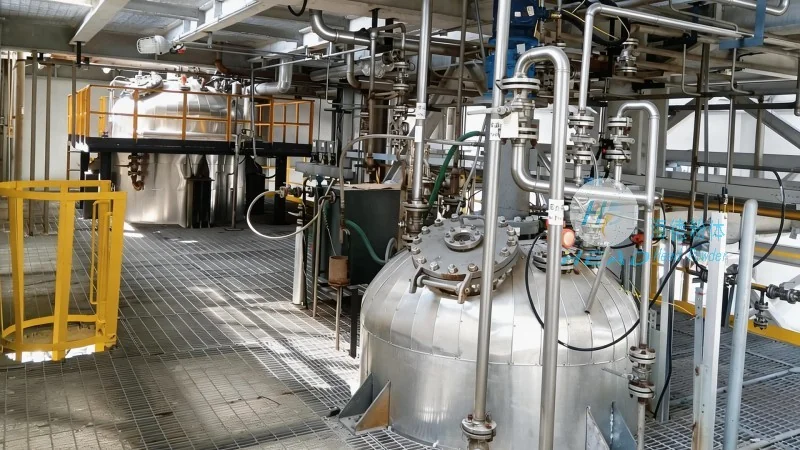
Shandong HeadPowder Engineering Co., Ltd. employs advanced engineering principles to design pneumatic conveying systems tailored to the specific needs of sodium carbonate handling. The system design typically includes a combination of positive pressure and negative pressure conveying modes, depending on the distance and layout of the facility. For instance, positive pressure systems are often used for short to medium distances, where air is blown through the pipeline to move the material, while negative pressure systems are suitable for longer distances or when the material needs to be transported from multiple sources to a central collection point. The pipeline network is constructed from corrosion-resistant materials such as stainless steel or special alloys to withstand the chemical properties of sodium carbonate and prevent degradation over time. Furthermore, the system incorporates advanced control mechanisms that monitor pressure, flow rate, and material level, ensuring smooth and continuous operation. This level of automation reduces the risk of downtime and improves overall productivity.
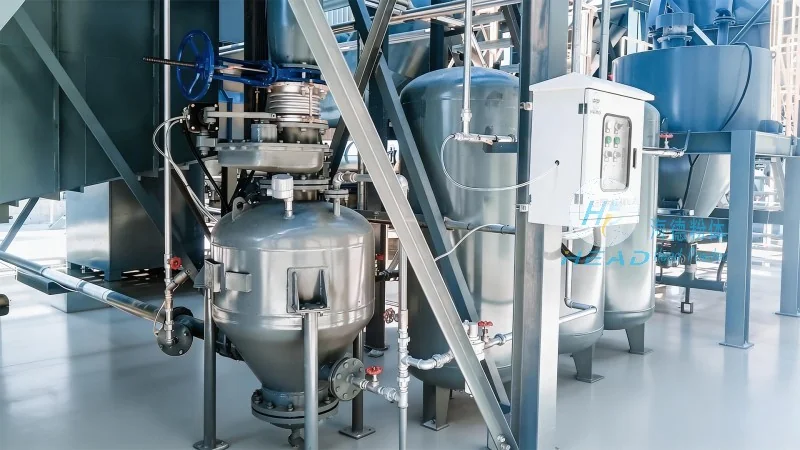
The effectiveness of pneumatic conveying in sodium carbonate transportation is evident in various industrial applications. In a glass manufacturing plant, for example, sodium carbonate is used as a key raw material in the production of glass. The pneumatic conveying system efficiently transports the material from storage silos to the glass furnace, ensuring a consistent supply without interruptions. Similarly, in detergent production facilities, sodium carbonate is a common ingredient, and the pneumatic system helps in delivering it to mixing and packaging units. These applications highlight the system's ability to handle large volumes of material while maintaining high standards of purity and efficiency. Case studies from clients of Shandong HeadPowder Engineering Co., Ltd. have shown significant improvements in operational costs and material handling times, underscoring the economic benefits of adopting pneumatic conveying technology.
Proper maintenance is essential to ensure the longevity and reliability of pneumatic conveying systems used for sodium carbonate transportation. Regular inspections of the pipeline and components are conducted to check for signs of wear and tear, particularly in areas where the material comes into contact with the system. Filters are regularly cleaned or replaced to prevent clogging, which can lead to system inefficiencies or breakdowns. The air compressor and other power components are also maintained according to manufacturer specifications to ensure optimal performance. By adhering to a structured maintenance schedule, the system's lifespan can be extended, and the risk of unexpected failures minimized. This proactive approach to maintenance aligns with the operational goals of industries that rely on consistent and reliable supply of sodium carbonate, such as chemical manufacturers and food processing companies.
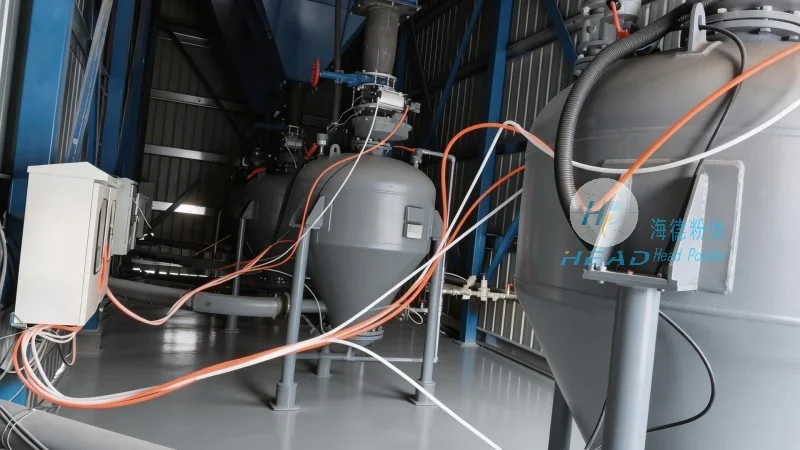
In conclusion, pneumatic conveying plays a vital role in the efficient and reliable transportation of sodium carbonate. The technology offers numerous advantages over traditional methods, including enhanced material handling capabilities, improved safety, and reduced operational costs. Shandong HeadPowder Engineering Co., Ltd. continues to innovate and refine its pneumatic conveying solutions to meet the evolving needs of the industry. As demand for sodium carbonate grows, the importance of efficient material handling systems will only increase, making pneumatic conveying an indispensable part of the supply chain. The company's commitment to quality and customer satisfaction ensures that its systems not only meet but exceed industry standards, providing long-term value to its clients.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top