Pharmaceutical powder pneumatic conveying technology is a critical component of material handling in the pharmaceutical industry. The efficient and safe transport of powder materials is essential for maintaining product quality, ensuring compliance with regulatory standards, and optimizing production processes. Among the various pneumatic conveying methods, vacuum and positive pressure systems are widely adopted due to their distinct operational characteristics and specific applications. This article provides a comprehensive overview of these two primary pneumatic conveying approaches, focusing on their principles, operational advantages, and practical implementations in pharmaceutical manufacturing.
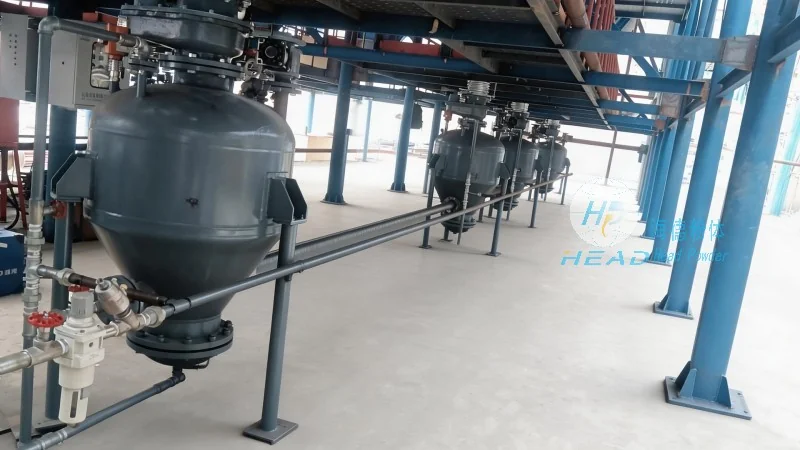
Pneumatic conveying systems utilize air or other gases to transport bulk materials, such as powders, granules, or fine particles, from one location to another. In the pharmaceutical sector, these systems are preferred for their ability to handle sensitive materials without contamination, minimize product degradation, and maintain a controlled environment. The choice between vacuum and positive pressure systems depends on factors like material properties, process requirements, and operational constraints. Both methods are designed to ensure reliable, hygienic, and efficient material transfer, which is paramount in pharmaceutical production.
Vacuum pneumatic conveying systems operate by creating a negative pressure (or vacuum) at the material pickup point, which draws the powder into the conveying line. This method is particularly suitable for applications where the material needs to be transported over relatively short distances or where the material is sensitive to high pressure or friction. The system typically consists of a vacuum pump, a material pickup hopper, a conveying line, and a discharge point. The vacuum is generated by the pump, which pulls air and material particles through the line, ensuring a continuous flow of powder. One of the key advantages of vacuum systems is their ability to handle fine powders and prevent product degradation due to low pressure and gentle handling. However, they may have limitations in terms of conveying distance and material throughput compared to positive pressure systems.
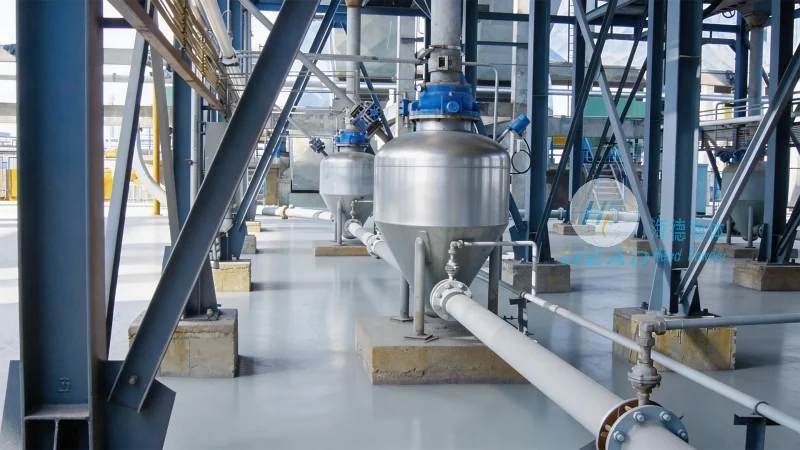
Positive pressure pneumatic conveying systems, on the other hand, operate by forcing air and material particles through the conveying line using a positive pressure source, such as a blower or a compressor. This method is ideal for transporting materials over longer distances and handling larger volumes of material. The system creates a positive pressure at the discharge end, which pushes the material through the line. Positive pressure systems are often preferred for applications involving abrasive or cohesive powders, as they can handle higher pressure and provide better control over material flow. Additionally, these systems are more suitable for conveying materials from multiple pickup points to a single discharge point, making them versatile for complex production lines. The primary advantage of positive pressure systems is their ability to achieve higher conveying rates and longer transport distances, which is crucial for large-scale pharmaceutical manufacturing.
The selection of a vacuum or positive pressure pneumatic conveying system depends on several critical factors. Material properties, such as particle size, density, and flowability, play a significant role in determining the most suitable system. For example, fine powders with low flowability may be better suited for vacuum systems due to their gentle handling, while cohesive or abrasive materials may require the higher pressure and control offered by positive pressure systems. Process requirements, including the distance between pickup and discharge points, required throughput, and environmental conditions, also influence the choice. Regulatory compliance is another critical consideration, as pharmaceutical manufacturers must adhere to stringent guidelines regarding product purity, contamination control, and system hygiene. The system's ability to maintain a sterile and clean environment is essential, and both vacuum and positive pressure systems can be designed to meet these standards with proper engineering and maintenance.
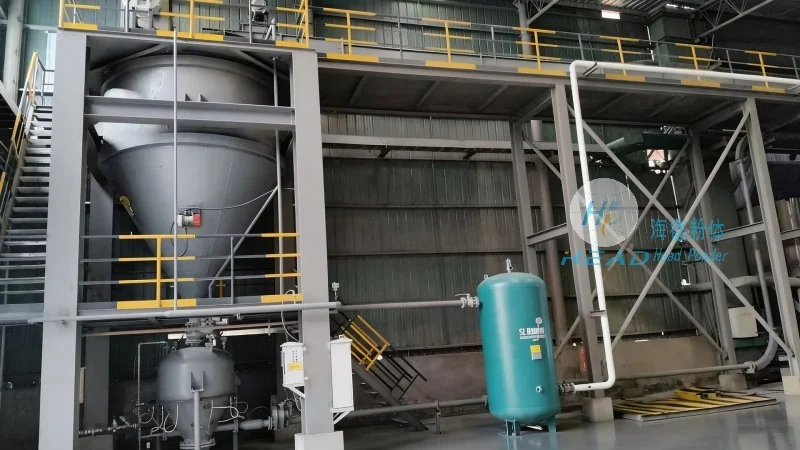
Both vacuum and positive pressure pneumatic conveying systems find extensive applications in pharmaceutical manufacturing. For instance, vacuum systems are commonly used for transporting active pharmaceutical ingredients (APIs), excipients, and other fine powders from storage hoppers to mixing or blending equipment. The gentle handling and low pressure of vacuum systems help preserve the integrity of these sensitive materials, ensuring consistent product quality. Positive pressure systems are often employed in larger-scale operations, such as the transport of bulk raw materials from storage silos to production lines or the conveying of finished products from packaging lines to storage areas. These systems are also used in processes like granulation, where the material needs to be transported over longer distances and handled with higher pressure to maintain flowability.
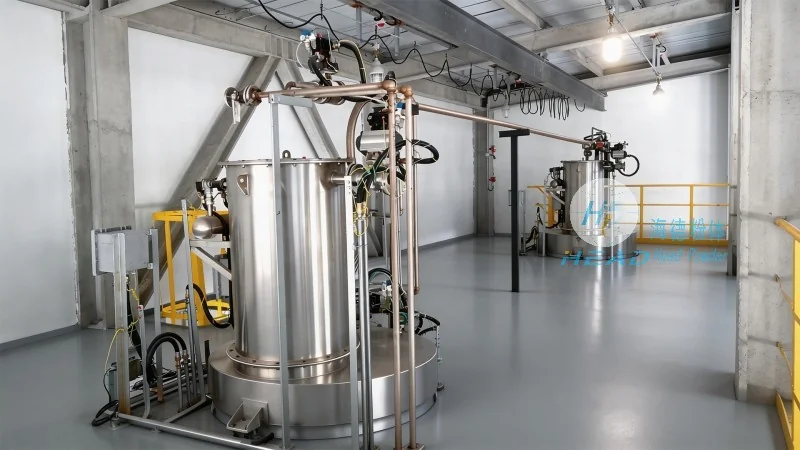
Each pneumatic conveying system has its own set of advantages and limitations. Vacuum systems excel in handling fine, sensitive powders and minimizing product degradation due to low pressure and gentle material handling. However, they may have limitations in terms of conveying distance and material throughput, making them less suitable for long-distance or high-volume applications. Positive pressure systems, conversely, offer higher conveying rates and longer transport distances, making them ideal for large-scale operations. They are better suited for handling abrasive or cohesive materials and can transport materials from multiple pickup points to a single discharge point. The main limitation of positive pressure systems is the potential for higher energy consumption and the need for more robust equipment to withstand higher pressures. Both systems require regular maintenance to ensure optimal performance and compliance with regulatory standards.
In conclusion, vacuum and positive pressure pneumatic conveying systems are essential technologies in pharmaceutical powder handling, each offering unique advantages tailored to specific applications. The choice between the two depends on material properties, process requirements, and operational constraints. Pharmaceutical manufacturers must carefully evaluate these factors to select the most appropriate system for their production needs. As the pharmaceutical industry continues to evolve, advancements in pneumatic conveying technology, such as improved control systems, enhanced material handling capabilities, and better integration with automation, will further optimize material transport processes. The continued development of these systems will contribute to improved product quality, increased efficiency, and compliance with regulatory standards, ensuring the safe and effective delivery of pharmaceutical products to patients worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top