Compound fertilizers are essential in modern agriculture, providing a balanced mix of nutrients to support crop growth. The efficient and reliable transport of these fertilizers from production sites to application points is crucial for optimizing agricultural productivity. Various conveying methods are employed in the industry, each with its own set of characteristics and applications. This article explores the different types of compound fertilizer conveying methods, with a particular focus on the advantages and features of pneumatic conveying.
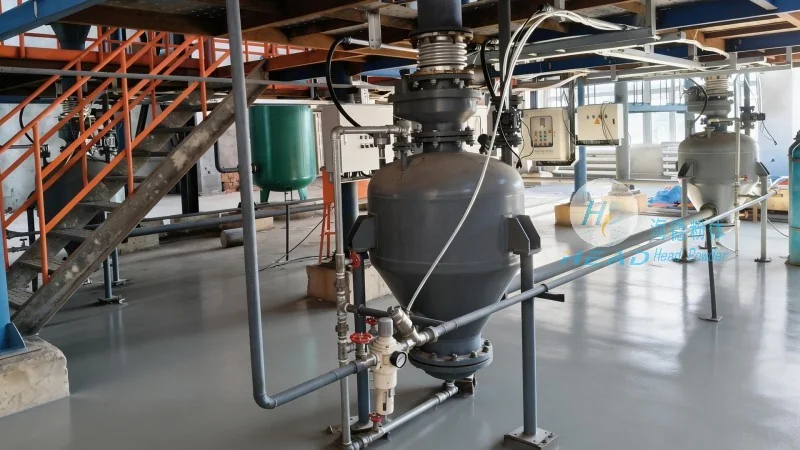
Compound fertilizers, which combine multiple nutrient elements into a single product, require specialized handling due to their granular or powder form. Conveying these materials involves moving them from storage silos, production lines, or storage facilities to distribution centers or application equipment. The primary methods used for compound fertilizer conveying include mechanical conveying (such as belt conveyors, screw conveyors, and bucket elevators) and pneumatic conveying. Each method has distinct advantages and limitations that make it suitable for different operational scenarios.
Pneumatic conveying, also known as air conveying, is a method that uses a stream of air to transport bulk materials like compound fertilizers through a pipeline system. This technology offers several key advantages that make it a preferred choice for many fertilizer producers and distributors. The primary benefits include high conveying capacity, minimal material degradation, and the ability to handle a wide range of particle sizes and moisture contents. Unlike mechanical conveyors, pneumatic systems do not require physical contact with the material, reducing the risk of contamination and wear on the fertilizer particles.
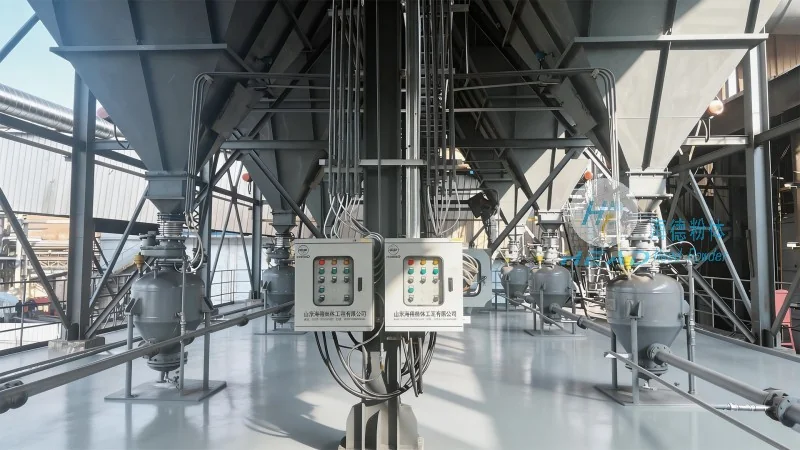
One of the most significant advantages of pneumatic conveying is its high efficiency in moving large volumes of compound fertilizers over long distances. The system can transport materials at high speeds, often reaching velocities of 20-30 meters per second, which significantly reduces the time required for material movement. This efficiency is particularly valuable in large-scale fertilizer operations where rapid turnover of inventory is essential. Additionally, pneumatic conveying systems are highly flexible, allowing for changes in the conveying route without major structural modifications. This adaptability makes them suitable for both new and existing facilities.
Another critical advantage is the preservation of fertilizer quality. Since the material is conveyed in a closed pipeline system, it is protected from environmental factors such as moisture, dust, and contamination. This is especially important for compound fertilizers, which can be sensitive to moisture absorption or chemical changes. The lack of physical contact with the conveying equipment also minimizes the risk of particle abrasion or breakage, ensuring that the final product maintains its intended nutrient composition and physical properties.
A pneumatic conveying system for compound fertilizers typically consists of several key components that work together to ensure efficient operation. The main parts include a material feed hopper, a blower or air compressor, a pipeline network, and a discharge unit. The feed hopper is designed to store and meter the fertilizer into the system, ensuring a consistent flow rate. The blower generates the necessary air pressure to move the material through the pipeline. The pipeline network, often made of stainless steel or other corrosion-resistant materials, is configured to handle the specific characteristics of the fertilizer, such as particle size and moisture content. The discharge unit, which may include a rotary valve or a pressure regulator, controls the release of the fertilizer at the destination point.
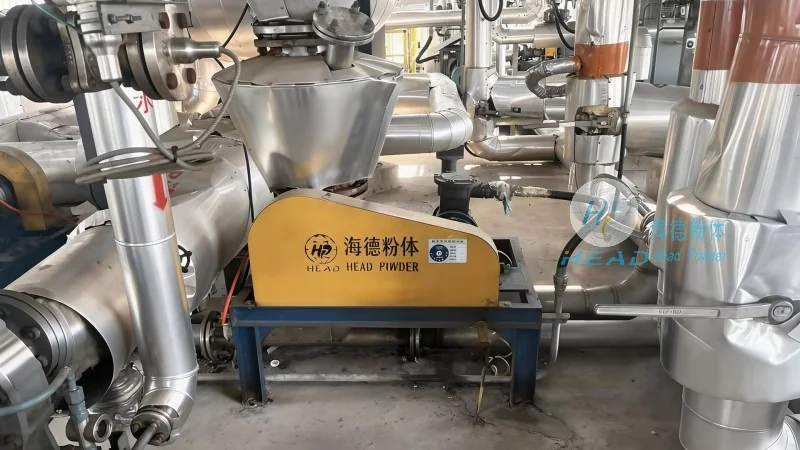
Pneumatic conveying is particularly well-suited for applications where compound fertilizers need to be transported over medium to long distances, often within industrial complexes or between different production units. For example, in large fertilizer plants, pneumatic systems are commonly used to move finished products from the granulation or coating lines to storage silos or loading facilities. The system's ability to handle both dry and slightly moist fertilizers makes it versatile for various production processes. Operational considerations for pneumatic conveying include maintaining proper air pressure and flow rates to prevent blockages or material degradation. Regular maintenance of the blower, pipeline, and feed equipment is also essential to ensure consistent performance and minimize downtime.
In conclusion, pneumatic conveying represents a highly effective and efficient method for transporting compound fertilizers. Its advantages in terms of capacity, material preservation, and flexibility make it a preferred choice for many industry professionals. As agricultural demands continue to grow, the need for reliable and efficient fertilizer handling systems becomes increasingly important. Pneumatic conveying, with its proven performance and adaptability, plays a vital role in meeting these needs, ensuring that compound fertilizers are delivered to the field in optimal condition. The technology, when properly designed and maintained, offers a sustainable solution for the long-term success of fertilizer operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top