Organic salt powder pneumatic conveying systems are advanced industrial equipment designed to transport organic salt powders efficiently and safely. These systems utilize pneumatic principles to move powders through a closed pipeline system, offering a reliable solution for material handling in various industrial applications. The following sections will explore the working principle and key features of such systems, providing insights into their functionality and benefits.
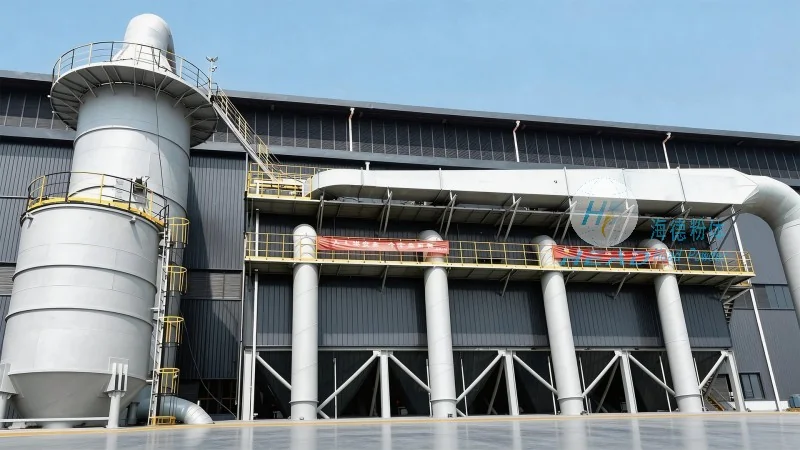
HeadPowder, a leading manufacturer in the field of powder handling equipment, specializes in developing and supplying high-quality organic salt powder pneumatic conveying systems. With a strong commitment to innovation and customer satisfaction, the company has established itself as a trusted partner for industries requiring efficient and reliable material transport solutions. HeadPowder Engineering Co., Ltd. is headquartered in Shandong, China, where it operates its production facilities and provides technical support to clients worldwide.
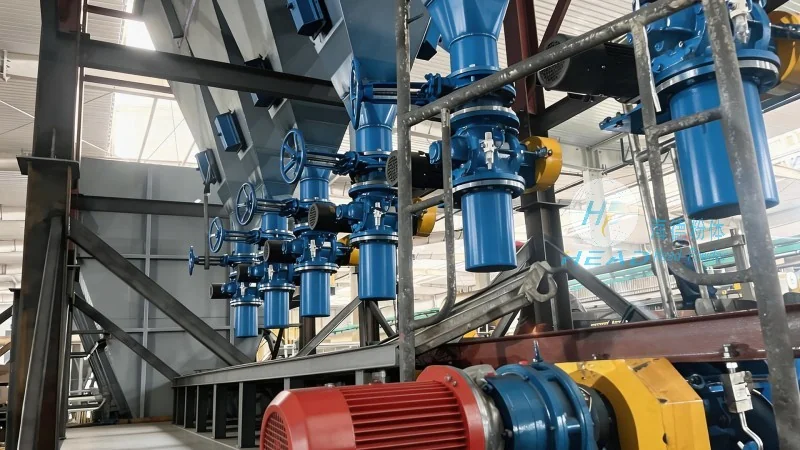
The core working principle of organic salt powder pneumatic conveying systems involves the use of compressed air or gas to create a flow that transports the powder particles through a pipeline. The process typically begins with the powder being fed into a hopper or feeder, where it is then introduced into the conveying line. Compressed air is then introduced into the system, creating a pressure differential that propels the powder forward. The velocity and pressure of the air are carefully controlled to ensure the powder is transported without degradation or segregation. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance and increasing operational efficiency. The system can operate in both positive and negative pressure modes, depending on the specific requirements of the application. Positive pressure systems push the powder through the line using compressed air, while negative pressure systems draw the powder using a vacuum. The choice between these modes depends on factors such as the distance of transport, the nature of the powder, and the need to prevent dust emissions.
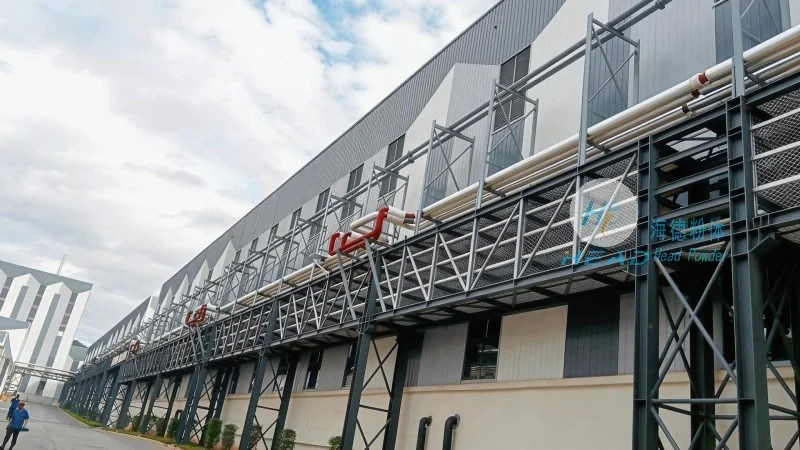
Organic salt powder pneumatic conveying systems offer several distinct advantages that make them ideal for handling organic salt powders. Firstly, they provide a dust-free and hygienic transport environment, which is crucial for maintaining product quality and meeting regulatory standards. The closed pipeline system prevents contamination from external sources and minimizes dust exposure for operators. Secondly, these systems are highly efficient in terms of energy consumption and operational costs. By eliminating the need for mechanical conveyors, they reduce energy usage and maintenance expenses over time. Thirdly, the systems are versatile and can handle a wide range of powder characteristics, including different particle sizes, moisture contents, and flow properties. This adaptability makes them suitable for various organic salt products, such as sodium bicarbonate, potassium chloride, or other similar powders. Additionally, the systems are designed for easy integration into existing production lines, allowing for seamless incorporation without significant modifications. The modular design of the equipment enables customization to meet specific client requirements, ensuring optimal performance for each application. Furthermore, the systems are equipped with advanced control systems that allow for precise regulation of air flow, pressure, and powder feed rates, enhancing process control and product consistency. Safety features, such as pressure relief valves and dust collection systems, are also integrated to ensure safe operation and compliance with safety regulations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top