For industries dealing with bulk sugar handling, efficient and reliable material transport is crucial. The sugar pneumatic conveying system, a key piece of equipment in the sugar processing sector, offers a solution that combines performance with operational flexibility. This article provides an overview of the structure and working principles of such systems, highlighting their importance in modern sugar production and processing facilities, and is presented by Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial conveying solutions based in China.
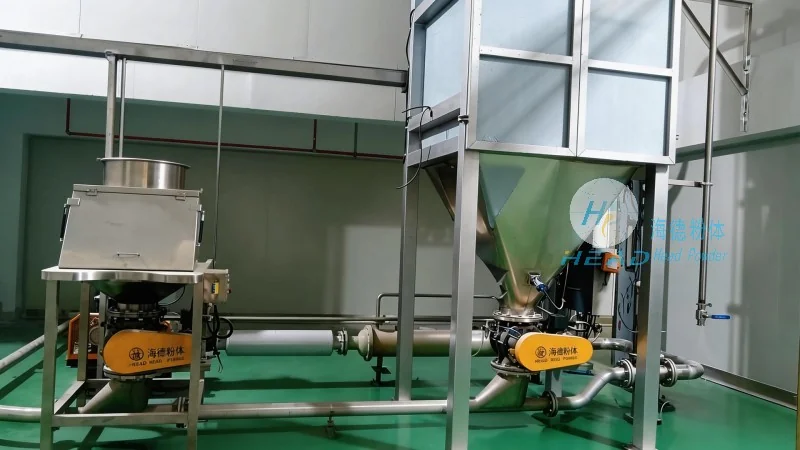
Pneumatic conveying systems are designed to transport bulk materials like sugar through a pipeline using air or other gases as the conveying medium. Unlike traditional mechanical conveying methods, which rely on belts, buckets, or screw conveyors, pneumatic systems utilize the force of compressed air to move material from one location to another. This method is particularly advantageous in sugar processing due to its ability to handle fine powders and granules without causing product degradation or contamination. The expertise of companies like Shandong HeadPowder Engineering Co., Ltd. has contributed to the development of advanced pneumatic systems tailored for the sugar industry's specific needs.
The structure of a typical sugar pneumatic conveying system comprises several essential components, each playing a critical role in the overall operation. These components include the material hopper, which serves as the storage and feeding unit; the air compressor, responsible for generating the necessary air pressure; the conveying line, which transports the sugar through the system; and the receiver or discharge hopper, where the material is collected after transport. Additionally, the system may incorporate accessories such as filters, cyclones, and control valves to ensure efficient and clean operation. Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing these components to meet the rigorous standards of the sugar industry.
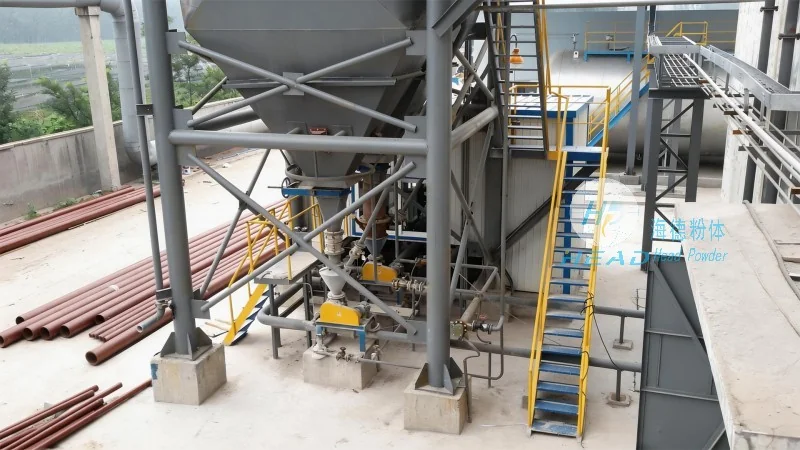
The operation of a sugar pneumatic conveying system follows a systematic process. Initially, the sugar is fed from the hopper into the conveying line under the influence of compressed air. The air, often introduced at a specific pressure and velocity, creates a flow that lifts and transports the sugar particles through the pipeline. As the material moves, it may encounter various components like filters or cyclones, which help separate any air from the product and maintain product purity. The system is designed to handle different sugar forms, including granulated, powdered, or crystalline sugar, adapting to the specific characteristics of each product. The engineering team at Shandong HeadPowder Engineering Co., Ltd. ensures that the system's design optimizes air usage and material transport efficiency.
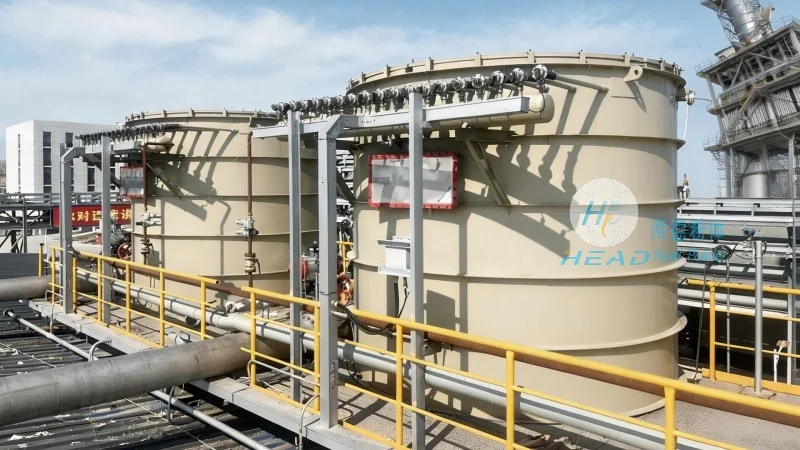
Implementing a pneumatic conveying system in sugar processing offers several benefits. Firstly, it minimizes product degradation by avoiding mechanical friction and impact, which can affect the quality and texture of sugar. Secondly, the system is highly flexible, allowing for changes in material flow rates and direction without significant modifications. Thirdly, it reduces labor costs and operational complexity compared to traditional mechanical systems, as it requires less maintenance and fewer moving parts. Moreover, pneumatic conveying can enhance safety by containing dust and preventing the spread of contaminants within the facility. These advantages make pneumatic conveying an ideal choice for sugar manufacturers seeking to improve their operational efficiency and product quality.
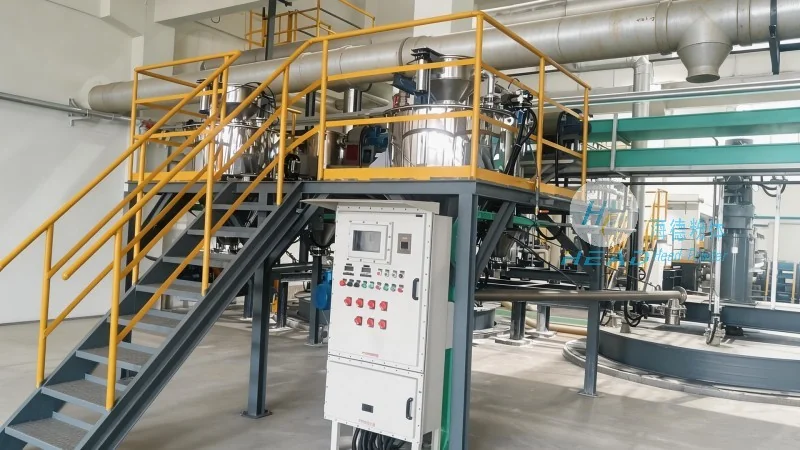
In sugar processing plants, pneumatic conveying systems are widely used for various applications, including raw material transport from storage silos to processing units, intermediate product transfer between different processing stages, and final product loading into packaging or storage containers. The system's ability to handle large volumes of sugar efficiently makes it ideal for high-throughput operations, where continuous and reliable material transport is essential. By integrating such systems, sugar manufacturers can improve their production efficiency, reduce downtime, and maintain consistent product quality. Shandong HeadPowder Engineering Co., Ltd. has successfully implemented these systems in numerous sugar processing facilities across China, demonstrating their effectiveness and reliability.
As an integral part of modern sugar processing infrastructure, pneumatic conveying systems provide a robust and efficient solution for bulk material handling. The combination of advanced engineering and careful design ensures that these systems operate reliably, maintaining product integrity while optimizing operational performance. For companies in the sugar industry, understanding the structure and working principles of pneumatic conveying systems is essential for making informed decisions about equipment selection and process optimization. With the right system in place, sugar manufacturers can enhance their operational capabilities and achieve higher levels of productivity and quality in their production processes. Shandong HeadPowder Engineering Co., Ltd. continues to lead in providing innovative and reliable pneumatic conveying solutions for the sugar industry, supporting its growth and development in China and beyond.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top