Pneumatic conveying systems are widely used in the agricultural and food processing industries for the efficient transport of bulk materials like rice grains. These systems utilize air pressure to move materials through a pipeline network, offering advantages such as dust control, hygienic operation, and the ability to handle fragile or sensitive products without mechanical contact. For rice grain handling, specialized equipment is designed to accommodate the unique characteristics of this material, ensuring minimal breakage and optimal flow characteristics.
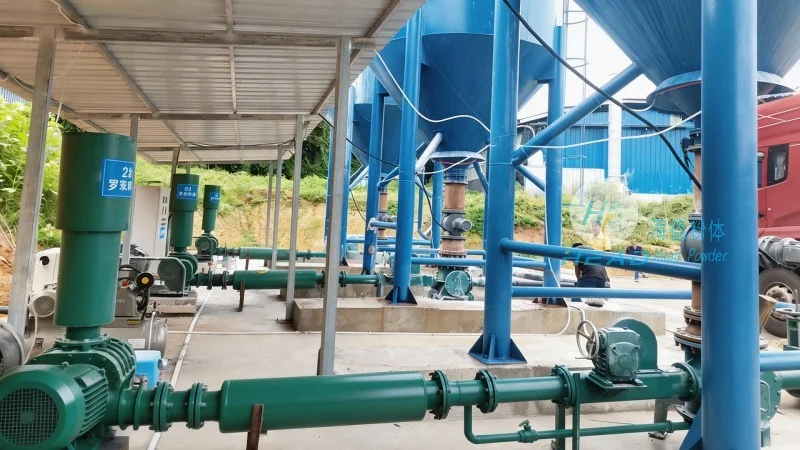
Rice grains are relatively small, lightweight, and have a smooth surface, which can affect their behavior in a pneumatic conveyor. The material's density, moisture content, and shape influence how it moves through the system. For instance, the uniform size of rice grains allows for consistent air flow, but their light weight means that higher air velocities or pressure differentials may be required to maintain proper transport. Additionally, the hygienic requirements for food processing mean that the conveying system must be designed to prevent contamination and ensure easy cleaning, which is a critical consideration for rice grain handling applications.
The fundamental principle of a pneumatic conveyor is the use of air to create a pressure differential that propels the material through a pipeline. In a typical system, a blower or compressor generates high-pressure air, which is introduced into the conveying line at the inlet point. The rice grains are then introduced into the system, either by gravity or through a hopper, and are entrained by the air flow. The air and material mixture travels through the pipeline, with the air providing the necessary force to move the grains to the discharge point. The system may include components such as a hopper, a rotary valve for material feeding, a filter to remove dust from the air, and a silencer to reduce noise. The design of the pipeline, including bends and vertical sections, is optimized to minimize pressure loss and ensure smooth material flow.
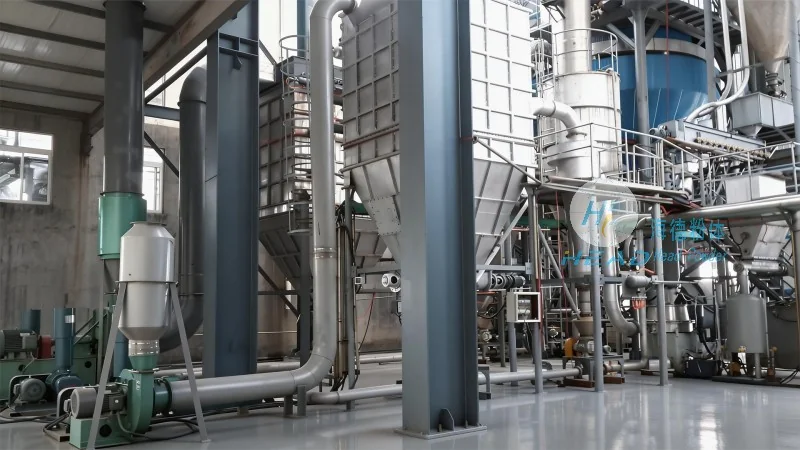
The operation of a rice grain pneumatic conveyor involves several key steps that ensure efficient and reliable material transport. First, the rice grains are loaded into the hopper, which is equipped with a rotary valve to control the flow rate. The rotary valve regulates the amount of material entering the conveying line, preventing overloading and maintaining consistent air flow. Next, the blower or compressor starts, generating the necessary air pressure to initiate the conveying process. The air is introduced into the inlet of the pipeline, creating a pressure differential that draws the rice grains into the system. As the grains are entrained by the air, they travel through the horizontal and vertical sections of the pipeline, with the air flow maintaining the material's movement. At the discharge point, the air and material mixture is separated, typically using a cyclone separator or a filter, and the rice grains are collected in a receiving bin. The air, now filtered of dust, is then discharged through a silencer to minimize noise pollution. Throughout the process, the system monitors pressure and flow rates to ensure optimal performance and to detect any issues that may affect the conveying efficiency.
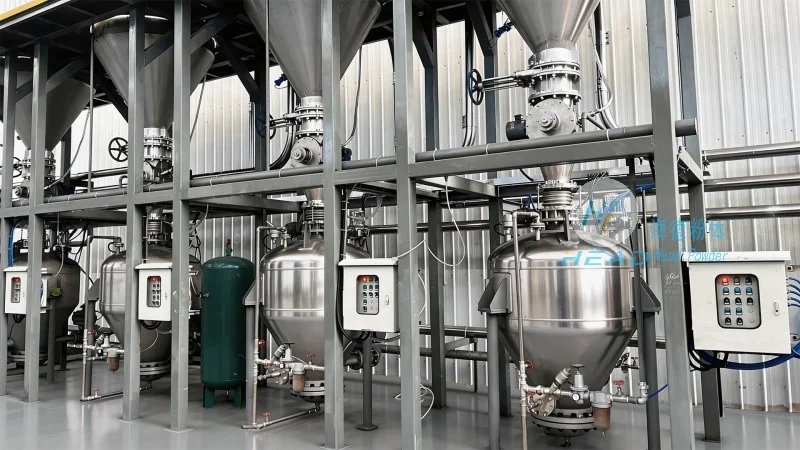
There are several advantages to using pneumatic conveying systems for rice grain material transport. First, the system is hygienic and dust-free, which is essential for food processing applications. The enclosed pipeline design prevents contamination from external sources and ensures that the rice grains remain clean and free from dust. Second, the system is efficient and can handle large volumes of material with minimal labor. The automated feeding and conveying process reduces the need for manual handling, which improves safety and reduces the risk of product damage. Third, the system is flexible and can be adapted to different production requirements. The pipeline can be extended or modified to accommodate changes in production volume or layout, making it a versatile solution for rice grain handling. Finally, the system is low maintenance, with components such as the blower and filter requiring periodic maintenance to ensure long-term operation. Companies like Shandong HeadPowder Engineering Co., Ltd. specialize in designing and manufacturing such systems, ensuring that the equipment meets the specific needs of rice grain processing facilities.
Pneumatic conveyors for rice grain material are used in various applications within the food processing industry. For example, in rice milling plants, the system is used to transport raw rice from storage silos to the milling equipment. The rice is conveyed through the pipeline to the milling machine, where it is processed into polished rice. In storage facilities, the system is used to move rice from the storage bins to the packaging line, ensuring a continuous supply of material. Additionally, the system is used in rice processing plants to transport rice to the packaging and labeling stations. These applications demonstrate the versatility and efficiency of pneumatic conveying systems for rice grain handling.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top