Dolomite, a calcium magnesium carbonate mineral, is widely used in various industrial applications such as cement production, steel manufacturing, and chemical processing. Efficient material handling is crucial for optimizing production efficiency and reducing operational costs. Pneumatic conveying systems offer a reliable and flexible solution for transporting dolomite and other bulk materials. This article provides an in-depth look at the operation process and working principle of a dolomite material pneumatic conveying line, highlighting key components, operational steps, and the technical advantages of such systems.
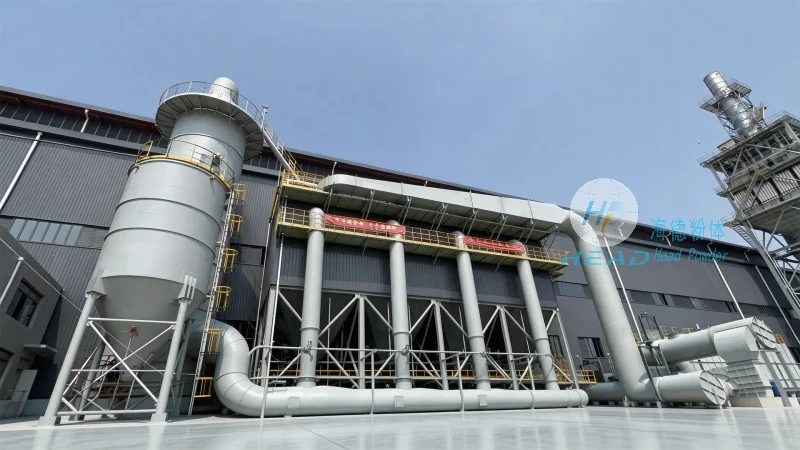
A typical dolomite pneumatic conveying line consists of several essential components that work in tandem to ensure smooth material transport. The main components include a hopper for material storage, a feeder to control the flow rate, a conveying pipeline, a blower or compressor to generate the air flow, a filter system to capture dust and particles, and a discharge unit for material release. Each component plays a critical role in maintaining the system's efficiency and safety. The hopper is designed to store dolomite in a controlled manner, preventing material bridging or clogging. The feeder, often a rotary valve or a screw feeder, regulates the material feed rate to match the system's air flow capacity. The conveying pipeline, usually made of stainless steel or plastic, ensures minimal material degradation and corrosion resistance. The blower or compressor provides the necessary air pressure to move the material through the pipeline. The filter system is crucial for maintaining air quality and preventing dust emissions. Finally, the discharge unit, such as a rotary valve or a gate valve, controls the release of dolomite at the destination point.
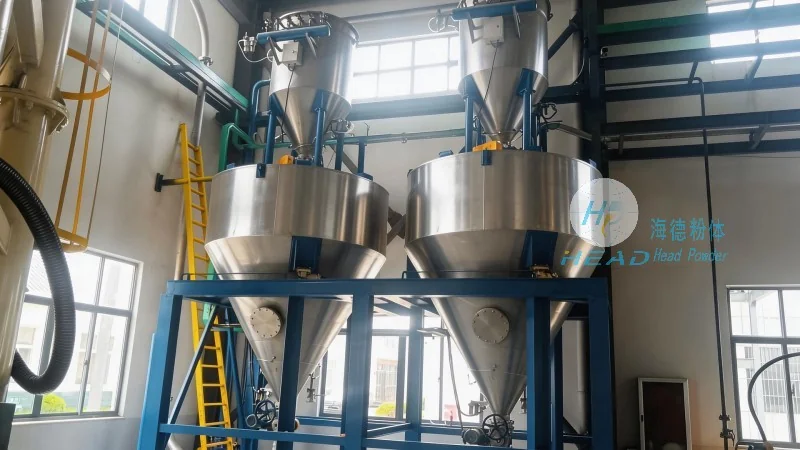
The operation of a dolomite material pneumatic conveying line involves a series of sequential steps that ensure consistent and reliable material transport. The process typically starts with the dolomite being loaded into the hopper. The feeder then regulates the flow of dolomite into the conveying pipeline, ensuring a steady feed rate. Simultaneously, the blower generates a high-pressure air stream that travels through the pipeline. As the dolomite particles are introduced into the air stream, they become entrained and carried along the pipeline. The air flow maintains the material in suspension, preventing it from settling or clogging the pipeline. The conveying system then transports the dolomite from the source point to the destination point, such as a storage silo or a processing unit. At the destination, the material is discharged through the discharge unit, and the air is filtered and recycled back to the blower. This continuous cycle ensures efficient material handling with minimal downtime. The operation process is designed to be automated, with sensors and controls monitoring the system's performance and adjusting parameters as needed to maintain optimal operation.
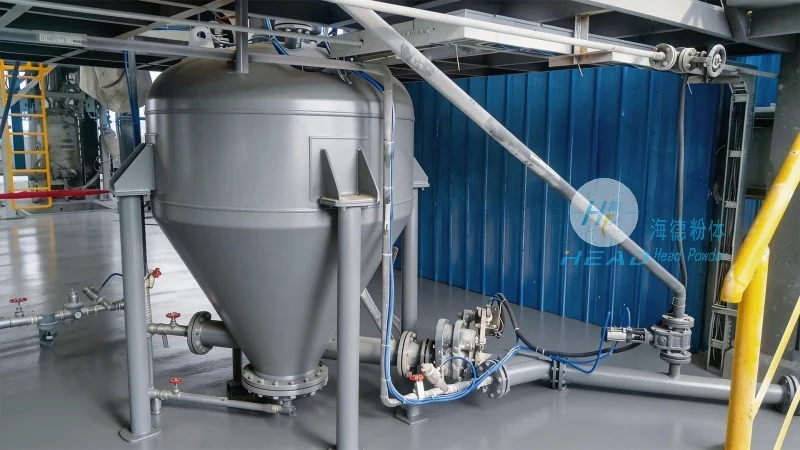
The working principle of a dolomite pneumatic conveying system is based on the principle of fluidization and suspension. When air is forced through the conveying pipeline at a sufficient velocity, it creates a fluidized bed of dolomite particles. The particles are suspended in the air stream, allowing them to be transported over long distances without the need for mechanical components like belts or buckets. This principle is particularly effective for handling fine or dusty materials like dolomite, as it minimizes material degradation and reduces the risk of clogging. The system operates under either positive pressure or negative pressure, depending on the application. Positive pressure systems use a blower to push the air and material through the pipeline, while negative pressure systems use a vacuum to draw the material into the pipeline. Both systems are suitable for dolomite transport, with positive pressure being more common for long-distance and high-capacity applications. The key to the system's efficiency is the balance between air velocity and material feed rate. If the air velocity is too low, the dolomite particles will settle and clog the pipeline. If the air velocity is too high, the system may experience excessive pressure drop and energy consumption. Proper system design and maintenance are essential to maintain this balance and ensure reliable operation.
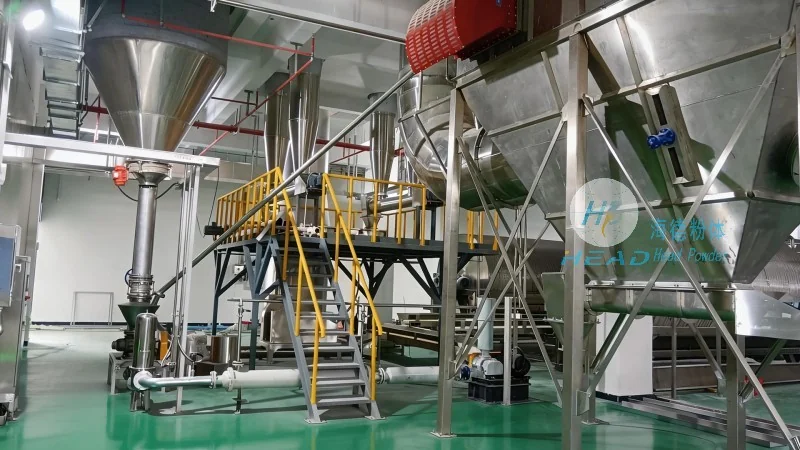
Implementing a pneumatic conveying system for dolomite material handling offers several advantages over traditional mechanical conveying methods. One of the primary benefits is the reduction in material degradation. Unlike belt or bucket conveyors, which can cause abrasion and breakage of dolomite particles, pneumatic systems transport materials in a fluidized state, preserving their integrity. This is particularly important for high-value or sensitive applications where particle size and quality are critical. Another advantage is the elimination of mechanical components, which reduces maintenance costs and downtime. Pneumatic systems have fewer moving parts, such as bearings and gears, which are prone to wear and failure. This results in lower operational costs and increased system reliability. Additionally, pneumatic conveying systems are more flexible in terms of layout and installation. They can be easily adapted to existing facilities or new construction, with minimal disruption to operations. The system can be configured to handle varying material feed rates and distances, making it suitable for a wide range of applications. Finally, pneumatic systems provide better control over material flow and dust management. The filter system captures dust particles, preventing emissions and maintaining a clean working environment. This is crucial for compliance with environmental regulations and ensuring workplace safety.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top