The phosphate fertilizer powder pneumatic conveying line is a critical piece of industrial equipment designed to transport bulk phosphate powder efficiently and safely. This system is widely used in the fertilizer manufacturing industry, where the reliable and low-cost movement of raw materials is essential for production continuity. The technology behind this line combines pneumatic principles with mechanical components to create a seamless material handling solution that minimizes downtime and operational costs.
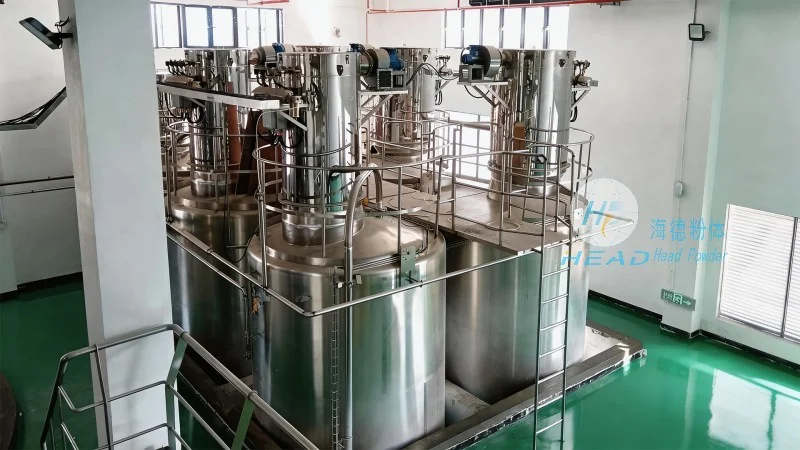
The pneumatic conveying line for phosphate fertilizer powder typically consists of several key components, each playing a vital role in the overall operation. The main components include the material hopper, which stores the phosphate powder; the air compressor or blower, which generates the necessary air pressure; the conveying pipe network, which transports the powder; and the receiver or discharge hopper, where the material is deposited. Additionally, the system may include filters to remove dust and moisture, and control valves to regulate air flow and pressure. Each component is carefully engineered to ensure compatibility with the abrasive and moisture-sensitive nature of phosphate fertilizer powder, ensuring long-term durability and performance.
The operation of the phosphate fertilizer powder pneumatic conveying line begins with the loading of phosphate powder into the material hopper. The hopper is designed with a sloped bottom to facilitate the flow of powder into the conveying line. Once the hopper is filled, the air compressor starts, generating a high-pressure air stream. The air stream is then introduced into the conveying pipe, creating a vacuum or pressure differential that draws the phosphate powder into the pipe. As the powder travels through the pipe, it is mixed with the air, forming a slurry-like mixture that is propelled towards the discharge point. The receiver or discharge hopper at the end of the line collects the powder, which can then be used for further processing or packaging. The entire process is automated, with sensors and control systems monitoring the flow rate, pressure, and temperature to ensure optimal performance and prevent blockages or other issues.
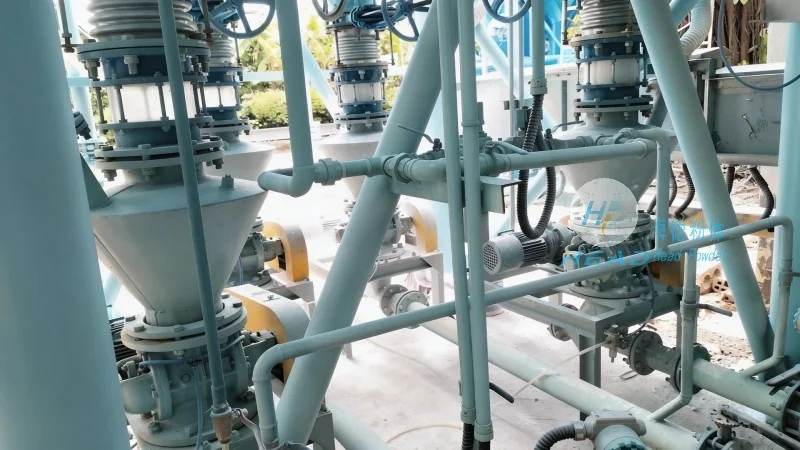
The working principle of the phosphate fertilizer powder pneumatic conveying line is based on the fundamental physics of fluid dynamics and particle transport. Pneumatic conveying uses compressed air to move solid particles through a pipeline. In the case of phosphate fertilizer powder, the system operates under either positive pressure or negative pressure (or a combination of both). Positive pressure systems use air compressors to force air and powder through the pipe, while negative pressure systems use vacuum pumps to draw the material into the pipe. The choice of system depends on factors such as the distance to be covered, the material characteristics, and the required flow rate. The key to efficient conveying is maintaining a consistent air-to-powder ratio, which ensures that the powder is fully suspended in the air stream and moves smoothly without settling or clogging. The system's design, including the pipe diameter, length, and bends, is optimized to minimize pressure losses and maintain the necessary velocity to keep the powder in suspension.
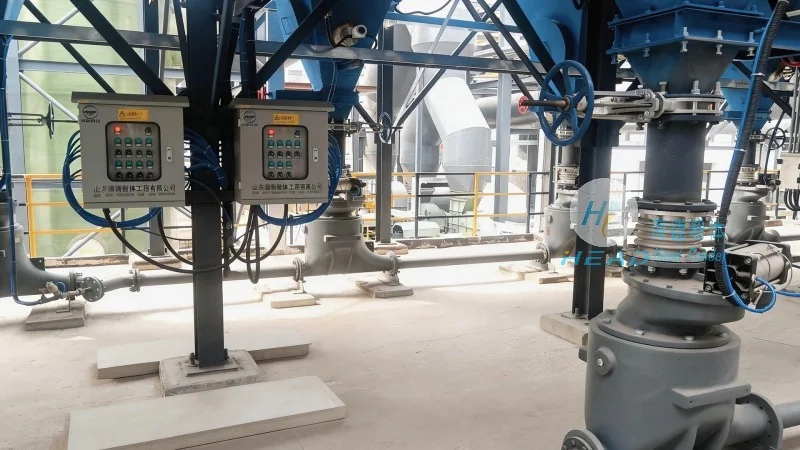
The phosphate fertilizer powder pneumatic conveying line offers several advantages over traditional material handling methods, such as belt conveyors or bucket elevators. One of the primary benefits is the ability to transport powder in a closed system, which reduces dust emissions and improves workplace safety. This is particularly important for phosphate fertilizer, which can be dusty and potentially hazardous. Additionally, pneumatic conveying systems are more flexible, as they can be easily reconfigured or expanded to accommodate changes in production volume or layout. The system also minimizes material degradation, as the powder is not subjected to high friction or impact, which can damage the particles and reduce their effectiveness. Furthermore, the automated nature of the system reduces labor costs and increases production efficiency, making it a cost-effective solution for industrial applications.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of industrial material handling equipment, including pneumatic conveying systems for phosphate fertilizer powder. With headquarters in Shandong, China, the company has established itself as a trusted partner in the fertilizer and chemical industries, providing high-quality, reliable equipment that meets the stringent requirements of modern manufacturing. HeadPowder's team of engineers and technicians specializes in designing and manufacturing customized pneumatic conveying lines tailored to the specific needs of each client. The company's commitment to innovation and quality has earned it a reputation for excellence in the industry, with a focus on delivering solutions that enhance operational efficiency and reduce costs. Whether for new installations or upgrades to existing facilities, headpowder offers comprehensive support, from design and installation to maintenance and after-sales service, ensuring that clients receive the best possible solution for their material handling needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top