Dilute phase pneumatic conveying systems are widely used in industrial applications for the efficient transport of powders and bulk materials over long distances. These systems operate by utilizing air or gas as the conveying medium, enabling the movement of particulate materials without the need for mechanical components like belts or buckets. The technology is particularly valuable in sectors such as pharmaceuticals, food processing, and chemical manufacturing, where maintaining product integrity and hygiene is critical.
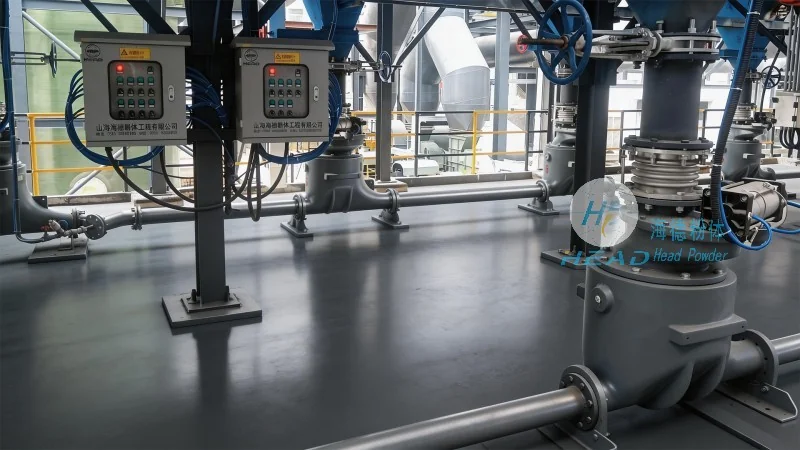
HeadPowder, a leading manufacturer in the field of pneumatic conveying equipment, specializes in the design, development, and installation of dilute phase systems. With a strong commitment to quality and innovation, the company has established itself as a trusted partner for businesses seeking reliable and efficient material handling solutions. HeadPowder's expertise lies in customizing systems to meet specific operational requirements, ensuring optimal performance and minimal downtime.
The core components of a dilute phase system include a blower or compressor, a hopper for material storage, a conveying line, and a receiver for the delivered material. The blower generates the necessary air pressure to transport the powder particles, which are suspended in the air stream. The hopper, typically equipped with a feeder, controls the flow of material into the system, while the conveying line, often made of stainless steel or other corrosion-resistant materials, ensures the material is transported without clogging or degradation.
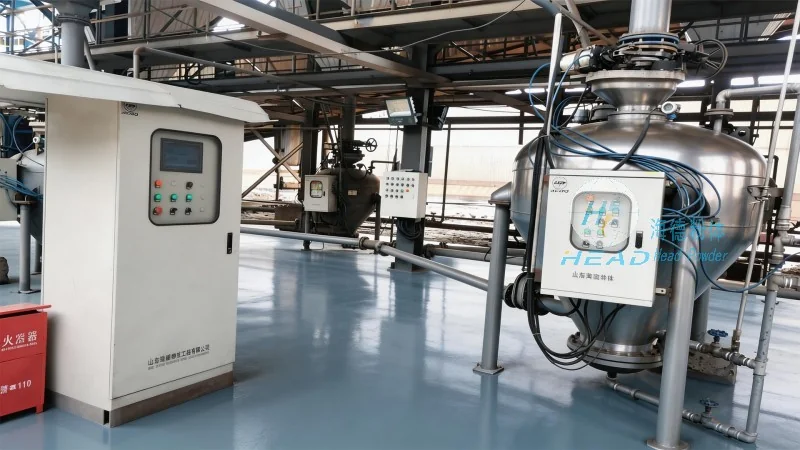
The operation process begins with the material being fed from the hopper into the conveying line. As the air is introduced by the blower, it creates a high-velocity stream that suspends the powder particles. The mixture of air and powder travels through the pipeline to the receiver, where the material is separated from the air by a cyclone or other separation device. The separated powder is collected in the receiver, while the air is either recirculated or discharged, depending on the system design. This continuous process allows for the efficient and controlled transport of large quantities of powder over considerable distances.
The working principle is based on the principle of fluidization and suspension. In a dilute phase system, the air velocity is maintained at a level that keeps the powder particles in a suspended state, preventing them from settling or clogging the pipeline. The key is to achieve a balance between the air flow rate and the material feed rate, ensuring that the particles are carried along without excessive pressure drop or energy consumption. This balance is crucial for maintaining system efficiency and minimizing operational costs.
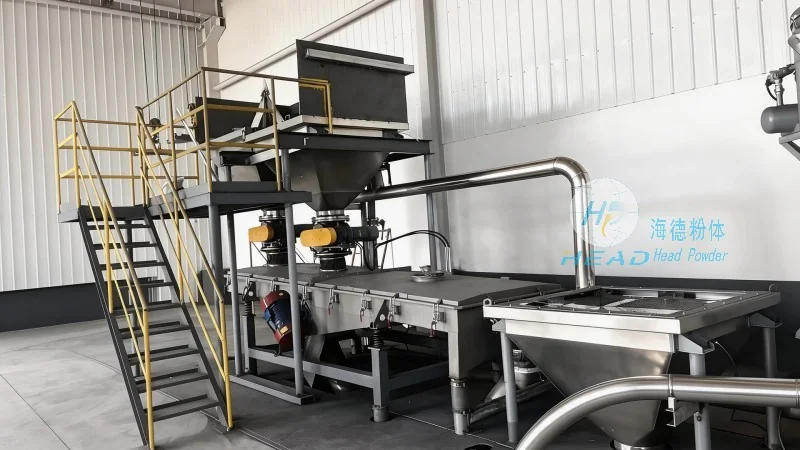
Dilute phase systems offer several advantages over other material handling methods. They provide a hygienic and dust-free environment, which is essential in industries like food and pharmaceuticals. The system is also flexible, allowing for changes in material type or flow rate without major modifications. Additionally, the absence of mechanical parts reduces maintenance requirements and extends the lifespan of the equipment. The ability to transport materials over long distances without the need for intermediate storage or handling points further enhances operational efficiency.
HeadPowder's dilute phase pneumatic conveying systems are applied in a wide range of industries. In the pharmaceutical sector, the systems are used for the transport of active pharmaceutical ingredients (APIs) and excipients, ensuring that the materials remain sterile and free from contamination. In food processing, the systems handle powders such as flour, sugar, and spices, maintaining the quality and freshness of the products. The chemical industry utilizes these systems for transporting bulk chemicals, while the mining and minerals sector benefits from efficient transport of ores and concentrates. HeadPowder's systems are tailored to meet the specific needs of each industry, ensuring optimal performance and compliance with industry standards.
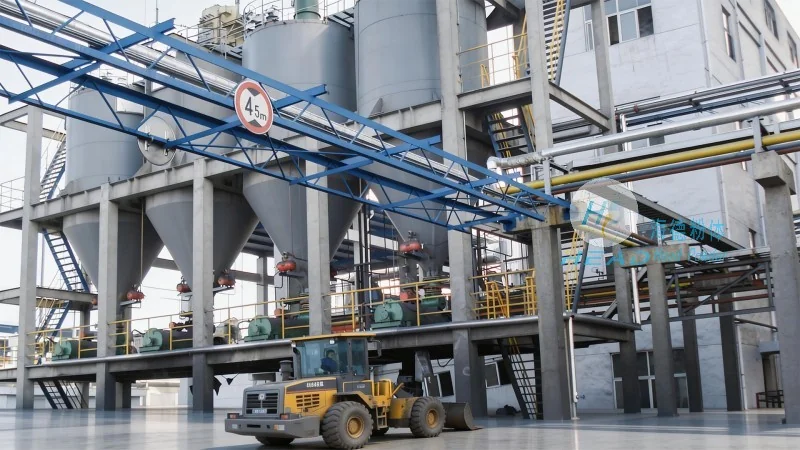
HeadPowder understands that each industrial application has unique requirements. Therefore, the company offers comprehensive customization services to design systems that meet specific operational parameters, such as material type, flow rate, and distance. The company's team of engineers works closely with clients to assess their needs and develop tailored solutions. After the system is designed, HeadPowder provides professional installation services, ensuring that the equipment is set up correctly and operates efficiently. The company also offers after-sales support, including maintenance and troubleshooting services, to ensure the long-term reliability of the systems.
Dilute phase pneumatic conveying systems, as offered by Shandong HeadPowder Engineering Co., Ltd., represent a sophisticated and efficient solution for the transport of powders and bulk materials. By leveraging advanced technology and a commitment to quality, HeadPowder provides systems that enhance operational efficiency, maintain product integrity, and reduce costs. The company's expertise in customizing and installing these systems ensures that clients receive solutions that are tailored to their specific needs, making them a preferred choice in the industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top