Ammonium bicarbonate, a white crystalline powder widely used in the chemical and agricultural industries, presents unique challenges during material handling due to its physical and chemical properties. This article explores the essential aspects of ammonium bicarbonate material handling and the critical design principles that ensure efficient, safe, and reliable operation in industrial settings.
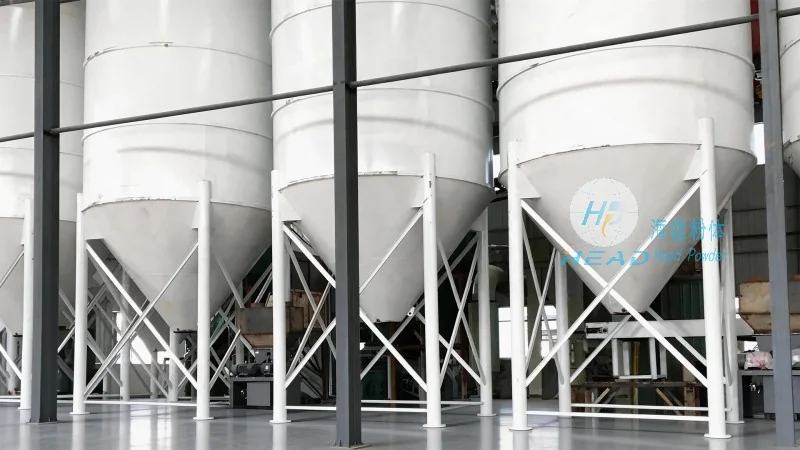
Ammonium bicarbonate (NH₄HCO₃) is a volatile compound that is hygroscopic and prone to caking. These characteristics make conventional material handling equipment unsuitable for its transport and storage. Effective handling requires specialized systems that address issues such as moisture absorption, blockage, and the release of ammonia gas. The design of such systems must prioritize both operational efficiency and safety, as improper handling can lead to product degradation, equipment damage, and environmental hazards.
The core design principles for ammonium bicarbonate material handling systems revolve around mitigating its inherent properties. One of the most critical considerations is the prevention of caking. This is achieved through the incorporation of anti-caking measures, such as temperature control (maintaining the material at a consistent temperature to prevent moisture-induced clumping) and mechanical agitation (using vibrators or rotating components to break up agglomerates). Additionally, the use of non-stick or coated surfaces in equipment like hoppers and chutes helps to minimize material adhesion.
Another essential design principle is the management of ammonia emissions. Ammonium bicarbonate is a source of ammonia gas, which can be hazardous if not properly contained. Therefore, all handling equipment must be equipped with effective sealing and ventilation systems. This includes the use of airtight hoppers, sealed conveyor belts, and exhaust systems that capture and neutralize ammonia fumes. Proper ventilation is crucial to maintain a safe working environment and prevent exposure to toxic gases.
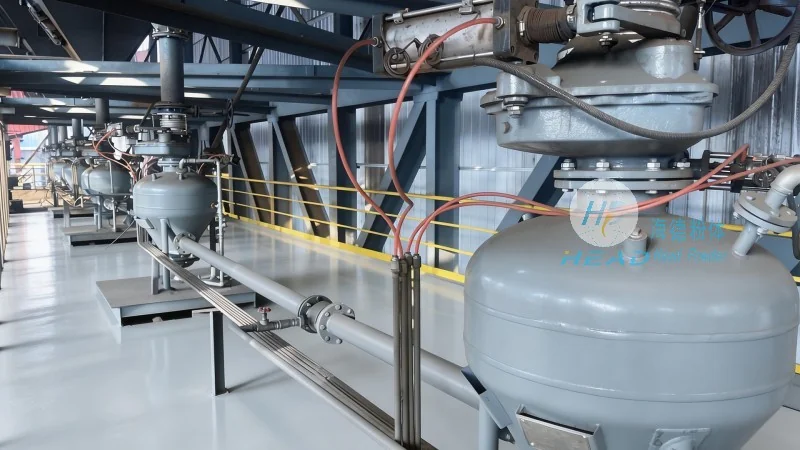
Efficient material flow is also a key design consideration. The choice of conveyor type depends on the specific application and the physical characteristics of the material. For example, screw conveyors are commonly used for vertical or horizontal transport due to their ability to handle bulk materials with minimal spillage. However, for longer distances or more complex layouts, pneumatic conveying systems may be preferred. These systems use air pressure to transport the material through pipes, which can be more effective in preventing caking and ensuring a consistent flow rate.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in designing and manufacturing customized material handling systems tailored to the unique needs of ammonium bicarbonate. With years of experience in the chemical industry, the company understands the challenges associated with handling this compound and provides comprehensive solutions that address all aspects of the process.
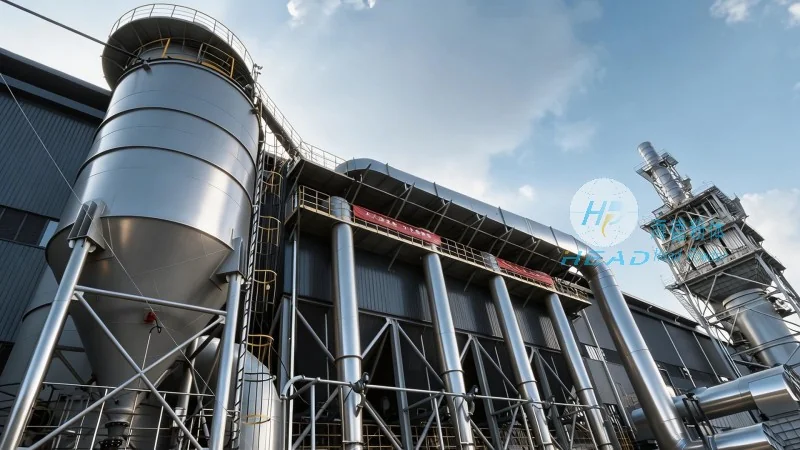
The company’s approach involves a thorough analysis of the client’s requirements, including the scale of production, the desired throughput, and the specific properties of the ammonium bicarbonate being handled. Based on this analysis, engineers at HeadPowder design systems that incorporate the latest technologies and best practices in material handling. This includes the integration of advanced control systems, monitoring equipment, and maintenance protocols to ensure optimal performance and longevity of the equipment.
HeadPowder’s systems are built with high-quality materials that are resistant to corrosion and chemical attack, ensuring durability in the harsh environment of ammonium bicarbonate processing. The company also provides ongoing support and maintenance services to clients, ensuring that the systems operate at peak efficiency throughout their lifespan. This commitment to quality and customer service has made HeadPowder a trusted partner for businesses in the agricultural and chemical sectors.
In conclusion, the proper handling of ammonium bicarbonate requires a deep understanding of its properties and the implementation of specialized design principles. From anti-caking measures to ammonia emission control, every aspect of the system must be carefully considered to ensure safety and efficiency. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing these solutions, leveraging their expertise to deliver customized systems that meet the unique demands of the industry. By adhering to these design principles and partnering with experienced manufacturers, businesses can ensure the safe and efficient transport of ammonium bicarbonate, supporting their operations and contributing to the success of the chemical and agricultural industries.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top