Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading enterprise in the field of material handling technology, headquartered in Shandong, China. The company specializes in the research, development, and production of advanced material transport systems, including vacuum suction type equipment that efficiently handles various bulk materials in industrial settings.
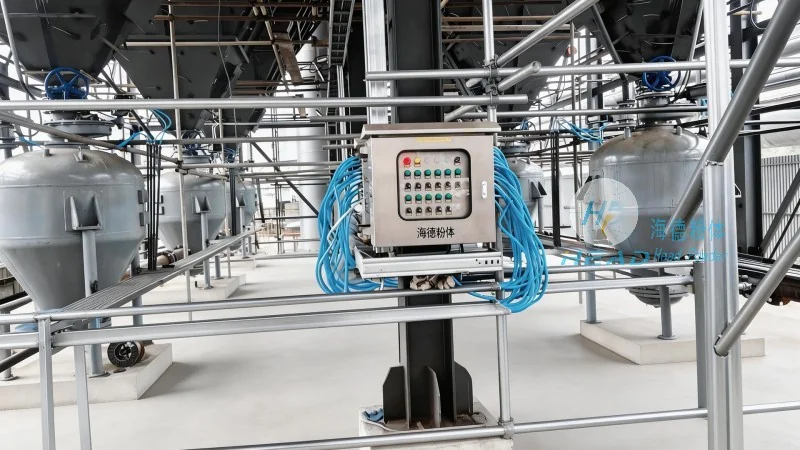
Vacuum suction material handling systems represent a sophisticated approach to transporting loose bulk materials over long distances or across different work areas. Unlike traditional conveyor systems that rely on mechanical force, these systems utilize negative pressure to draw materials into a sealed pipeline. This method offers significant advantages in terms of safety, flexibility, and environmental protection, making it ideal for applications in pharmaceuticals, food processing, chemicals, and other industries where material contamination and dust control are critical.
The core of a vacuum suction system is the vacuum pump, which generates a pressure lower than atmospheric pressure. This negative pressure is then distributed through a network of pipes and connected to suction points (such as nozzles or hoppers) where the material is located. As the vacuum pump operates, it creates a pressure differential that pulls the material particles into the pipeline. The material is then carried along the pipeline by the flow of air or a carrier gas, moving towards the discharge point. The system typically includes a filter or separator to remove dust and particles from the air stream before it is released back into the environment or recirculated.
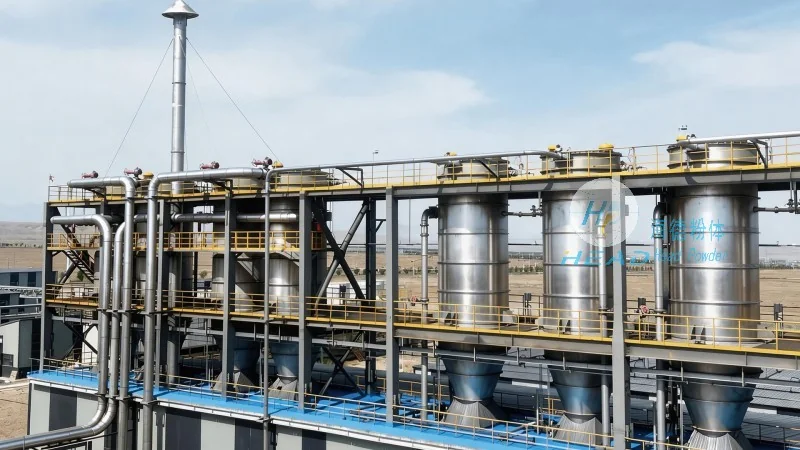
The operation of a vacuum suction material handling system follows a systematic sequence to ensure efficient and safe material transport. The process begins with the activation of the vacuum pump, which establishes the necessary negative pressure in the system. Once the pump is running, the operator positions the suction nozzle over the material source, such as a hopper or a storage bin. The nozzle is then activated, and the material is drawn into the pipeline. The material travels through the pipeline network, which may include bends, branches, and vertical sections, to reach the discharge point. At the discharge end, a valve or other control mechanism regulates the release of the material into a receiving container or processing unit. The system continues to operate until the material is fully transferred, after which the pump is shut down and the system is depressurized.
Several critical components work in tandem to ensure the proper functioning of the vacuum suction system. The vacuum pump is the primary power source, responsible for creating the negative pressure. Suction nozzles or hoppers are the entry points for the material, designed to efficiently capture and draw in the bulk material. The pipeline system, often made of flexible or rigid materials like PVC or metal, transports the material and air mixture. Filters or cyclones are used to separate the material from the air, preventing dust and particles from being released into the environment. Control valves and switches regulate the flow of material and air, allowing for precise control over the system's operation. Additionally, safety features such as pressure relief valves and emergency shut-off mechanisms are integrated to protect the system and operators from potential hazards.
Compared to traditional material handling methods, vacuum suction systems offer several key advantages. First, they provide a dust-free and clean operation environment, which is essential in industries like food and pharmaceuticals where contamination control is paramount. Second, the system is highly flexible, as the suction points and discharge points can be easily repositioned or added to the existing pipeline network without major modifications. Third, the system is energy-efficient, as it uses less power compared to mechanical conveyors that require continuous mechanical force. Fourth, it is safe for handling hazardous materials, as the sealed pipeline prevents exposure to operators. Finally, the system is environmentally friendly, as it reduces the need for open-air handling and minimizes dust emissions.
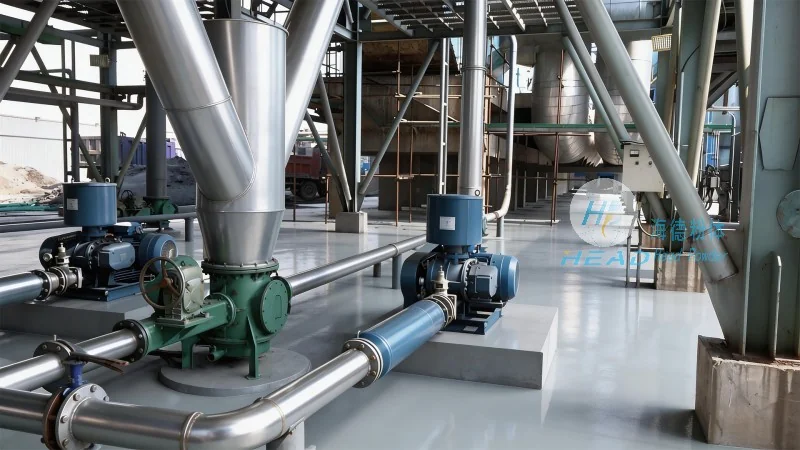
Vacuum suction material handling systems are widely used in various industries due to their versatility and effectiveness. In the pharmaceutical industry, they are used to transport powders and granules in cleanroom environments, ensuring product purity and safety. In the food processing industry, they handle ingredients like flour, sugar, and spices, maintaining hygiene standards. The chemical industry utilizes these systems for transporting powders and solids in hazardous or sensitive applications. Additionally, they are employed in the agricultural sector for handling grains and other bulk agricultural products. The system's ability to handle a wide range of materials, from fine powders to coarse granules, makes it suitable for diverse industrial needs.
To ensure the long-term performance and safety of the vacuum suction system, regular maintenance is essential. This includes checking the vacuum pump for proper operation, inspecting the pipeline for leaks or blockages, cleaning the filters regularly, and lubricating moving parts. Safety is a critical aspect of operating such systems, as high vacuum pressures and moving components can pose risks. Operators must follow proper safety protocols, including wearing appropriate personal protective equipment (PPE), ensuring the system is depressurized before maintenance, and avoiding the use of tools or objects that could be drawn into the pipeline. Additionally, regular safety inspections and training for operators are recommended to minimize the risk of accidents.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top