Shandong HeadPowder Engineering Co., Ltd., a leading enterprise in the field of chemical engineering and material handling solutions, specializes in the design, manufacturing, and installation of advanced systems for transporting and processing potassium carbonate fertilizer. This article provides a detailed overview of the operation process and working principle of their material handling system, highlighting the key components, operational flow, and technical aspects that ensure efficient and reliable fertilizer transport.
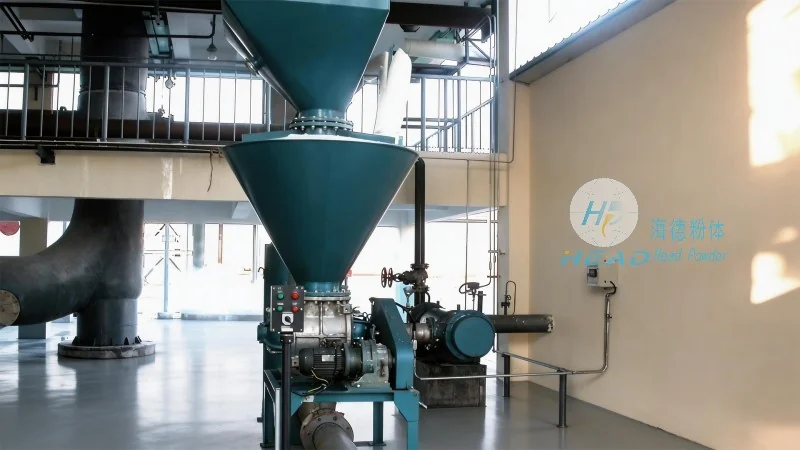
The potassium carbonate fertilizer material handling system is engineered to handle bulk materials with precision and efficiency. The system typically consists of several critical components, including feed hoppers, conveyor belts, rotary valves, pneumatic or mechanical conveyors, and storage silos. Each component is meticulously designed to work in tandem, ensuring seamless material flow from the initial loading point to the final discharge or storage location. The feed hopper is responsible for receiving raw potassium carbonate fertilizer from storage silos or bulk trucks, while the conveyor belts transport the material horizontally or at an incline. Rotary valves act as gateways, controlling the flow rate and preventing backflow, which is crucial for maintaining system stability and preventing material degradation.
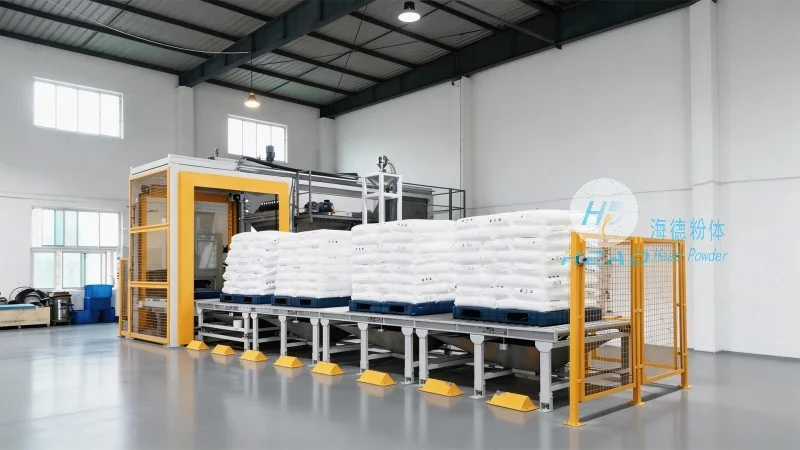
The operation of the potassium carbonate fertilizer material handling system follows a systematic, automated process that minimizes human intervention and maximizes throughput. The process begins with the loading of raw material into the feed hopper. Once the hopper is filled to a predetermined level, the conveyor system activates, transporting the material to the next stage. The rotary valve then regulates the flow, ensuring a consistent feed rate to the pneumatic or mechanical conveyor. The conveyor then transports the material to the storage silos or the final discharge point. The system is equipped with sensors and control panels that monitor key parameters such as flow rate, pressure, and temperature, allowing for real-time adjustments to maintain optimal performance. The entire process is controlled by a programmable logic controller (PLC), which coordinates the operation of all components and ensures smooth, continuous operation. The system also includes safety features such as emergency stop buttons and overload protection to prevent accidents and equipment damage.
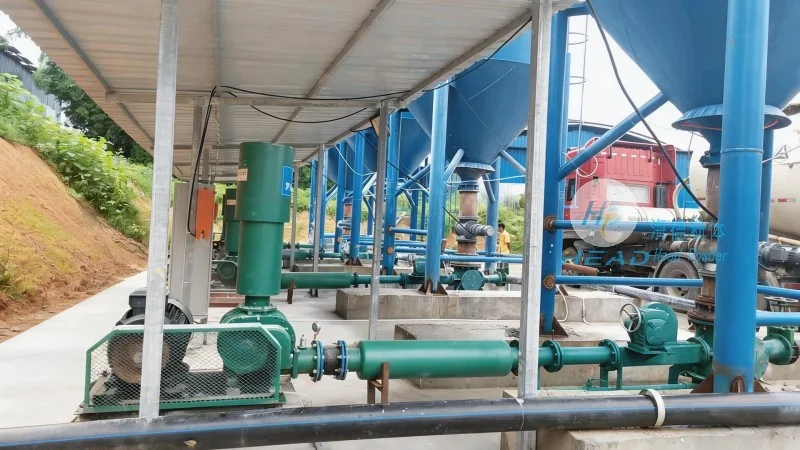
The working principle of the potassium carbonate fertilizer material handling system combines mechanical and pneumatic technologies to achieve efficient material transport. The mechanical components, such as conveyor belts and rotary valves, rely on motor-driven mechanisms to move the material. The conveyor belts use friction to move the bulk material, while the rotary valves use a rotating disc to control the flow. The pneumatic components, such as airlocks and pneumatic conveyors, use compressed air to transport the material through pipelines. The system integrates these technologies to handle the specific characteristics of potassium carbonate fertilizer, which is a fine, free-flowing powder that requires gentle handling to prevent segregation and degradation. The mechanical conveyors are designed with low friction surfaces and smooth idlers to minimize material wear and maintain product quality. The pneumatic conveyors use low-pressure air to transport the material, reducing the risk of material degradation and ensuring a clean, dust-free operation. The combination of mechanical and pneumatic systems allows for flexibility in material handling, enabling the system to adapt to different operational requirements and material characteristics.
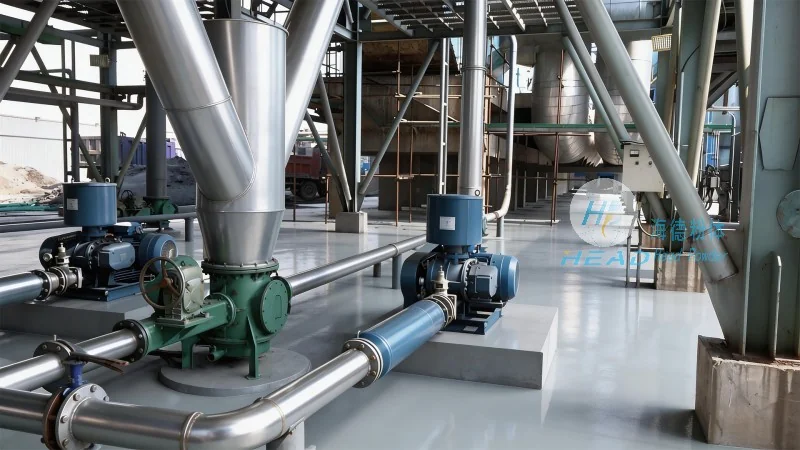
The potassium carbonate fertilizer material handling system developed by Shandong HeadPowder Engineering Co., Ltd. offers several advantages that make it ideal for fertilizer processing and distribution. The system is designed for high efficiency, with a high throughput capacity that can handle large volumes of potassium carbonate fertilizer. The mechanical and pneumatic components are durable and low-maintenance, reducing downtime and operational costs. The system is also equipped with advanced control systems that provide real-time monitoring and data analysis, allowing for optimal performance and predictive maintenance. The technical specifications of the system include a maximum material flow rate of up to 200 tons per hour, a conveying distance of up to 100 meters, and a material handling capacity of up to 50,000 tons per year. The system is also designed to meet international safety and environmental standards, ensuring compliance with regulations and minimizing the risk of accidents or environmental impact.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top