Shandong HeadPowder Engineering Co., Ltd., a leading enterprise in the powder conveying industry, specializes in the design, manufacturing, and application of advanced powder handling systems. This article provides a detailed overview of the operation process and working principle of PFA (Polytetrafluoroethylene-co-hexafluoropropylene) powder conveying systems, which are widely used in various industrial sectors due to their excellent chemical resistance, thermal stability, and non-stick properties. The following sections will explore the key components, operational workflow, and technical mechanisms that enable efficient and reliable PFA powder transport.
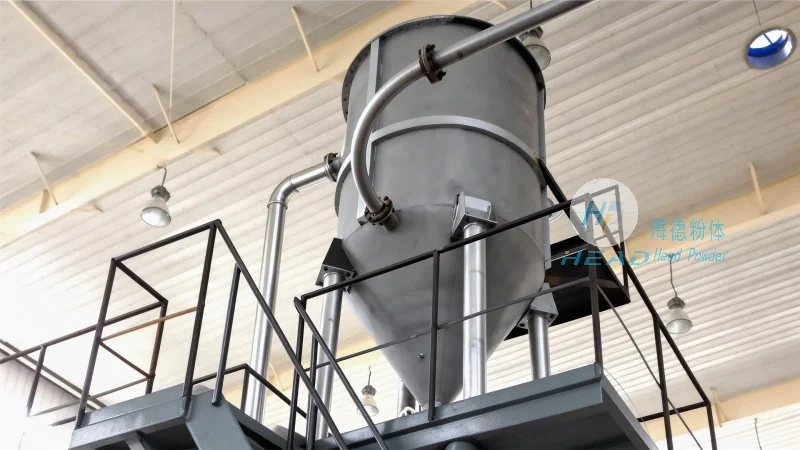
The PFA powder conveying system typically consists of several core components that work in concert to ensure smooth material handling. These components include the material hopper, feeding device, conveying pipeline, control system, and discharge unit. The material hopper is designed to store the PFA powder and maintain a consistent feed rate, often equipped with level sensors to monitor the material inventory. The feeding device, such as a rotary valve or screw feeder, regulates the flow of powder from the hopper into the conveying pipeline. The conveying pipeline, usually made of corrosion-resistant materials like PFA or stainless steel, transports the powder under pressure or vacuum. The control system, which may include PLC (Programmable Logic Controller) and sensors, monitors and adjusts the system parameters to optimize performance. Finally, the discharge unit, such as a rotary valve or bagging machine, releases the PFA powder at the desired location.
The working principle of PFA powder conveying systems is based on the principles of pneumatic or mechanical conveying, depending on the specific design. For pneumatic conveying, the system uses compressed air or vacuum to move the powder through the pipeline. The powder is suspended in the air stream and transported to the discharge point. The pressure or vacuum level is carefully controlled to ensure the powder flows smoothly without clogging or degradation. For mechanical conveying, the system employs rotating components like screws or augers to push the powder through the pipeline. This method is particularly suitable for abrasive or sticky powders, as it minimizes friction and reduces the risk of material degradation. The choice between pneumatic and mechanical conveying depends on factors such as the powder characteristics, system capacity, and operational requirements.
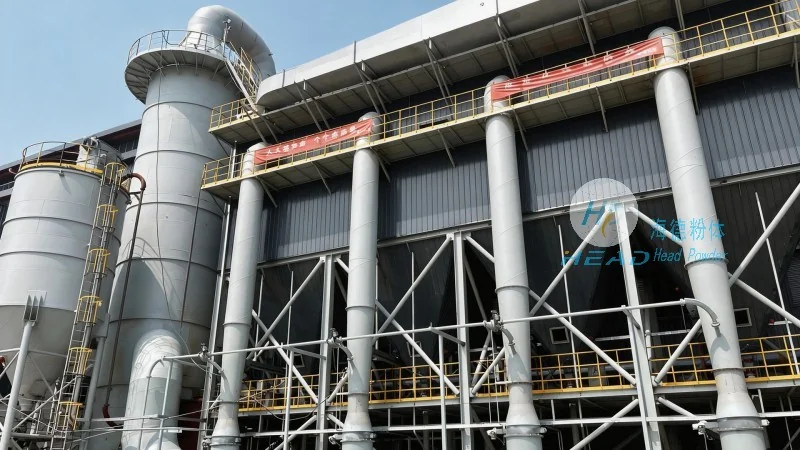
The operation process of a PFA powder conveying system involves several sequential steps to ensure efficient and safe material handling. The first step is the preparation phase, where the system is checked for proper functionality, including the condition of the hopper, feeding device, and pipeline. The material is then loaded into the hopper, and the level sensors are calibrated to monitor the inventory. The second step is the start-up phase, where the control system is activated, and the conveying medium (air or mechanical force) is initiated. The system is then allowed to run for a short period to purge any air or debris from the pipeline. The third step is the normal operation phase, where the powder is conveyed from the hopper to the discharge point at a controlled rate. The control system continuously monitors the flow rate, pressure, and temperature to maintain optimal performance. The fourth step is the shutdown phase, where the system is stopped, and the pipeline is purged to remove any remaining powder. Finally, the system is cleaned and maintained as per the manufacturer's recommendations to ensure long-term reliability.
PFA powder conveying systems offer several advantages that make them ideal for handling PFA powder and other similar materials. Firstly, PFA is highly resistant to chemicals, including acids, bases, and solvents, which ensures the system's longevity and minimal maintenance. Secondly, PFA has excellent thermal stability, allowing the system to operate at high temperatures without degradation. Thirdly, the non-stick properties of PFA prevent powder buildup on the pipeline and equipment, reducing the risk of clogging and improving flow efficiency. Additionally, the systems are designed for low maintenance, with easy-to-clean components and minimal wear parts. These advantages make PFA powder conveying systems a cost-effective and reliable solution for industries such as electronics, pharmaceuticals, and chemical processing.
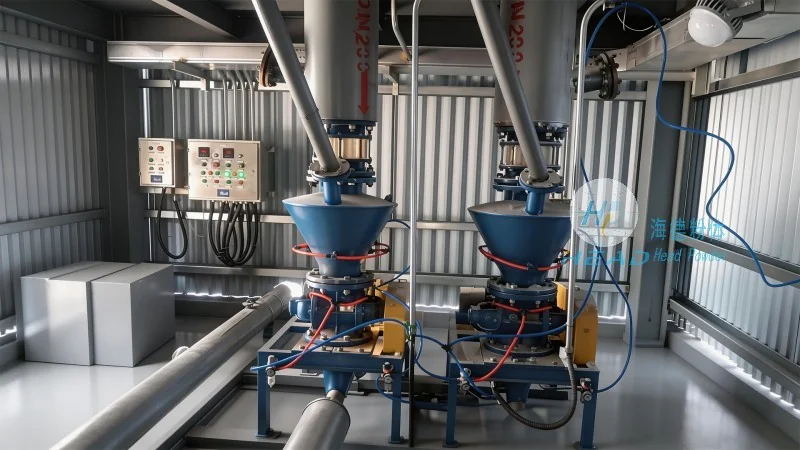
PFA powder conveying systems are widely used in various industrial applications where PFA powder is handled. Some common applications include the manufacturing of PFA tubing, PFA fittings, and PFA coatings. In the electronics industry, PFA is used for insulation and heat resistance in electrical components, and the conveying system ensures efficient transport of the powder to the production lines. In the pharmaceutical industry, PFA is used for medical devices and packaging, and the system maintains the purity and integrity of the powder during transport. In the chemical processing industry, PFA is used as a corrosion-resistant material in reactors and pipelines, and the conveying system ensures safe and efficient handling of the powder. The versatility of PFA powder conveying systems makes them suitable for a wide range of applications, from small-scale laboratory use to large-scale industrial production.
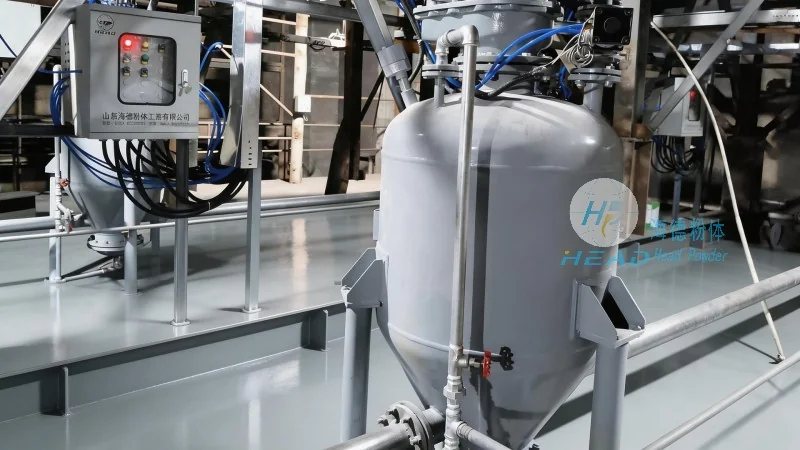
Maintenance and troubleshooting are essential to ensure the long-term performance and reliability of PFA powder conveying systems. Regular maintenance includes cleaning the hopper, feeding device, and pipeline to remove any powder buildup or debris. The components should be inspected for wear and tear, and replaced as needed. The control system and sensors should be calibrated periodically to ensure accurate monitoring and control. Troubleshooting common issues such as clogging, low flow rate, or pressure fluctuations involves checking the material feed rate, pipeline condition, and system pressure. If clogging occurs, the system may need to be purged or the pipeline cleaned. Low flow rate may indicate a blockage or insufficient conveying medium, while pressure fluctuations could be due to a faulty valve or sensor. By following the manufacturer's maintenance guidelines and addressing issues promptly, the system can operate efficiently and reliably for years.
Shandong HeadPowder Engineering Co., Ltd. provides advanced PFA powder conveying systems that are designed to meet the demanding requirements of various industrial applications. The operation process and working principle of these systems involve a combination of advanced engineering and careful design, ensuring efficient and reliable powder transport. With their excellent chemical resistance, thermal stability, and non-stick properties, PFA powder conveying systems offer significant advantages over traditional materials. By understanding the key components, working principles, and operational processes, users can optimize the performance of their PFA powder conveying systems and achieve cost-effective and safe material handling. As a leading provider in the industry, Shandong HeadPowder Engineering Co., Ltd. continues to innovate and improve its products to meet the evolving needs of the market.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top