For agricultural operations dealing with rapeseed, efficient and reliable material handling is crucial. The rapeseed pneumatic conveying machine, a product of Shandong HeadPowder Engineering Co., Ltd., offers a sophisticated solution to transport rapeseed efficiently from one location to another. This equipment is designed to handle the unique characteristics of rapeseed, ensuring minimal damage and optimal flow during the conveying process.
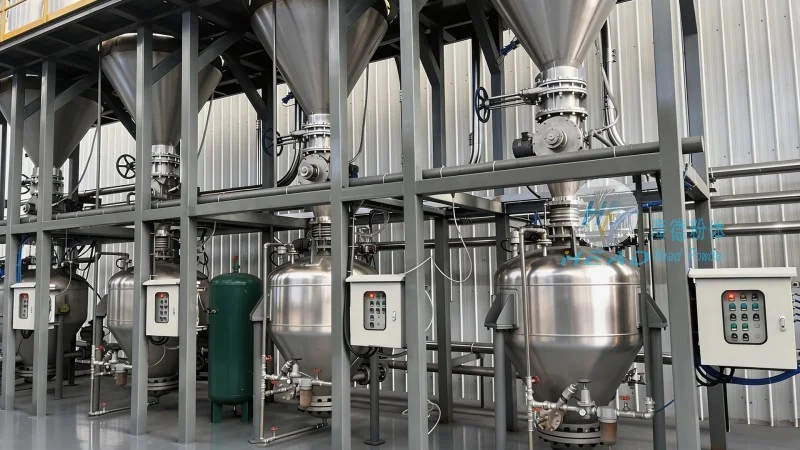
Before delving into the operational details, it's essential to understand the role of pneumatic conveying systems in modern agricultural processing. These machines utilize air pressure to move bulk materials like rapeseed through a pipeline network. The design of the rapeseed pneumatic conveying machine by HeadPowder is tailored to meet the specific demands of rapeseed handling, including its density, moisture content, and potential for breakage during transport.
The rapeseed pneumatic conveying machine consists of several critical components that work in tandem to ensure smooth operation. These include the hopper for material storage, the air compressor that generates the necessary air pressure, the pipeline system for material transport, and the discharge valve for material release. Each component plays a vital role in maintaining the integrity of the rapeseed and the efficiency of the conveying process.
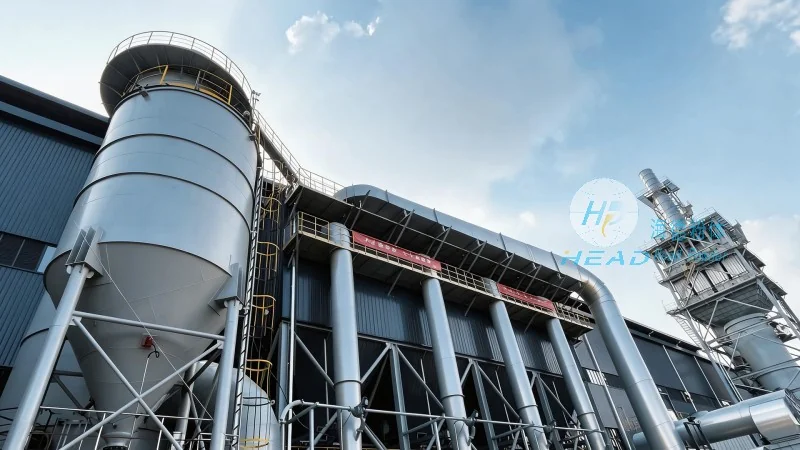
The operation of the rapeseed pneumatic conveying machine begins with the loading of rapeseed into the hopper. As the material is fed into the system, the air compressor starts, creating a pressure differential that draws the rapeseed into the pipeline. The air and material mixture travels through the pipeline, with the air providing the force to move the rapeseed. At the discharge end, the air is separated from the rapeseed, and the material is collected in the receiving container. This process is continuous and can be adjusted to handle varying volumes of rapeseed, making it suitable for both small-scale and large-scale operations.
The working principle of the rapeseed pneumatic conveying machine is based on the principles of fluid dynamics and air pressure. When the air compressor operates, it generates a high-pressure air stream that enters the pipeline. The rapeseed is introduced into the pipeline either by gravity or by a feeder mechanism, and the air stream lifts and transports the material. The velocity of the air and the size of the particles determine the conveying capacity and efficiency of the system. The design of the pipeline and the air velocity are optimized to prevent material deposition and ensure consistent flow.
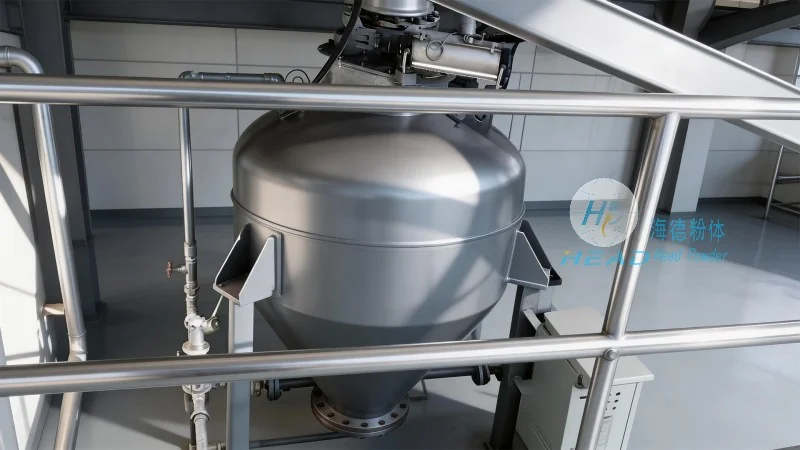
Implementing a rapeseed pneumatic conveying machine offers several advantages over traditional methods like belt conveyors or bucket elevators. These advantages include reduced material handling time, lower labor costs, and minimal product damage. The enclosed system also helps maintain the quality of the rapeseed by protecting it from contamination and moisture. Additionally, the flexibility of the pipeline system allows for easy integration into existing processing lines, making it a versatile solution for various agricultural applications.
The rapeseed pneumatic conveying machine is widely used in rapeseed processing facilities, from seed cleaning and sorting to storage and packaging. The operational considerations include maintaining proper air pressure, ensuring the pipeline is free of blockages, and monitoring the material flow rate. Regular maintenance of the air compressor and other components is essential to keep the system running efficiently and prevent downtime. By adhering to these considerations, users can maximize the lifespan and performance of the rapeseed pneumatic conveying machine.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top