Coal and coke are essential raw materials in various industrial sectors, including steel production, power generation, and chemical manufacturing. The efficient and reliable transportation of these bulk materials is crucial for maintaining smooth operations and optimizing production processes. Pneumatic conveying systems, particularly those designed for coal and coke, offer a versatile and effective solution for handling these materials with precision and minimal downtime. This article delves into the operation process and working principle of coal and coke pneumatic conveying machines, highlighting the key components, operational steps, and technological advancements that make them indispensable in modern material handling.
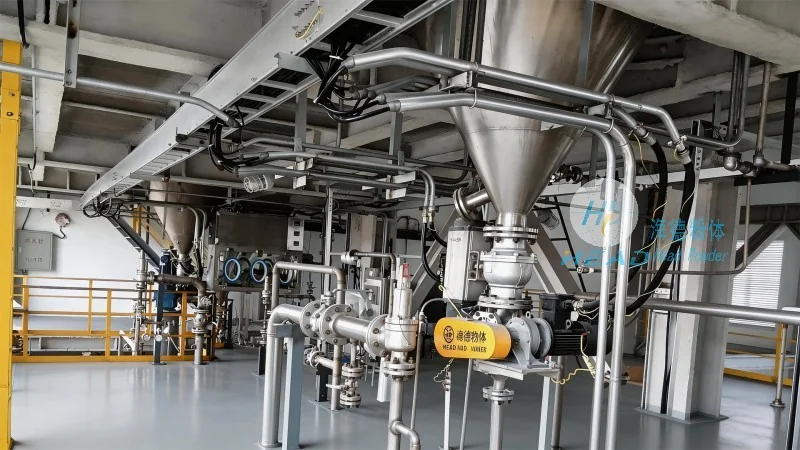
The coal and coke pneumatic conveying machine consists of several critical components that work in harmony to ensure efficient material transport. The primary components include the hopper, which serves as the storage and feeding unit for the bulk material; the air compressor or blower, responsible for generating the necessary airflow to move the material; the conveying line, typically made of flexible or rigid tubing, which carries the material and air mixture; and the discharge unit, where the material is deposited at the destination. Additionally, auxiliary components such as filters, silencers, and pressure regulators are integrated to maintain system efficiency, control air quality, and ensure safe operation. The design of these components is tailored to handle the specific characteristics of coal and coke, such as their particle size, density, and moisture content, ensuring optimal performance and longevity.
The working principle of coal and coke pneumatic conveying machines is based on the use of compressed air to transport bulk materials through a pipeline. The process begins with the material being fed into the hopper, where it is then drawn into the conveying line by the airflow generated by the air compressor. As the air flows through the line, it entrains the material particles, creating a slurry-like mixture that is propelled forward. The velocity of the air and the design of the conveying line determine the efficiency of material transport, with higher air velocities typically resulting in better conveying performance for finer particles. The system operates under either positive pressure (where air is forced into the line) or negative pressure (where air is drawn out of the line), depending on the specific application and material characteristics. In the case of coal and coke, positive pressure systems are commonly used due to their ability to handle larger particle sizes and prevent material degradation during transport.
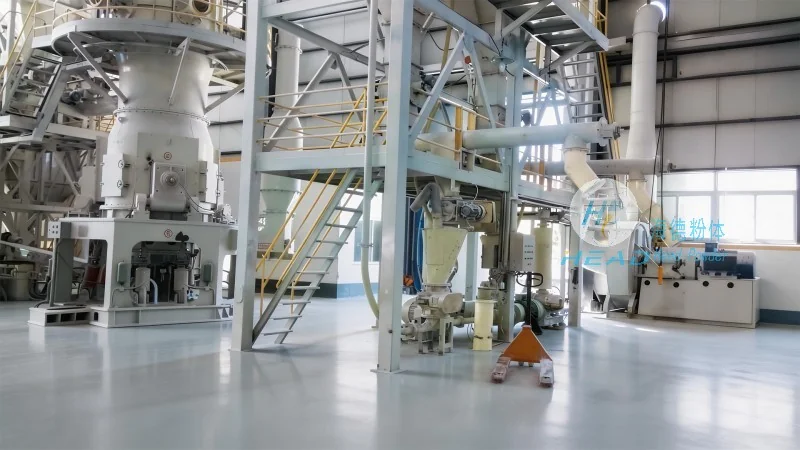
The operation process of a coal and coke pneumatic conveying machine involves several sequential steps that ensure the smooth and continuous transport of materials. The first step is material loading, where coal or coke is fed into the hopper from a storage silo or truck. The hopper is equipped with a feeder, such as a rotary valve or screw conveyor, which regulates the flow rate of the material into the conveying line. The second step is air compression, where the air compressor or blower generates the required airflow, typically at a pressure of 0.5 to 1.5 bar, depending on the system design and material characteristics. The compressed air is then introduced into the conveying line, creating a flow that pulls the material particles into the system. The third step is material transport, where the air and material mixture travels through the pipeline to the discharge point. The pipeline may include bends, elbows, or expansion joints to accommodate changes in direction or elevation, ensuring the material is conveyed without blockages or degradation. The fourth step is material discharge, where the material is deposited at the destination, such as a storage silo, furnace, or processing unit. The system may also include a filter to remove dust and particulate matter from the exhaust air, ensuring compliance with environmental regulations and maintaining air quality. Finally, the system is monitored and controlled by a programmable logic controller (PLC) or other control systems, which adjust the airflow and material feed rate to maintain optimal performance and prevent system overload.
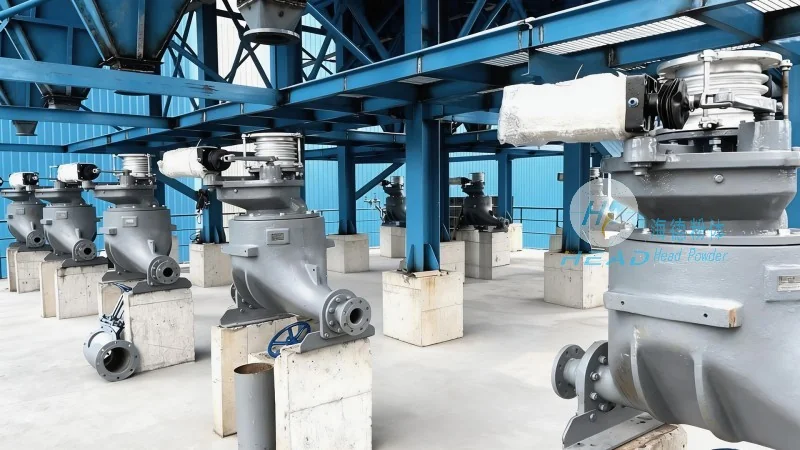
Coal and coke pneumatic conveying machines offer several advantages over traditional material handling methods, such as belt conveyors or bucket elevators. One of the primary advantages is the ability to transport materials over long distances with minimal maintenance and downtime. The system is also highly flexible, as it can be easily reconfigured to accommodate changes in production requirements or facility layout. Additionally, pneumatic conveying systems are less prone to material degradation, as the material is enclosed in the pipeline and protected from external factors such as moisture, dust, or temperature fluctuations. The system also provides better control over material flow, as the airflow and feed rate can be precisely adjusted to match the production needs. Furthermore, the use of compressed air allows for the transport of materials in a closed system, reducing the risk of dust emissions and improving workplace safety. These advantages make coal and coke pneumatic conveying machines an ideal solution for industries that require efficient, reliable, and safe material handling.
Coal and coke pneumatic conveying machines are widely used in various industrial applications, particularly in the steel and power generation industries. In steel production, these systems are used to transport coal and coke from storage silos to blast furnaces or coke ovens, ensuring a steady supply of raw materials for the production process. In power generation, the systems are used to convey coal from storage facilities to boilers, where it is burned to generate electricity. Additionally, the systems are used in chemical and petrochemical industries to transport coke and other bulk materials to processing units. The versatility of coal and coke pneumatic conveying machines makes them suitable for a wide range of applications, from small-scale operations to large industrial plants. The systems can be customized to meet the specific requirements of each application, including the material type, conveying distance, and production capacity.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top