Long-distance pneumatic conveying systems are advanced industrial solutions designed to transport bulk materials over extended distances with efficiency and reliability. These systems are widely used in various industries, including food processing, pharmaceuticals, chemicals, and mining, due to their ability to handle a wide range of materials while maintaining product integrity. The technology behind these systems combines air flow and mechanical components to move materials from a source to a destination, often without the need for direct contact between the material and the conveying equipment.
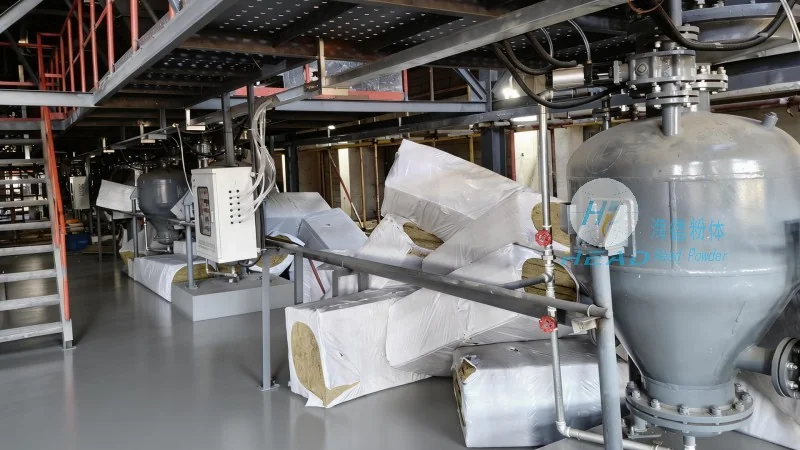
Headpowder, the professional manufacturer of pneumatic conveying systems, is headquartered in Shandong, China. As a leading company in the field, Headpowder specializes in designing, manufacturing, and supplying high-quality long-distance pneumatic conveying solutions tailored to meet the diverse needs of global clients. With years of experience and a commitment to innovation, Headpowder has established itself as a trusted partner for industries seeking efficient material handling solutions.
Long-distance pneumatic conveying systems typically consist of several critical components that work in tandem to ensure smooth material transport. These components include a material feeder, a conveying line (often equipped with pressure vessels or ducts), a control system, and a discharge unit. The material feeder is responsible for introducing the bulk material into the system, while the conveying line uses compressed air to propel the material through the ducts. The control system monitors and regulates the air pressure, flow rate, and material feed rate to maintain optimal operation. Finally, the discharge unit collects the material at the destination, ensuring a clean and efficient transfer process.
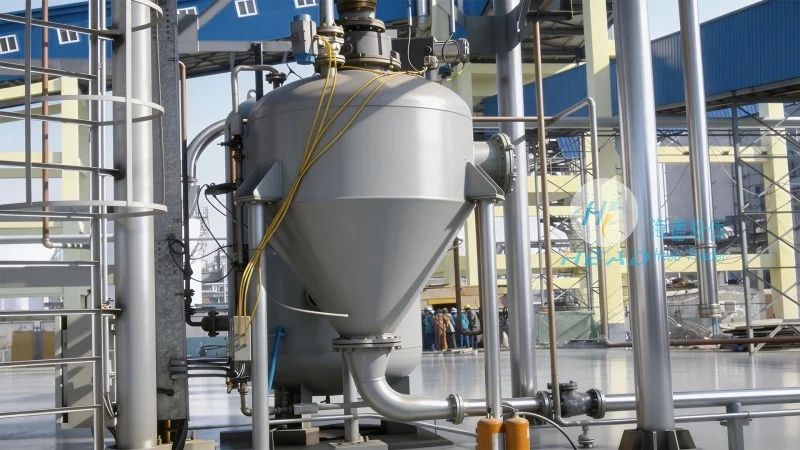
The operation process of a long-distance pneumatic conveying system involves several sequential steps that ensure the material is transported safely and efficiently. First, the bulk material is fed into the system through the material feeder. The feeder may use a hopper or a screw feeder to regulate the flow rate, preventing overloading or underfeeding. Next, compressed air is introduced into the conveying line, creating a pressure differential that propels the material forward. The air flow rate is carefully controlled to match the material's characteristics, such as particle size, density, and moisture content. As the material travels through the ducts, it is suspended in the air stream and moves towards the discharge point. The system may include intermediate vessels or expansion chambers to reduce pressure and allow for material settling, if necessary. Finally, the material is discharged at the destination, where it is collected in a storage bin or processing unit. The entire process is automated and monitored by the control system, ensuring consistent performance and minimal downtime.
The working principle of long-distance pneumatic conveying systems is based on the fundamental concept of fluidization and air flow. When compressed air is introduced into the conveying line, it creates a low-pressure environment that draws the material into the air stream. The air flow rate is adjusted to maintain a stable suspension of the material particles, preventing clogging or blockages in the ducts. The system can operate in either positive pressure or negative pressure modes, depending on the application and material characteristics. In positive pressure systems, air is forced through the conveying line, pushing the material forward. In negative pressure systems, air is drawn out of the system, creating a vacuum that pulls the material into the ducts. Both modes are effective, but the choice depends on factors such as material sensitivity, distance, and environmental considerations. The efficiency of the system is influenced by the air velocity, duct diameter, and material properties, all of which are optimized during the design phase to ensure maximum performance.
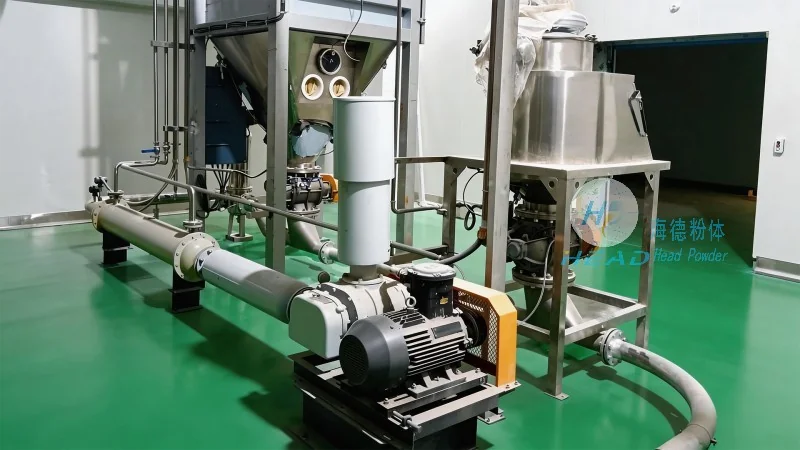
Long-distance pneumatic conveying systems offer numerous advantages over traditional material handling methods, such as belt conveyors or bucket elevators. One of the primary benefits is the ability to transport materials over long distances without the need for intermediate transfer points, reducing the risk of material contamination and loss. The systems are also highly flexible, allowing for changes in material flow direction or destination without significant modifications. Additionally, pneumatic conveying systems are capable of handling a wide range of materials, including powders, granules, and even wet or sticky substances, with minimal degradation. The enclosed design of the system also helps maintain product quality and hygiene, which is crucial in industries like food and pharmaceuticals. Furthermore, these systems are energy-efficient and can be integrated with existing infrastructure, making them a cost-effective solution for material handling needs.
Long-distance pneumatic conveying systems are widely used in various industries due to their versatility and efficiency. In the food industry, these systems are used to transport ingredients such as flour, sugar, and spices from storage to processing lines, ensuring a clean and hygienic transfer process. In the pharmaceutical industry, pneumatic conveying is employed to handle active pharmaceutical ingredients (APIs) and other sensitive materials, maintaining strict contamination control. The chemical industry utilizes these systems to transport powders and granules, such as catalysts and reagents, in manufacturing processes. Mining and mineral processing industries also benefit from long-distance pneumatic conveying systems, which are used to transport ore and other bulk materials from mines to processing facilities. Additionally, the system is applied in the agricultural sector for handling grains and other agricultural products, improving storage and transportation efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top