Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial material handling solutions based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems for the efficient transport of cement fly ash and mineral powders. These systems are integral to modern production processes, enabling reliable and low-maintenance material handling for various applications in the cement, mining, and chemical industries.
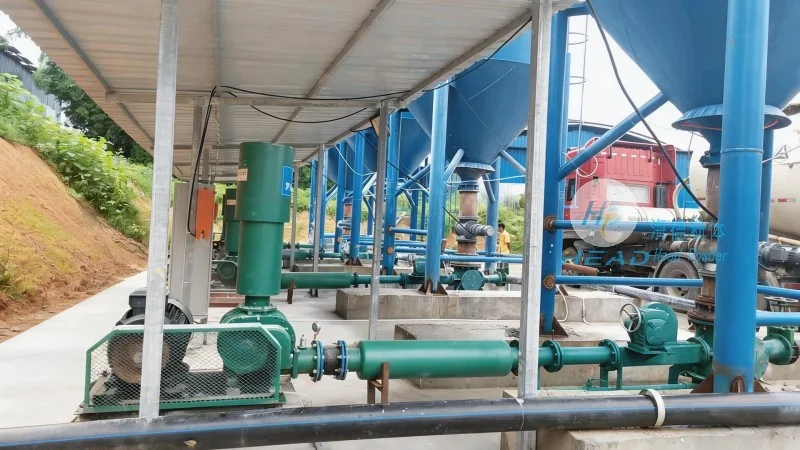
The pneumatic conveying system for cement fly ash and mineral powders typically comprises several critical components that work in unison to achieve efficient material transport. These components include a material hopper or feeder, a conveying pipeline, a high-pressure blower or air compressor, a control panel with monitoring and adjustment features, and a discharge unit or silo. Each component is engineered to address the unique challenges of handling fine powders like cement fly ash, which are prone to caking, agglomeration, or dust generation if not managed properly.
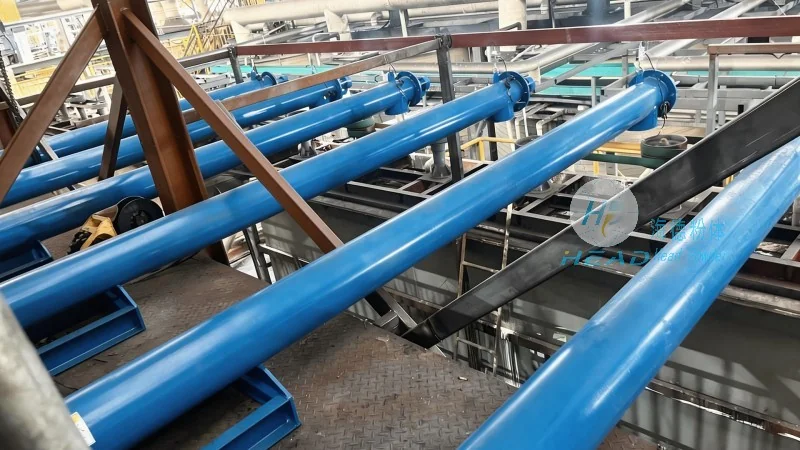
The fundamental working principle of pneumatic conveying for cement fly ash and mineral powders is based on the use of compressed air to create a flow that suspends and transports the solid particles through a closed pipeline. When the blower operates, it generates high-pressure air that enters the pipeline, establishing a pressure differential between the inlet and outlet. This pressure difference draws the material from the hopper into the pipeline, where it is suspended by the air stream. The air velocity is carefully controlled to maintain the material in a suspended state, preventing blockages and ensuring smooth transport. The system can operate in either positive pressure (where the pipeline is pressurized above ambient air pressure) or negative pressure (where the pipeline is slightly vacuumed), with positive pressure being more common for long-distance transport due to its ability to handle larger volumes and longer pipelines.
The operation of a pneumatic conveying system for cement fly ash and mineral powders follows a systematic sequence of steps. Initially, the material is fed into the hopper from the storage silo or production line. The feeder, often equipped with a rotary valve or screw conveyor, regulates the flow rate to ensure a consistent supply of material to the system. Once the feeder is activated, the control system initiates the blower, which starts generating the required air pressure. The control panel continuously monitors parameters such as pressure, flow rate, and material level, adjusting the blower speed or feeder rate as needed to maintain optimal operation. As the air flows through the pipeline, it carries the cement fly ash and mineral powders from the hopper to the discharge point, which may be a processing unit, a storage silo, or another destination. The system continues to operate until the material supply is exhausted or the process is manually stopped. Regular maintenance, including cleaning the hopper, checking for blockages, and inspecting the blower and pipeline, is essential to ensure the system remains efficient and free from operational issues.
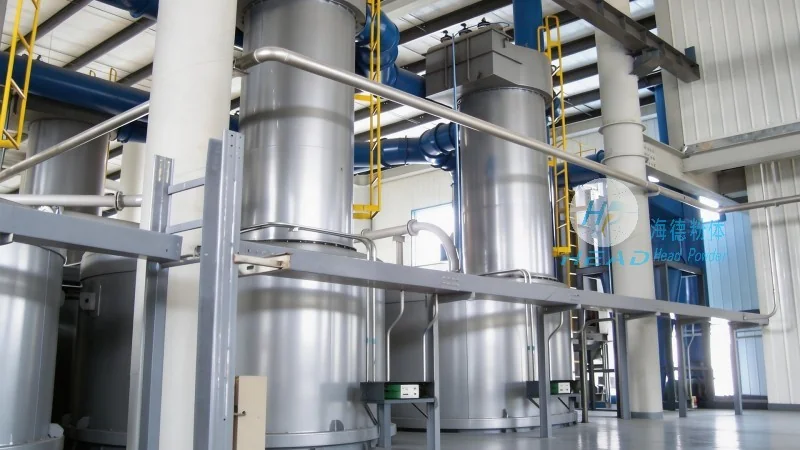
Pneumatic conveying systems offer significant advantages when handling cement fly ash and mineral powders, making them a preferred choice in many industrial applications. One of the key benefits is high transport efficiency, as the system can move large volumes of material over long distances with minimal energy consumption compared to traditional methods like belt conveyors or bucket elevators. The enclosed pipeline design effectively prevents dust contamination, protecting the environment and maintaining a clean working environment. Additionally, the system is flexible and can be easily integrated into existing production lines with minimal modifications, allowing for seamless integration with other processing equipment. The low maintenance requirements and long service life of the components, such as the blower and pipeline, contribute to cost savings and operational reliability over time. Furthermore, the system can handle a wide range of particle sizes and moisture contents, making it suitable for various applications in the cement, mining, and chemical industries.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top