HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of air-powered conveyor systems tailored for small stone material handling. This article explores the fundamental principles behind these systems and highlights the key working scene characteristics that make them an efficient solution for various industrial applications.
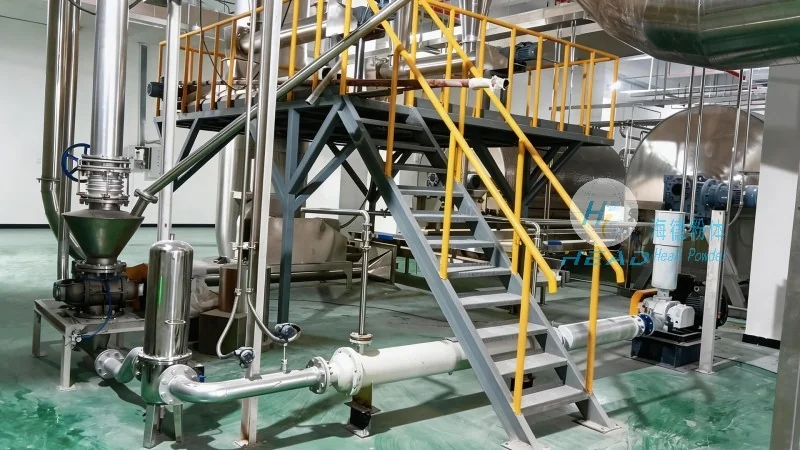
HeadPowder is a professional engineering company dedicated to providing high-quality material handling solutions. With a strong focus on innovation and customer satisfaction, the company has established itself as a trusted name in the industry. Headquartered in Shandong, China, HeadPowder leverages advanced technology and extensive experience to develop reliable air-powered conveyor systems for diverse material processing needs.
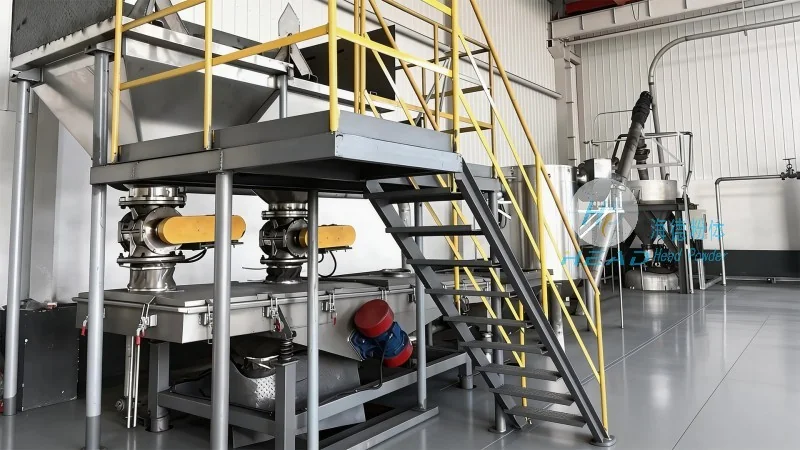
The air-powered conveyor, also known as a pneumatic conveyor, operates by using compressed air to transport small stone materials through a pipeline system. The core principle involves creating a pressure differential between the inlet and outlet of the conveyor, which propels the material along the pipeline. This method eliminates the need for mechanical components like belts or rollers, reducing maintenance requirements and enhancing operational efficiency. The system typically consists of a hopper for material loading, a compressor to generate compressed air, and a pipeline network that guides the material from the source to the destination. The design is flexible, allowing for vertical, horizontal, or inclined transport, making it suitable for various spatial configurations in industrial settings.
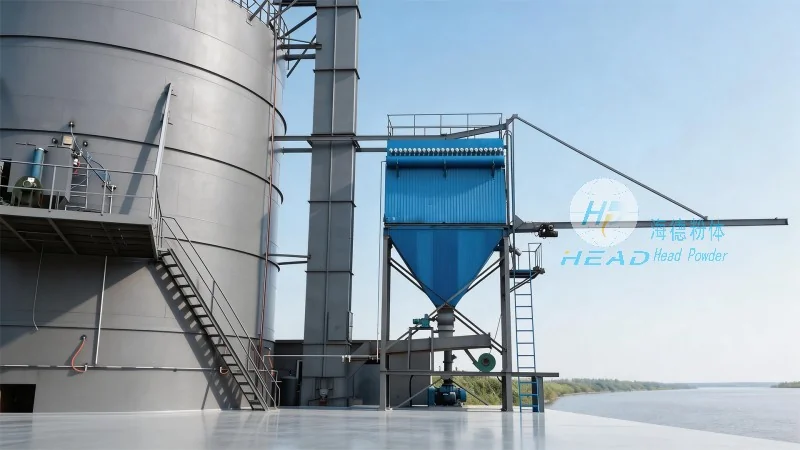
The effectiveness of air-powered conveyors for small stone materials is influenced by several working scene characteristics that optimize their performance. First, the material size and density play a crucial role. Small stones with uniform dimensions and moderate density are ideal for pneumatic transport, as they can be easily suspended and moved by the air flow. The conveyor's capacity is directly related to the material's bulk density and the system's air pressure, which must be carefully matched to ensure consistent material flow without blockages. Second, the layout of the working environment is a critical factor. The system's flexibility allows for integration into existing production lines or new setups, with the ability to navigate around obstacles and adapt to different spatial constraints. This adaptability is particularly valuable in facilities where space is limited or where the workflow requires multiple transport routes. Third, the environmental conditions within the working scene also impact the conveyor's performance. Pneumatic conveyors are generally well-suited for indoor applications, as they can be enclosed to control dust and maintain a clean working environment. However, they may require additional filtration systems if outdoor or dusty conditions are present, ensuring compliance with industrial safety and hygiene standards. Finally, the operational efficiency of the system is enhanced by the ability to control the air flow and pressure dynamically. This allows for precise regulation of material transport speed, which is essential for maintaining consistent production rates and preventing material degradation or breakage during transit.
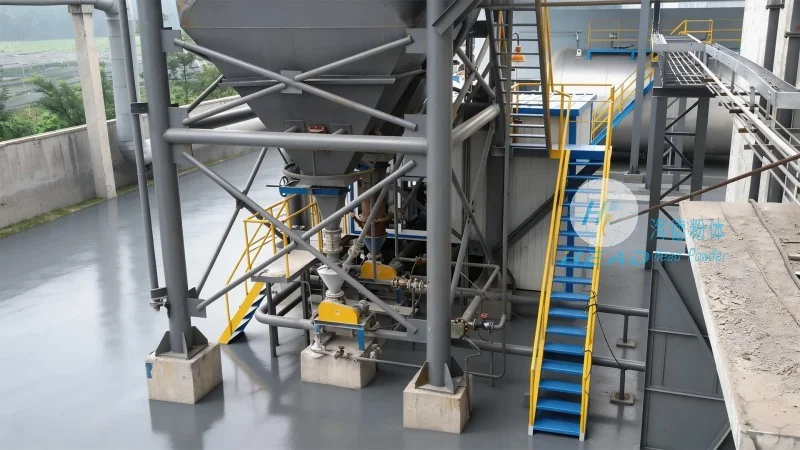
Air-powered conveyors for small stone materials find widespread application in various industrial sectors, including mining, construction, and manufacturing. In mining operations, these systems are used to transport crushed stone from processing plants to storage areas or for further processing, improving material handling efficiency and reducing manual labor. In construction sites, they facilitate the movement of aggregates and small stones from stockpiles to mixing plants or other work areas, streamlining the construction process and enhancing productivity. In manufacturing facilities, they are employed to transport raw materials or finished products with small stone components, such as in the production of concrete or other building materials. The primary benefits of using air-powered conveyors in these applications include increased operational efficiency, reduced labor costs, and improved safety by minimizing the need for manual handling of heavy or dusty materials. Additionally, the system's ability to operate in a closed environment helps maintain a clean and safe working atmosphere, which is crucial for compliance with occupational health and safety regulations. The low maintenance requirements and long service life of pneumatic conveyors further contribute to their cost-effectiveness, making them a preferred choice for industries seeking reliable and efficient material handling solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top