Wheat starch material pneumatic conveying lines represent a sophisticated industrial solution for transporting powders like wheat starch efficiently and hygienically. These systems are integral to modern processing facilities, particularly in the food and chemical sectors, where maintaining product purity and operational efficiency is paramount. The technology operates by using air or gas to move material through a pipeline network, offering advantages over traditional mechanical conveying methods such as reduced contamination risk, lower maintenance requirements, and the ability to handle materials over extended distances. This article delves into the fundamental principles governing these systems and examines the key working scene characteristics that define their application across various industrial environments.
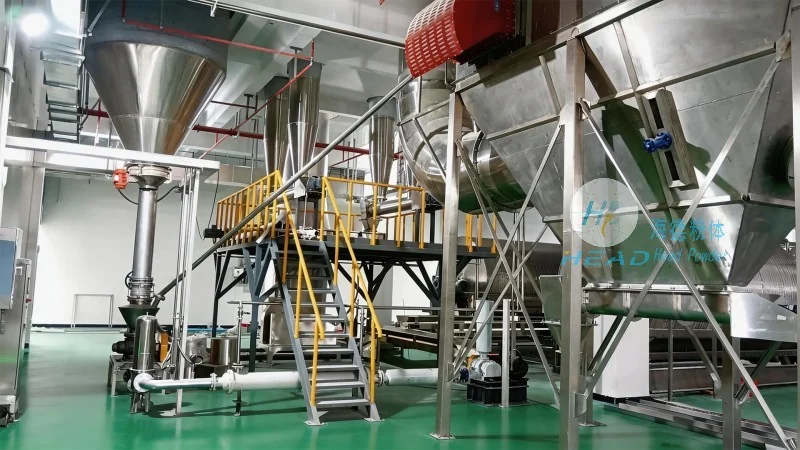
The fundamental principle of pneumatic conveying for wheat starch involves creating a controlled flow of air or gas that draws the material into a pipeline. The system typically comprises several key components: a material hopper for storage and feeding, a blower or compressor to generate the necessary air pressure, a pipeline network with appropriate fittings, and a discharge mechanism to separate the material from the air stream. The process begins when wheat starch is introduced into the hopper. The blower then produces a high-pressure air stream that pulls the material into the pipeline. As the air and material mixture travels through the pipeline, the velocity and pressure are carefully managed to ensure stable and efficient transport. The design of the pipeline, including its diameter, length, and the type of air flow (positive or negative pressure), directly impacts the system's conveying capacity and performance. For wheat starch, which is a fine powder, the system must be engineered to prevent material bridging, ensure consistent flow, and maintain product integrity throughout the transport process.
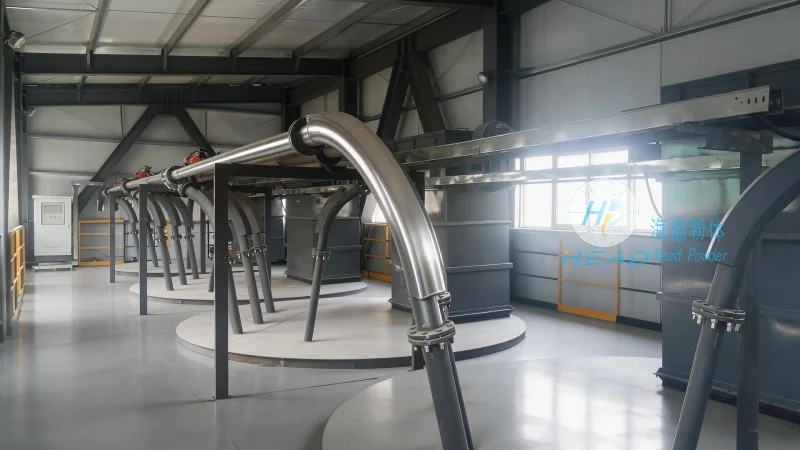
Wheat starch pneumatic conveying lines are deployed in diverse industrial settings, each with unique characteristics that influence system design and operational parameters. In food processing facilities, the systems must adhere to stringent hygiene standards, often requiring stainless steel construction, easy-to-clean components, and minimal contact surfaces to prevent contamination. The conveying process must also minimize product degradation, which is achieved through controlled air velocities and temperature management to avoid overheating or moisture loss. In contrast, in chemical processing plants, the systems may handle more abrasive or corrosive materials, necessitating robust materials of construction and specialized filtration to prevent equipment wear and contamination. The scale of the operation also plays a critical role; large-scale production lines may utilize multiple conveying lines or a network of pipelines to handle high material throughput, while smaller applications might employ single-line systems for localized material transport. Additionally, the system's flexibility in adapting to varying material properties, such as moisture content or particle size, is a key characteristic that enhances its suitability for different working environments.
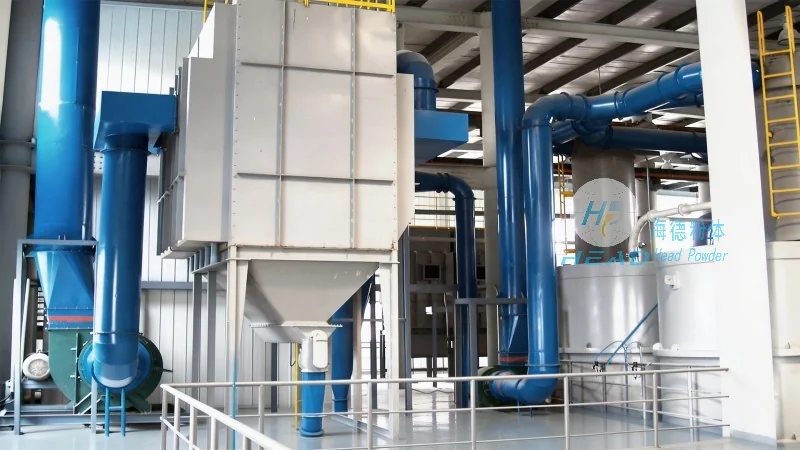
Real-world applications of wheat starch pneumatic conveying lines are widespread across industries. In the food industry, these systems are commonly used for transporting starch from storage silos to processing equipment, such as milling or blending machines. The ability to convey materials without direct mechanical contact reduces the risk of contamination and ensures product purity, which is essential for food-grade applications. In the chemical industry, similar systems are employed for transporting starch-based additives or fillers in pharmaceutical manufacturing. The operational benefits of pneumatic conveying extend beyond hygiene and contamination control; they also include reduced labor costs, as the system automates the material handling process, and increased production efficiency due to continuous, uninterrupted operation. Furthermore, the flexibility of pneumatic systems allows for easy integration with existing production lines, enabling manufacturers to adapt to changing production demands without significant infrastructure modifications. This adaptability makes them a preferred choice for industries where production volumes or product specifications may vary over time.
The effectiveness of a wheat starch pneumatic conveying line depends on the proper selection and integration of key components. The hopper, where the material is stored and fed into the system, must be designed to prevent material bridging and ensure consistent flow. The blower or compressor is the heart of the system, providing the necessary air pressure and volume to move the material. The pipeline network, including elbows, tees, and bends, must be carefully engineered to minimize pressure losses and maintain the air-material mixture's velocity. The discharge point, such as a cyclone separator or a rotary valve, is critical for separating the material from the air stream and directing it to the next processing stage. Design considerations also include the material of construction, which must be compatible with the wheat starch and any additives, and the system's ability to handle variations in material moisture content or particle size. Proper maintenance and monitoring of these components are essential to ensure long-term system reliability and performance. For example, regular cleaning of the hopper and pipeline can prevent material buildup, while monitoring air pressure and flow rates helps identify potential issues before they impact system efficiency.
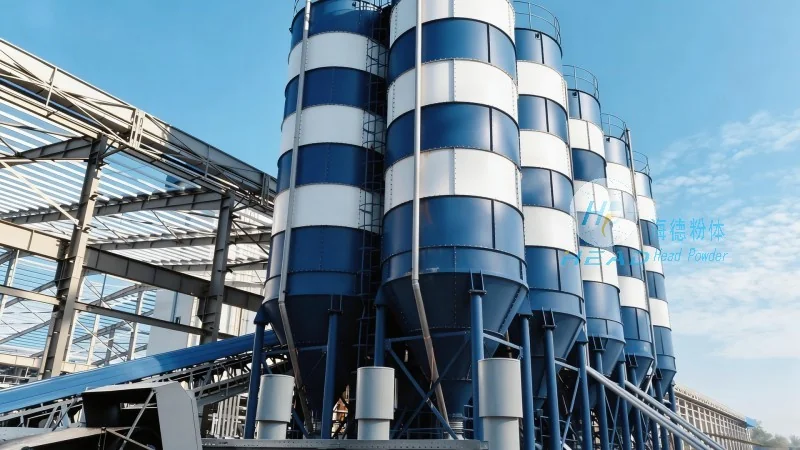
Wheat starch material pneumatic conveying lines represent a highly effective and hygienic solution for material handling in various industrial applications. By leveraging the principles of pneumatic transport, these systems offer significant advantages over traditional methods, including improved product quality, reduced operational costs, and enhanced flexibility. The working scene characteristics of these systems are tailored to meet the specific needs of different industries, ensuring optimal performance and compliance with industry standards. As the demand for efficient and clean material handling solutions continues to grow, the importance of well-designed pneumatic conveying lines in the wheat starch processing industry will only increase. For businesses seeking to optimize their material handling processes, understanding the principles and characteristics of these systems is crucial for making informed decisions and achieving operational excellence. The technology's adaptability and reliability make it a cornerstone of modern industrial processing, supporting the production of high-quality wheat starch products for diverse applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top