For industries dealing with powder electrolytes, efficient and reliable material handling is crucial. A specialized piece of equipment known as a powder electrolyte bulk material conveyor plays a vital role in this process. This article explores the purpose and design principles of such conveyors, providing insights into how they enhance operational efficiency in material transport.
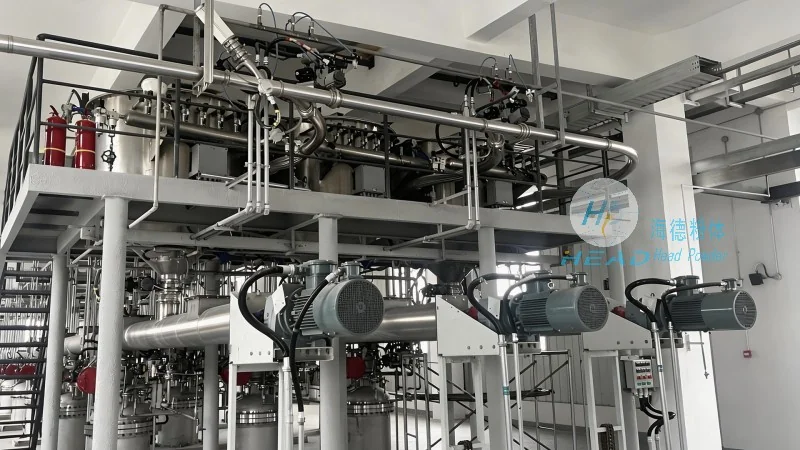
Powder electrolytes are widely used in various applications, including battery manufacturing, chemical processing, and energy storage systems. These materials require precise handling to maintain their integrity and prevent contamination. A bulk material conveyor designed specifically for powder electrolytes addresses these challenges by offering a controlled and consistent method of material transport. The primary function of such a conveyor is to move large quantities of powder electrolyte from one location to another within a production facility, ensuring minimal loss and optimal flow characteristics.
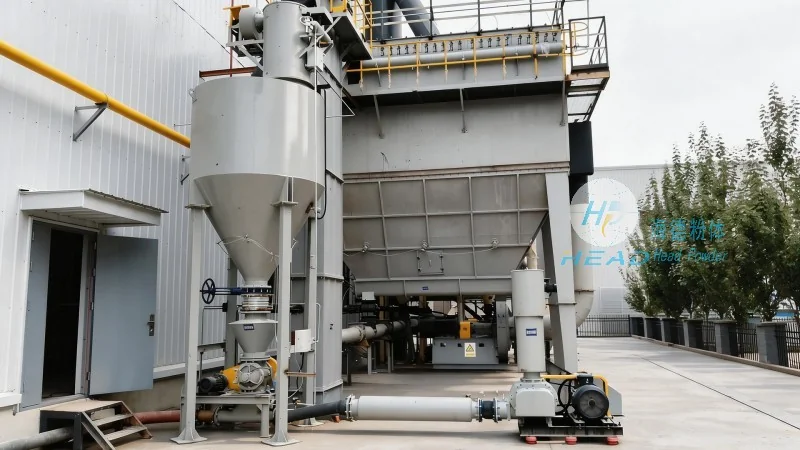
The design of a powder electrolyte bulk material conveyor is tailored to meet the unique properties of these materials. Several key principles guide the development and operation of these systems. First, the conveyor must be constructed from materials that are compatible with the powder electrolyte, preventing chemical reactions or contamination. Common materials include stainless steel, PTFE-coated components, and specialized coatings that resist corrosion and wear. Second, the design incorporates features to minimize particle degradation and agglomeration. This includes gentle handling mechanisms, such as low-speed augers or pneumatic systems, which reduce the risk of particle breakage or clumping. Third, the conveyor is engineered for efficient air management. Proper ventilation and dust control systems are essential to maintain a clean environment and prevent dust accumulation, which can affect both safety and material quality. Fourth, the system is designed for easy maintenance and cleaning. This is critical for industries where product purity is paramount, as any residue can compromise the quality of the powder electrolyte.
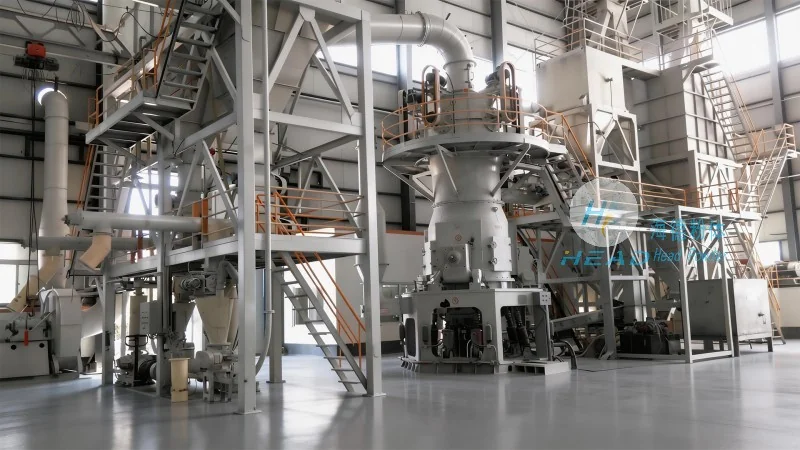
At the core of a powder electrolyte bulk material conveyor are several key components that work together to ensure smooth operation. The primary components include a hopper for material storage, a conveyor mechanism (such as an auger or screw conveyor), and a discharge system. The hopper is typically designed with a sloped bottom to facilitate material flow and prevent clogging. The conveyor mechanism, often an auger, rotates slowly to move the powder electrolyte through the system. This gentle movement minimizes particle damage and ensures consistent flow rates. The discharge system is designed to deliver the material to the next stage of processing, such as a mixer or storage tank. Additionally, many conveyors include a dust collection system to capture and filter any airborne particles, ensuring a safe and clean working environment.
Powder electrolyte bulk material conveyors are widely used across various industries. In battery manufacturing, they are essential for transporting electrolyte powders to production lines, ensuring consistent quality and reducing downtime. In chemical processing, these conveyors help maintain precise material ratios and prevent contamination during batch processing. The benefits of using such conveyors extend beyond efficiency; they also contribute to improved safety by reducing manual handling of powders and minimizing dust exposure. Furthermore, the controlled flow of material helps maintain product consistency, which is critical for meeting quality standards and customer expectations.
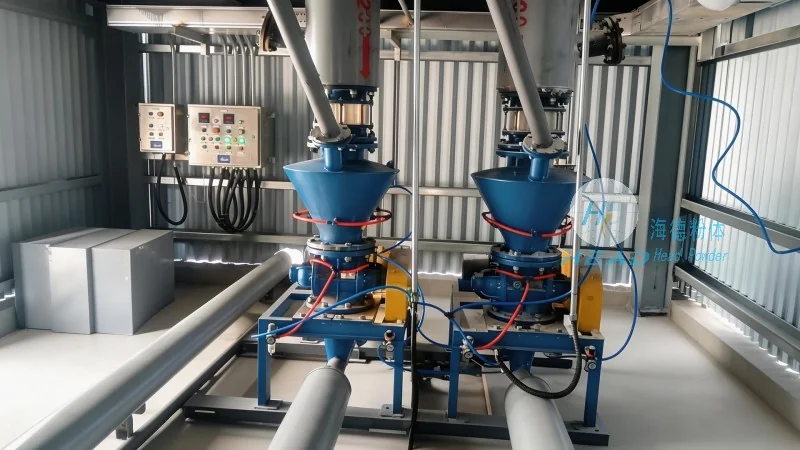
HeadPowder, a leading manufacturer in the field of material handling equipment, specializes in designing and producing high-quality powder electrolyte bulk material conveyors. With years of experience and a commitment to innovation, the company has established itself as a trusted partner for industries requiring reliable and efficient material transport solutions. HeadPowder's products are engineered to meet the specific needs of powder electrolyte applications, incorporating advanced design principles and durable materials to ensure long-term performance. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility equipped with cutting-edge technology and skilled professionals. HeadPowder's dedication to quality and customer satisfaction has earned it a reputation for excellence in the industry, making it a preferred choice for businesses seeking top-tier material handling solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top