Principle and Working Scene Characteristics of Rare Earth Powder Material Pneumatic Conveying Equipm
Release time:2026-09-20 00:01:35
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Manager Zhang
For industrial applications involving rare earth powder handling, efficient and reliable material transport is crucial. The pneumatic conveying equipment designed by Shandong HeadPowder Engineering Co., Ltd. offers a sophisticated solution that addresses the unique challenges associated with transporting fine, abrasive, and valuable rare earth powders. This equipment is engineered to ensure minimal product degradation, maintain high transfer efficiency, and provide a safe operational environment.
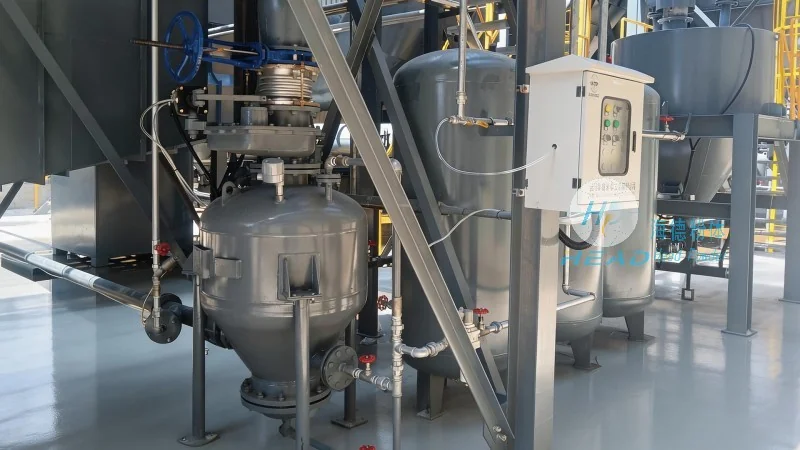
Principle of Pneumatic Conveying for Rare Earth Powders
The core principle of the pneumatic conveying system is the use of compressed air to move powder particles through a pipeline. In the case of rare earth powder handling, the system typically employs a positive displacement or pressure-assisted design to overcome the high friction and particle-to-particle interactions that can cause agglomeration or degradation. The equipment utilizes a combination of air flow control, material feed mechanisms, and pipeline design to achieve consistent and controlled transport. The process begins with the rare earth powder being fed into the system, often through a hopper or feeder, which then introduces the material into the conveying line. Compressed air is then introduced, creating a flow that propels the powder particles forward. The velocity and pressure of the air are carefully managed to ensure that the powder moves without excessive turbulence or separation, which could lead to loss or contamination.
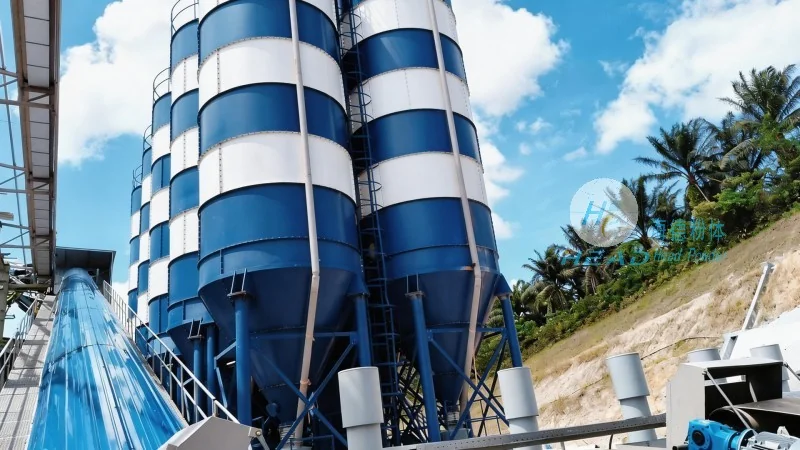
Key Working Scene Characteristics
The working scene characteristics of the rare earth powder pneumatic conveying equipment are tailored to meet the specific demands of industrial processes. These characteristics include:
- High Transfer Efficiency: The system is designed to achieve high material transfer rates with minimal loss, ensuring that the rare earth powder reaches its destination with minimal degradation. This is critical for maintaining the purity and quality of the material, which is essential for downstream applications.
- Low Product Degradation: The equipment minimizes mechanical stress on the powder particles, reducing the risk of attrition and agglomeration. This is achieved through smooth pipeline surfaces, appropriate air flow velocities, and controlled acceleration and deceleration of the material.
- Flexible and Scalable Design: The system can be configured to handle various flow rates and material types, making it adaptable to different production scales and process requirements. This flexibility allows for integration into existing industrial setups or as a standalone solution for new projects.
- Safe and Clean Operation: The pneumatic conveying process is enclosed, preventing dust emissions and ensuring a clean working environment. This is particularly important for rare earth powders, which can be hazardous if inhaled or if they contaminate other materials. The system also incorporates safety features such as pressure relief valves and material flow monitors to prevent overloading or blockages.
- Energy Efficiency: Modern pneumatic conveying systems are optimized for energy consumption, using efficient air compressors and flow control mechanisms to minimize operational costs. This makes the equipment not only effective but also cost-effective for long-term use.
Application Scenarios
The rare earth powder pneumatic conveying equipment is widely used in various industrial sectors where rare earth materials are processed. Common application scenarios include:
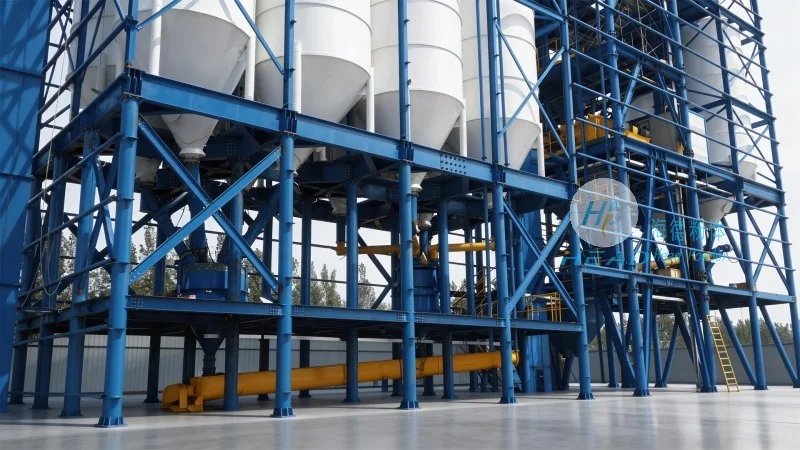
- Mineral Processing Plants: In rare earth ore processing facilities, the equipment is used to transport crushed and milled rare earth concentrates from grinding mills to flotation or separation units. This ensures a continuous flow of material and maintains the integrity of the ore.
- Chemical and Metallurgical Industries: The system is employed in chemical plants that process rare earth oxides or salts, where the powder needs to be transferred from reactors to storage tanks or processing equipment. The equipment's ability to handle abrasive and corrosive materials makes it suitable for these harsh environments.
- Electronics and Manufacturing: In the production of electronic components and magnets, rare earth powders are used as raw materials. The pneumatic conveying equipment efficiently delivers these powders to mixing and sintering equipment, ensuring consistent quality in the final products.
- Research and Development Labs: For laboratory-scale processing of rare earth powders, the equipment provides a precise and controlled method for material transfer, allowing researchers to conduct experiments with minimal variability.
Conclusion
Shandong HeadPowder Engineering Co., Ltd. provides advanced pneumatic conveying solutions for rare earth powder handling, combining technical expertise with practical design to meet the demands of modern industrial applications. The equipment's principles and working characteristics ensure efficient, safe, and reliable transport of rare earth materials, supporting the production processes in various industries. With a focus on minimizing product degradation and maximizing transfer efficiency, this equipment is a critical component in the supply chain of rare earth materials, enabling manufacturers to maintain high-quality standards and operational productivity.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China
