Automatic bulk bag unloading powder pneumatic conveying equipment represents a sophisticated solution for the efficient handling and transportation of bulk powders in industrial settings. This technology integrates advanced automation and pneumatic systems to streamline the process of material transfer, from the initial unloading of bulk bags to the final delivery of powders to processing equipment. The equipment is designed to enhance operational efficiency, reduce labor costs, and improve safety by minimizing direct human contact with potentially hazardous or heavy materials.
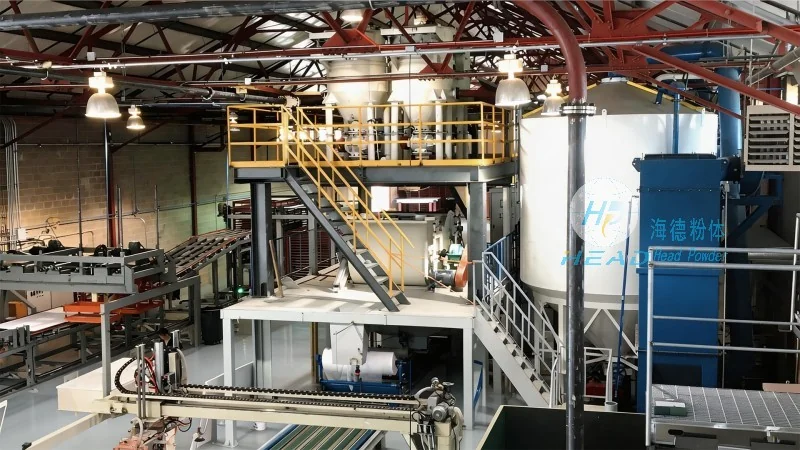
At the heart of this equipment is the ability to automate the entire workflow associated with handling bulk bagged powders. The system typically includes a bulk bag discharger, a pneumatic conveying unit, and associated control systems. These components work in tandem to ensure that powders are transferred from the bulk bag into a storage silo, hopper, or directly into processing machinery without the need for manual intervention. This automation is particularly valuable in industries where consistency, hygiene, and safety are paramount, such as pharmaceuticals, food processing, and chemical manufacturing.
The fundamental principle behind pneumatic conveying is the use of pressurized or vacuum air to move bulk materials through a pipeline. In the context of automatic bulk bag unloading, the system often employs a positive pressure system, where air is blown through the conveying line to push the powder forward. Alternatively, a negative pressure (suction) system may be used, where air is drawn out of the line to pull the powder. The choice of system depends on factors such as the material's characteristics, the distance to be conveyed, and the desired level of dust control. The equipment is engineered to maintain consistent air pressure and flow rates, ensuring reliable and continuous material transfer.
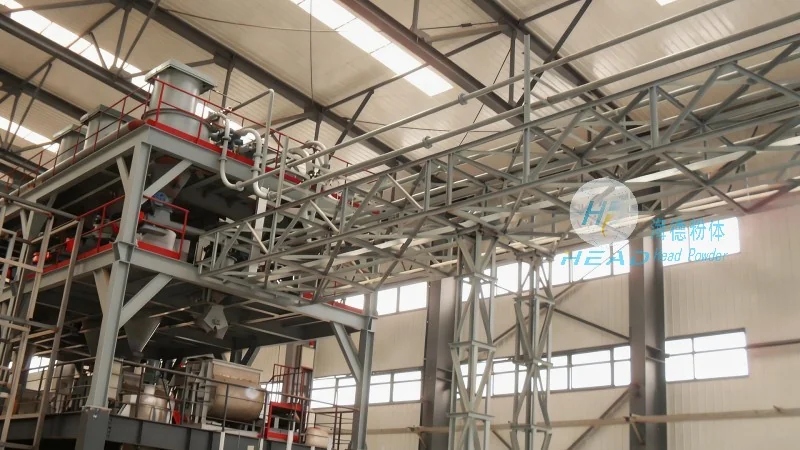
The automatic bulk bag unloading system comprises several critical components, each playing a vital role in the overall operation. The bulk bag discharger, or "unloader," is the primary component responsible for opening the bag and releasing the powder. This unit typically features a hopper with a discharge valve and a sealing mechanism to prevent dust emissions. The pneumatic conveying unit consists of a blower, filter, and a network of pipes that transport the powder from the unloader to the destination. The control system, often integrated with sensors and programmable logic controllers (PLCs), monitors and regulates the flow of material, air pressure, and other parameters to ensure optimal performance. The operational mechanism involves the sequential steps of bag placement, bag opening, powder discharge, and conveying, all controlled by the system's software to achieve a seamless and automated process.
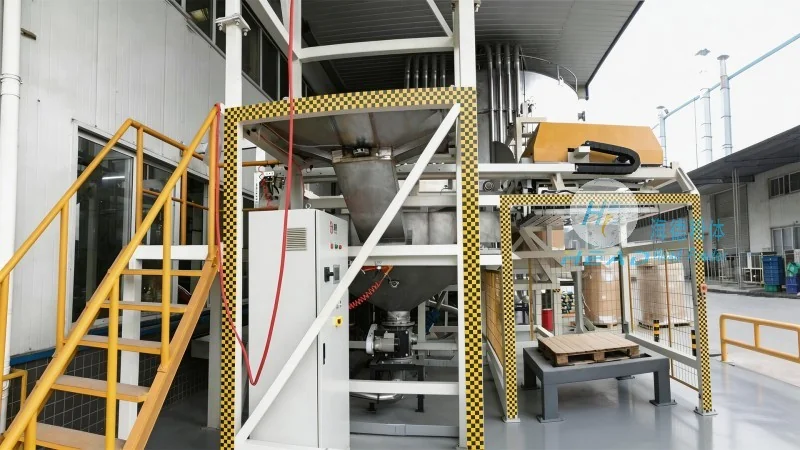
The versatility of automatic bulk bag unloading pneumatic conveying equipment makes it suitable for a wide range of industrial applications. In the chemical industry, it is commonly used to handle raw materials like powders, granules, and solids for manufacturing processes. The food and beverage sector utilizes these systems for the safe and hygienic transfer of ingredients such as flour, sugar, and spices. The pharmaceutical industry benefits from the equipment's ability to maintain strict contamination control and ensure the integrity of sensitive powders. Additionally, in the agricultural and mining sectors, the system can be employed to transport bulk fertilizers, minerals, and other bulk materials. Each application scenario leverages the equipment's ability to handle different material types, from fine powders to coarse granules, while adhering to industry-specific standards for quality and safety.
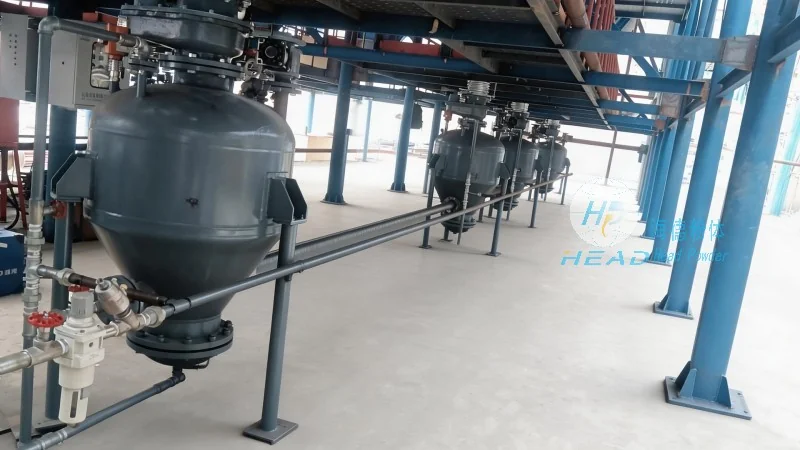
Implementing automatic bulk bag unloading pneumatic conveying equipment offers numerous advantages for industrial operations. One of the most significant benefits is the reduction in labor costs, as the system eliminates the need for manual handling and bag emptying. This not only reduces operational expenses but also minimizes the risk of workplace injuries associated with lifting heavy bags or handling powders manually. The equipment also enhances process efficiency by providing a continuous and consistent flow of material, which can improve production throughput and reduce downtime. Furthermore, the automated nature of the system improves product quality by maintaining consistent material handling and reducing the risk of contamination or degradation. From an environmental perspective, the equipment is designed to minimize dust emissions and improve air quality, contributing to a safer and more sustainable workplace.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field of bulk material handling solutions, specializes in the design, development, and production of advanced pneumatic conveying equipment. HeadPowder is headquartered in Shandong, China, and has established itself as a trusted partner for industries seeking reliable and efficient material handling systems. The company's commitment to innovation and quality has enabled it to deliver customized solutions tailored to the unique needs of each client. With a focus on research and development, HeadPowder continuously improves its products to meet evolving industry standards and customer requirements. The company's facilities in Shandong are equipped with state-of-the-art technology and skilled personnel, ensuring the highest level of product performance and customer satisfaction.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top