Welcome to Shandong HeadPowder Engineering Co., Ltd., a leading provider of advanced vacuum suction powder pneumatic conveying systems. Our company specializes in the design, manufacturing, and integration of efficient and reliable equipment for handling bulk powders in various industrial applications. This article explores the fundamental principles behind vacuum suction pneumatic conveying, as well as the key characteristics and working scenarios where such systems excel.
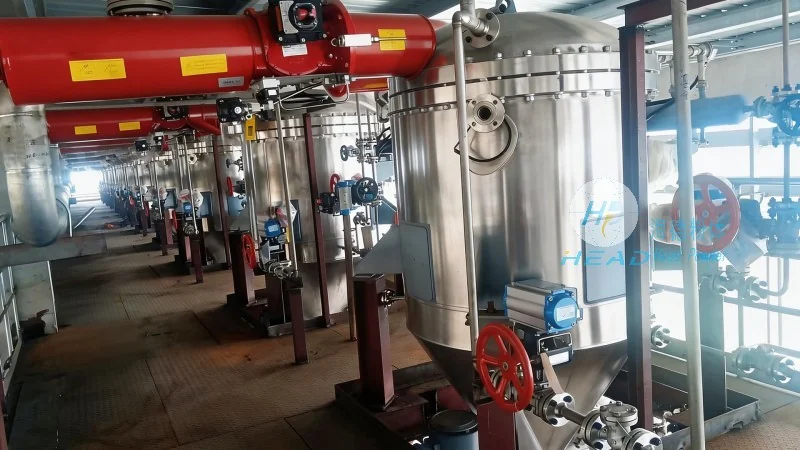
At the heart of vacuum suction powder conveying systems lies the principle of creating a negative pressure environment to draw powders from a source into a transport line. Unlike positive pressure systems that push material through a pipeline, vacuum suction systems utilize a vacuum pump to generate a pressure differential. This differential draws the powder particles into the conveying line along with a controlled flow of air. The process begins with the material being placed in a hopper or storage vessel. A suction nozzle or feed point is then positioned at the material's surface, and the vacuum pump activates, creating a low-pressure zone. As the pressure inside the conveying line drops below the atmospheric pressure at the material's surface, the powder is entrained and pulled into the system. The air-powder mixture travels through the pipeline to a separation or deposition point, where the powder is released and the air is either filtered or recirculated. This method is particularly effective for materials that are prone to dust generation or require a clean, sealed transfer process.
Vacuum suction pneumatic conveying equipment is widely utilized across diverse industrial sectors due to its unique advantages and adaptability. The primary working scene characteristics include:
1. Clean and Contain Dust: One of the most significant benefits of vacuum suction systems is their ability to handle powders in a sealed environment. By drawing material from a source and transporting it through a pipeline under negative pressure, these systems minimize dust emissions and prevent contamination from external air. This is crucial in industries such as pharmaceuticals, food processing, and electronics, where product purity and environmental safety are paramount.
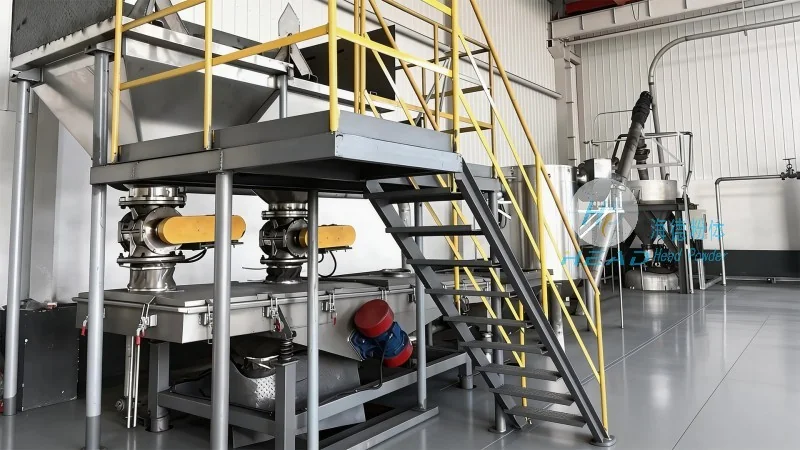
2. Flexible and Versatile Material Handling: Vacuum suction systems can handle a wide range of powder types, including fine powders, granules, and even cohesive or sticky materials. The adjustable suction velocity and pressure control allow for optimization of the conveying process for different material properties. This flexibility makes the equipment suitable for applications involving various bulk materials, from chemical powders to agricultural products.
3. Space Efficiency and Layout Adaptability: Unlike traditional conveyor systems that require extensive space and fixed routes, vacuum suction systems can be installed in compact areas and follow flexible pathways. The ability to route the pipeline around obstacles or through multiple levels makes them ideal for facilities with limited space or complex layouts. This adaptability is particularly valuable in retrofitting existing plants or designing new facilities with optimized material flow.
4. Energy Efficiency and Cost-Effectiveness: While vacuum suction systems may require more initial investment than some alternative methods, they offer long-term cost savings through reduced material waste, lower maintenance costs, and improved operational efficiency. The sealed transfer process minimizes material loss and contamination, while the controlled air flow reduces energy consumption compared to systems that rely on high-pressure air. Over time, these factors contribute to a lower total cost of ownership for the equipment.
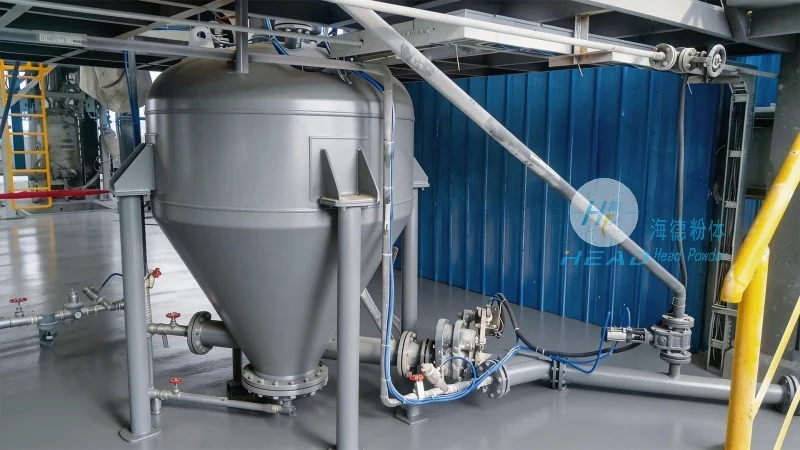
Shandong HeadPowder Engineering Co., Ltd. has successfully implemented vacuum suction pneumatic conveying solutions in numerous industries, demonstrating the equipment's effectiveness in diverse working scenarios. Some of the key applications include:
1. Pharmaceutical and Food Industries: In these sectors, the strict requirements for product purity and hygiene make vacuum suction systems the preferred choice. The sealed transfer process prevents cross-contamination and ensures that powders remain free from external particles or moisture. This is critical for maintaining the quality and safety of pharmaceuticals and food products.
2. Chemical and Petrochemical Manufacturing: Vacuum suction conveying is widely used to handle hazardous or reactive powders, such as chemicals, pigments, and catalysts. The negative pressure environment prevents the release of harmful substances into the workplace, enhancing safety for operators. Additionally, the system's ability to handle abrasive materials without causing wear and tear on components makes it suitable for long-term operation in chemical plants.
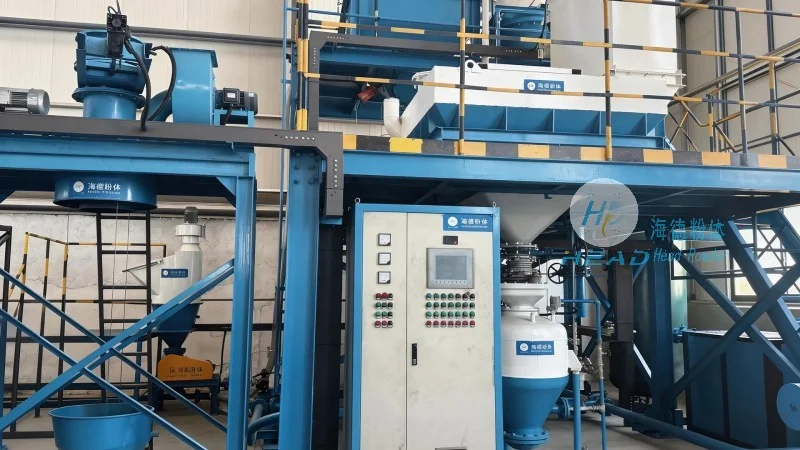
3. Agricultural and Food Processing: For handling bulk agricultural products like grains, flour, or animal feed, vacuum suction systems provide an efficient and hygienic method of transfer. The sealed pipeline reduces the risk of pest infestation and moisture absorption, preserving the quality of the raw materials. This is particularly important in food processing facilities where maintaining product integrity is essential.
4. Mineral Processing and Mining: In mining operations, vacuum suction systems are used to transport fine minerals and ores from storage bins or processing units to processing equipment. The ability to handle abrasive and heavy materials makes the system durable and reliable, even in harsh industrial environments. The sealed transfer also minimizes dust exposure for workers, improving workplace safety.
As industrial processes continue to evolve, the demand for efficient, reliable, and clean material handling solutions has grown. Vacuum suction powder pneumatic conveying systems, provided by Shandong HeadPowder Engineering Co., Ltd., offer a sophisticated solution that addresses the challenges of modern manufacturing. By leveraging the principles of negative pressure and controlled air flow, these systems provide a flexible, hygienic, and cost-effective method for handling bulk powders across various industries. Whether in pharmaceutical, chemical, food, or mining applications, the working scene characteristics of vacuum suction systems make them an indispensable tool for optimizing material flow and ensuring operational excellence. With a commitment to quality and innovation, Shandong HeadPowder Engineering Co., Ltd. remains at the forefront of providing advanced pneumatic conveying solutions that meet the evolving needs of industrial clients worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top