Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer of negative pressure vacuum material handling equipment based in Shandong, China. The company specializes in providing efficient and reliable solutions for material transport in various industrial sectors, including chemical, food, and pharmaceutical industries. This article explores the fundamental principles of negative pressure vacuum systems and highlights the key characteristics and working scenarios where such equipment is most effective.
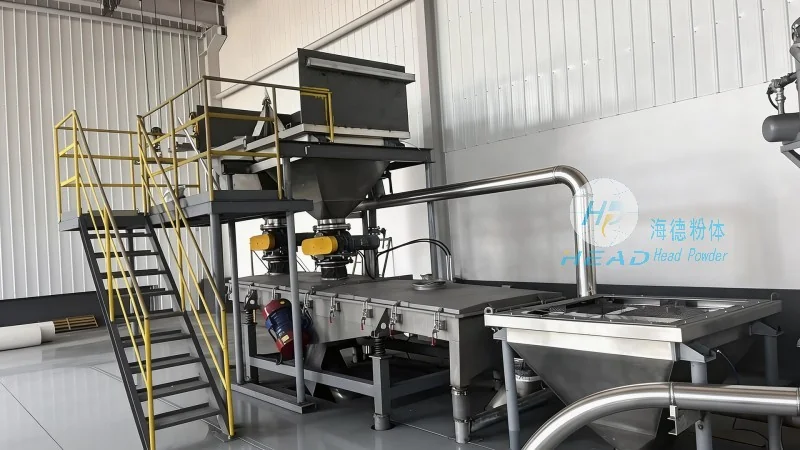
The operation of negative pressure vacuum material handling equipment is based on the principle of pressure differential. A vacuum pump is used to create a low-pressure environment within the conveying pipeline, while the external atmospheric pressure acts as the driving force to push the material from the source into the pipeline. This process is known as suction conveying, as the material is drawn into the system rather than being pushed mechanically. The key components of the system include a vacuum pump, a filter system to prevent dust and particles from entering the pump, a control panel for monitoring and adjusting the system, and a series of pipes and valves to direct the material flow.
The vacuum pump generates a negative pressure that is typically maintained between 0.5 to 1 bar below atmospheric pressure. This pressure differential ensures that the material is continuously pulled into the pipeline as long as the vacuum is maintained. The speed of material transport can be controlled by adjusting the vacuum level, the pipe diameter, and the material's bulk density. For example, a higher vacuum level or a larger pipe diameter will result in faster material flow, while a lower vacuum level or smaller pipe diameter will reduce the flow rate. The system is designed to handle a wide range of materials, from fine powders to granules, with varying particle sizes and moisture content.
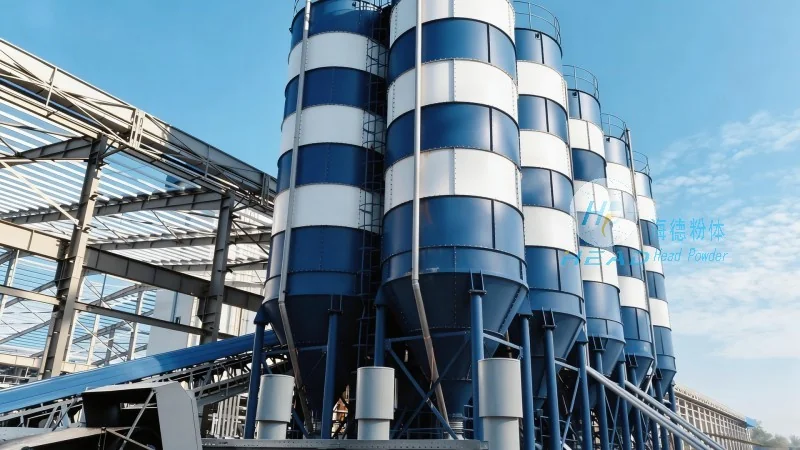
Negative pressure vacuum material handling equipment is widely used in industrial settings where material transport needs to be efficient, hygienic, and safe. The equipment is particularly suitable for applications involving powders and granules that are prone to dust generation or contamination. In the chemical industry, it is commonly used to transfer raw materials such as calcium carbonate, titanium dioxide, and other fine chemicals from storage silos to processing equipment. The sealed pipeline prevents dust from escaping into the environment, ensuring compliance with environmental regulations and maintaining a clean working environment.
In the food and beverage industry, the equipment is used to transfer ingredients like flour, sugar, and spices from raw material bins to production lines. The hygienic design of the system, including smooth surfaces and easy-to-clean components, meets the strict sanitary standards required in food processing facilities. The negative pressure system also helps in maintaining the quality of the materials by preventing cross-contamination and moisture absorption. For example, in the pharmaceutical industry, it is used to transport active pharmaceutical ingredients (APIs) and excipients with high purity requirements, ensuring that the materials remain free from contaminants and are handled in a controlled environment.
The equipment's flexibility allows it to be adapted to different production layouts and scales. It can be used for short-distance transport within a single production line or for long-distance transfer between different buildings or facilities. The modular design of the system enables easy expansion or reconfiguration as production needs change. For instance, additional pipes or vacuum pumps can be added to increase the conveying capacity or to connect multiple material sources to a single receiving point.
One of the main advantages of negative pressure vacuum material handling equipment is its energy efficiency. Compared to positive pressure pneumatic systems, which require higher pressure to push the material, negative pressure systems consume less energy while still achieving high material transport rates. The system also reduces material wear and tear, as the material is conveyed through a sealed pipeline without direct contact with mechanical components like belts or screws. This results in lower maintenance costs and longer equipment lifespan.
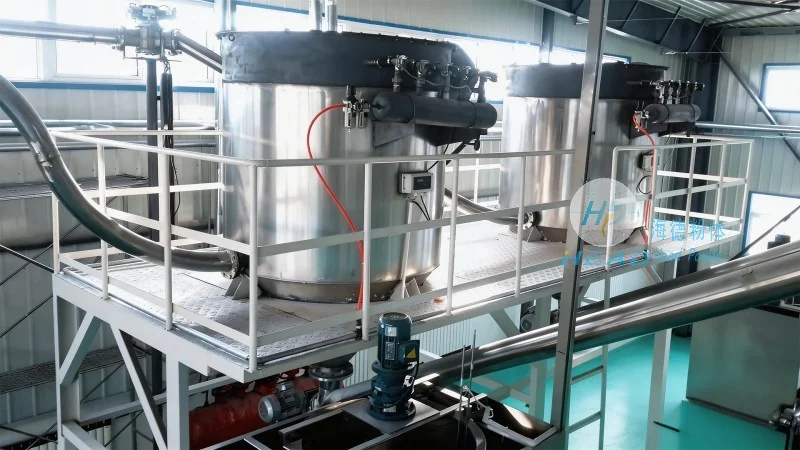
The negative pressure system provides a safe and controlled environment for transporting potentially hazardous materials. The sealed pipeline prevents exposure to the atmosphere, reducing the risk of dust explosions or contamination. The system also allows for precise control over the material flow, with adjustable vacuum levels and valves that can regulate the speed and direction of the material transport. This control is crucial in applications where the material's properties, such as moisture content or particle size, need to be maintained during transport.
In addition to its operational advantages, the equipment offers environmental benefits. By using a vacuum system, the need for compressed air or other external power sources is minimized, reducing energy consumption and operational costs. The sealed pipeline also prevents dust and particles from being released into the air, contributing to a cleaner and healthier working environment. This is particularly important in industries where dust is a health hazard or where environmental regulations are stringent.
Negative pressure vacuum material handling equipment, manufactured by Shandong HeadPowder Engineering Co., Ltd., offers a reliable and efficient solution for material transport in various industrial applications. The system's principle of pressure differential, combined with its hygienic design and flexible configuration, makes it suitable for a wide range of materials and industries. By understanding the working principles and characteristics of this equipment, businesses can make informed decisions about implementing such systems to improve their material handling processes, enhance productivity, and ensure compliance with industry standards.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top