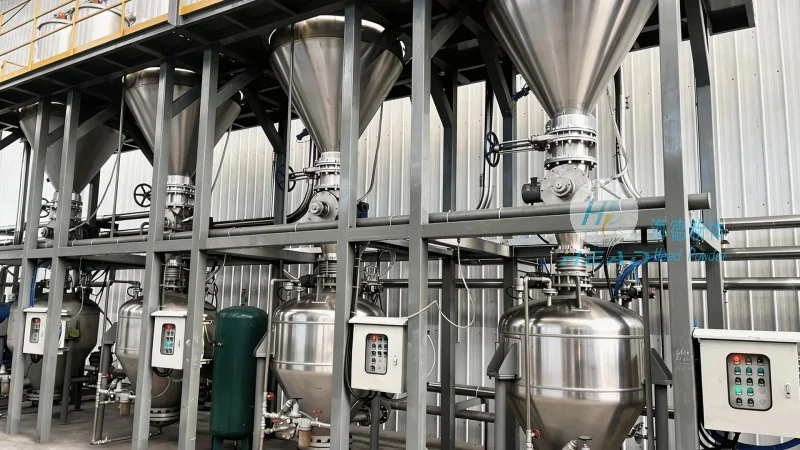
Bin pumps, also known as pressure vessels or pneumatic conveyors, are critical components in material handling and bulk material transport applications. These systems are designed to efficiently transport dry bulk materials over long distances with minimal maintenance and operational costs. The core functionality of a bin pump involves the use of compressed air or other gases to create pressure differentials that move material from a storage bin or hopper to the discharge point. This technology is widely adopted in industries such as mining, cement production, food processing, and chemical manufacturing due to its flexibility and ability to handle a wide range of materials, including powders, granules, and fine particles.
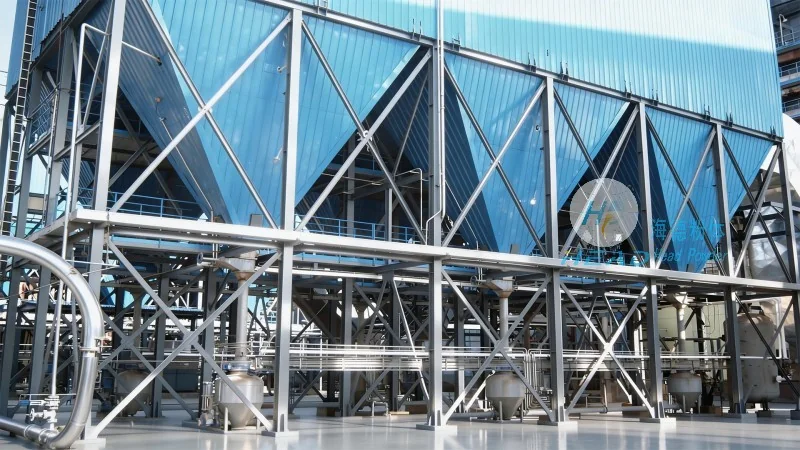
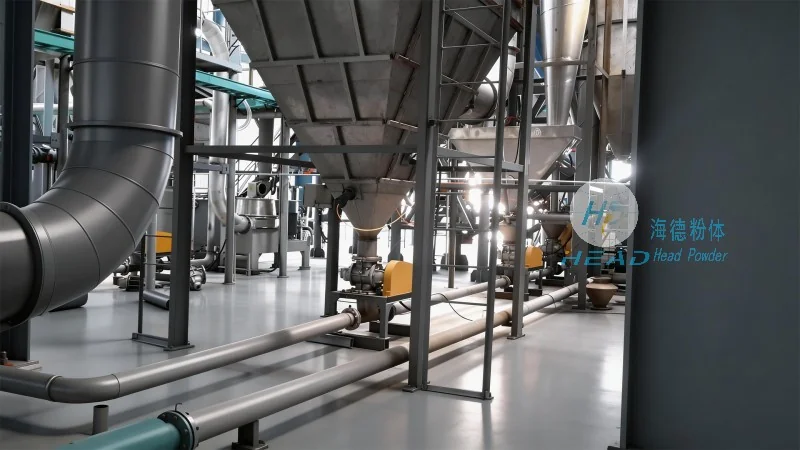
The fundamental principle of bin pump operation is based on the creation of a pressure differential between the inlet and outlet of the system. The process typically begins with the material being fed into the bin pump from a hopper or storage silo. As the material accumulates, a pressure is built up inside the pump chamber. When the pressure reaches a predetermined level, a valve opens, allowing compressed air to be introduced into the pump. This compressed air then forces the material out of the pump through the discharge line, transporting it to the target location. The cycle repeats as the material level in the bin decreases, and the pump refills with more material. The control system, which may include sensors and automated valves, ensures that the process operates smoothly and efficiently, maintaining consistent material flow rates and preventing overpressurization or underfilling.
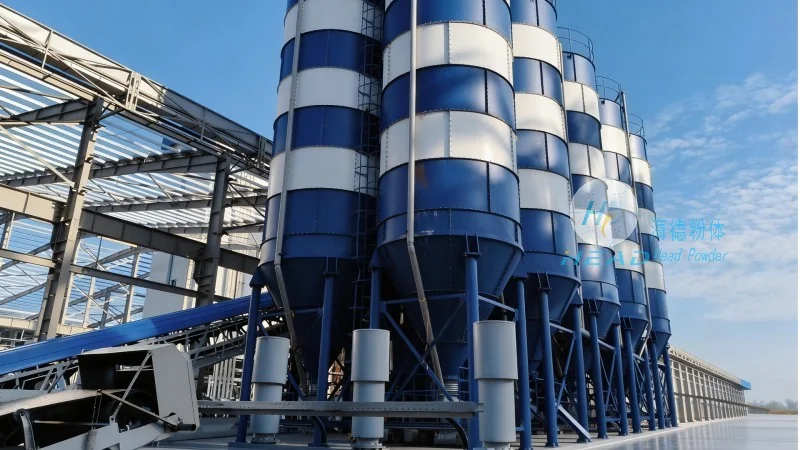
Bin pump systems are characterized by several distinct working scene features that make them suitable for various industrial applications. One of the primary advantages is their ability to handle long-distance material transport with minimal energy consumption compared to traditional methods like belt conveyors or trucks. The system's compact design allows for installation in confined spaces, making it ideal for retrofitting into existing facilities or in new plant layouts where space is limited. Additionally, bin pumps can operate under varying material conditions, including different particle sizes, moisture contents, and flow characteristics, without significant performance degradation. The pneumatic nature of the system also provides a degree of safety, as it eliminates the need for mechanical parts that could cause material blockages or equipment damage. Furthermore, the system's flexibility allows for easy integration with other processing equipment, such as mixers, classifiers, or storage tanks, enabling seamless material flow throughout the production line.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field of material handling equipment, specializes in the design, development, and production of high-quality bin pump systems. With a strong commitment to innovation and customer satisfaction, the company has established itself as a trusted partner for industries requiring reliable and efficient bulk material transport solutions. HeadPowder's products are engineered to meet international standards and are backed by rigorous quality control processes to ensure durability and performance. The company's team of experienced engineers and technicians provides comprehensive support, from system design and installation to maintenance and after-sales service, ensuring that clients receive tailored solutions that address their specific operational needs. HeadPowder's facilities in Shandong, China, are equipped with advanced manufacturing capabilities and testing equipment, enabling the production of customized bin pump systems that are optimized for different applications and material types.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top