HeadPowder, a leading manufacturer based in Shandong, China, specializes in providing advanced material handling solutions. This article delves into the fundamental principles and operational characteristics of continuous material feeding conveying systems, highlighting their efficiency and versatility in various industrial applications.
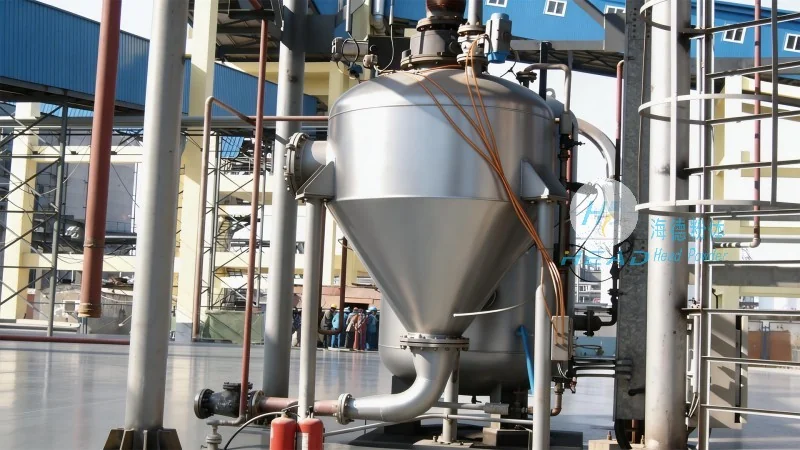
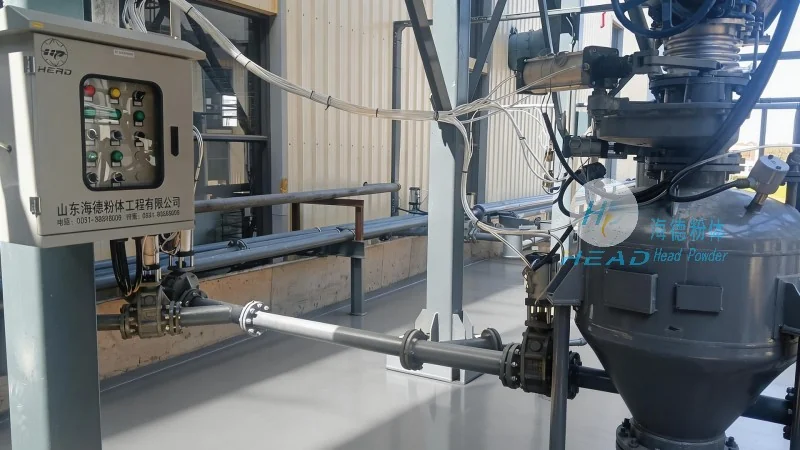
Continuous material feeding conveying systems are designed to transport bulk materials from a source to a destination in a seamless, uninterrupted manner. The core principle involves the use of mechanical components such as conveyor belts, rollers, or chains to move materials through a defined path. These systems typically operate by converting energy (e.g., electrical power) into kinetic energy, enabling the consistent movement of materials. The design ensures minimal downtime and high throughput, making them ideal for high-volume production environments. The system's efficiency is enhanced by features like variable speed control, which allows for adjustments based on material type and processing requirements. Additionally, the integration of sensors and control systems enables real-time monitoring and automation, further optimizing performance.
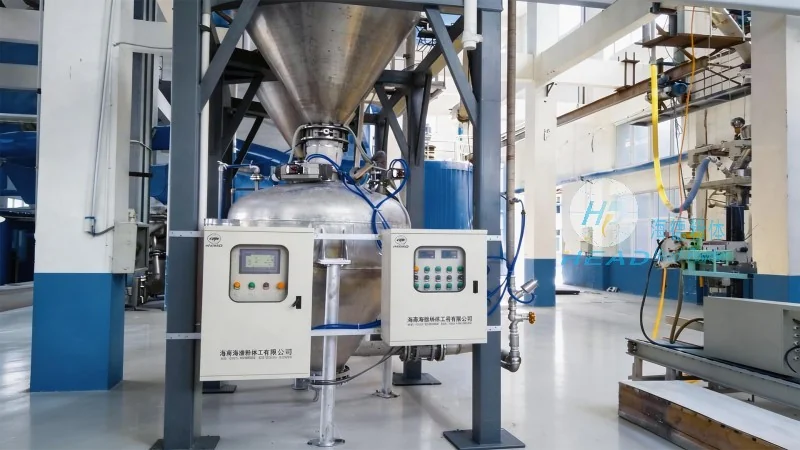
Continuous material feeding conveying systems are widely used across diverse industrial sectors, each presenting unique operational characteristics that influence system design and performance. In manufacturing plants, these systems are crucial for feeding raw materials to processing equipment, ensuring a steady supply for production lines. The characteristics include high reliability, as they are built to withstand heavy loads and continuous operation. In mining and construction industries, the systems handle bulk materials like ores, gravel, and sand, where durability and resistance to harsh conditions are paramount. The working environment often involves dust, moisture, and temperature variations, requiring robust construction materials and protective enclosures. Another key characteristic is adaptability, as systems can be customized to accommodate different material sizes, shapes, and flow rates. This flexibility allows for integration with existing infrastructure, minimizing installation time and costs. Furthermore, the systems are designed for easy maintenance, with accessible components that facilitate routine checks and repairs, reducing overall operational downtime.
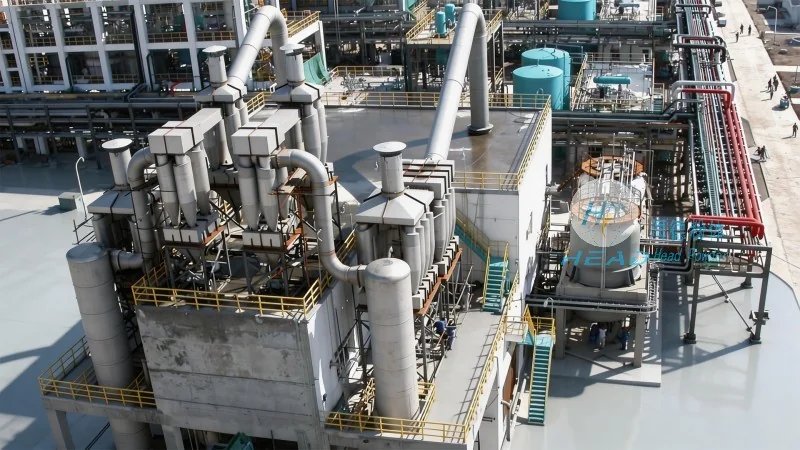
Practical applications of continuous material feeding conveying systems showcase their adaptability and efficiency in real-world scenarios. For example, in food processing facilities, these systems handle raw ingredients like grains and powders, ensuring hygienic and consistent feeding into production lines. The systems are equipped with sanitary components, such as stainless steel construction and easy-to-clean surfaces, which meet regulatory standards for food safety. In the chemical industry, the systems transport powders and granules with precision, minimizing dust generation and contamination risks. The use of enclosed conveyor designs and dust collection systems enhances safety and compliance. Additionally, the systems' ability to handle varying material densities and flow rates makes them suitable for dynamic production environments where demand fluctuates. This flexibility allows manufacturers to adjust feed rates in response to changing production schedules, optimizing resource utilization and reducing waste. The integration of advanced control technologies, such as PLC (Programmable Logic Controllers) and SCADA (Supervisory Control and Data Acquisition) systems, enables remote monitoring and data analysis, providing insights into system performance and potential areas for improvement.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top