HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, development, and production of advanced dust-free powder feeding and conveying systems. This article delves into the fundamental principles behind these systems and highlights the key characteristics of their operational environments, providing a comprehensive understanding for potential users and industry professionals.
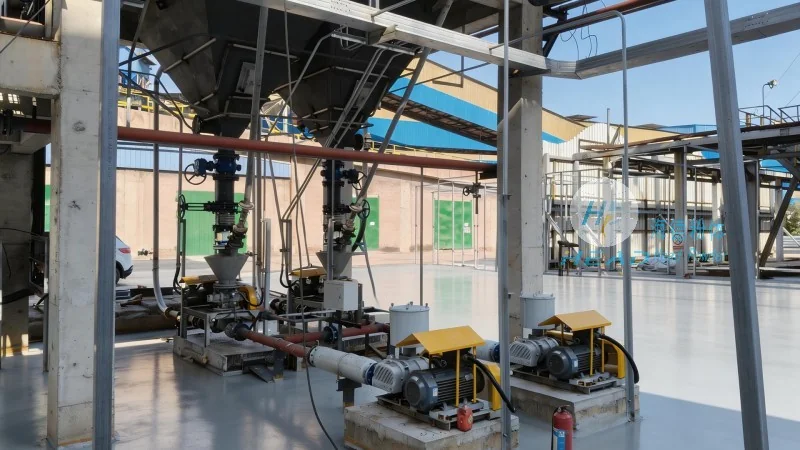
HeadPowder Engineering Co., Ltd. is headquartered in Shandong, China, where the company has established itself as a trusted provider of high-quality powder handling solutions. The company's commitment to innovation and precision engineering has led to the development of sophisticated systems that ensure efficient, safe, and clean transfer of powders in various industrial applications. These systems are crucial for industries such as pharmaceuticals, food processing, chemical manufacturing, and more, where maintaining a dust-free environment is paramount to product quality and operational safety.
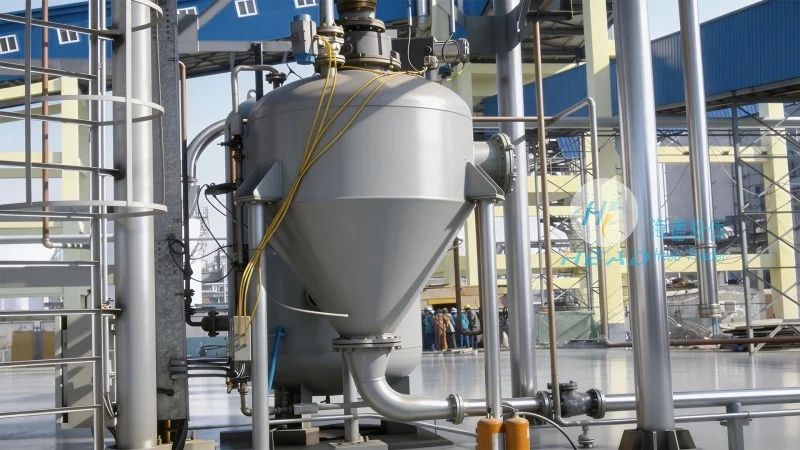
The fundamental principle of dust-free powder feeding and conveying systems is to minimize particle dispersion and prevent contamination during the transfer process. Traditional methods often involve the use of air or mechanical systems that can generate dust, leading to health hazards and product degradation. In contrast, modern dust-free systems employ enclosed, sealed mechanisms that control the movement of powders within a controlled environment. This approach ensures that the material remains contained, reducing the risk of airborne particles and maintaining the integrity of the product. The systems typically consist of components like feeders, conveyors, and dust collection units, all working in tandem to achieve a seamless and clean transfer.
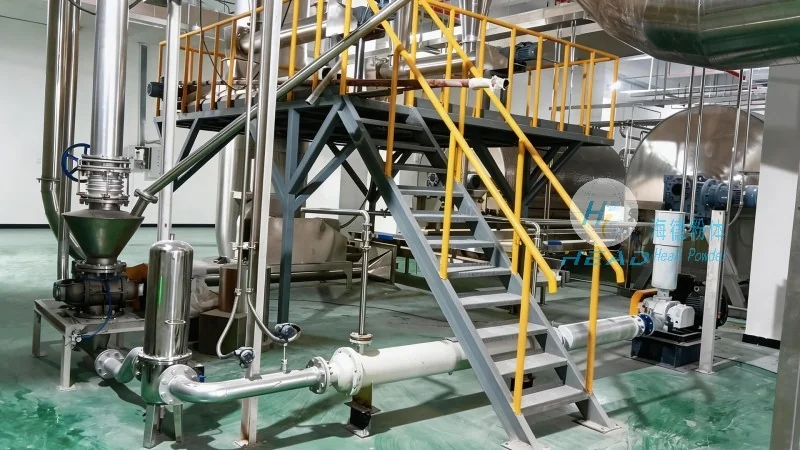
The operational characteristics of these systems are tailored to meet the specific demands of different industrial settings. For instance, in pharmaceutical manufacturing, where product purity is non-negotiable, the systems are designed to operate in a sterile, controlled environment. This involves features such as HEPA filters, sealed enclosures, and automated controls that minimize human interaction and prevent cross-contamination. In food processing facilities, the systems are constructed from food-grade materials and comply with stringent hygiene standards, ensuring that the powders remain free from contaminants and meet regulatory requirements. Chemical manufacturing environments, on the other hand, require robust systems capable of handling abrasive or corrosive powders, with features like corrosion-resistant materials and specialized sealing mechanisms to prevent leaks and maintain operational safety.
HeadPowder's dust-free powder feeding and conveying systems offer numerous advantages that make them ideal for a wide range of applications. One of the primary benefits is the enhanced product quality, as the systems prevent dust accumulation and contamination, which can affect the performance and shelf life of the final product. Additionally, these systems improve operational efficiency by reducing downtime due to maintenance and cleaning, as the enclosed design minimizes the need for frequent cleaning and reduces the risk of equipment failure. The systems also contribute to a safer working environment by eliminating the health risks associated with airborne dust particles, such as respiratory issues and allergic reactions. In industries like pharmaceuticals and food processing, where regulatory compliance is critical, these systems help companies meet stringent standards and avoid costly penalties. The versatility of the systems allows them to be adapted to various powder types, including fine powders, granules, and bulk materials, making them suitable for diverse applications from small-scale laboratory use to large-scale industrial production.
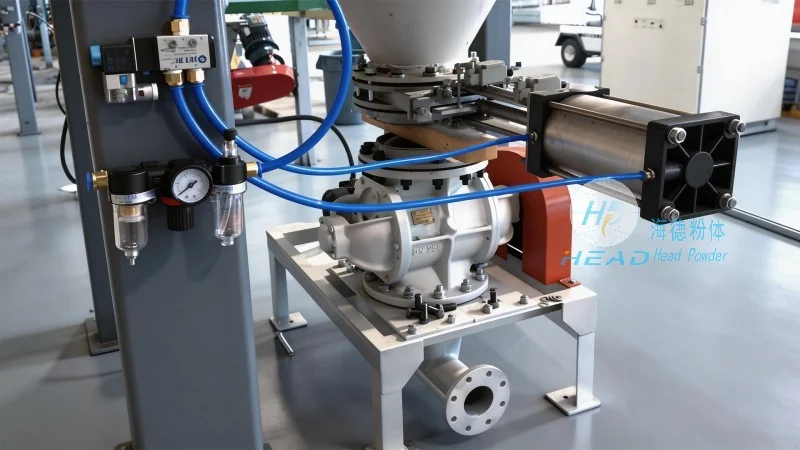
HeadPowder Engineering Co., Ltd. continues to lead the way in the development of advanced dust-free powder feeding and conveying systems, leveraging its expertise and innovation to meet the evolving needs of various industries. By understanding the core principles and operational characteristics of these systems, users can make informed decisions about implementing the right technology for their specific applications. The company's commitment to quality, safety, and efficiency ensures that its products remain at the forefront of powder handling solutions, providing reliable and effective solutions for industries worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top