High-alumina fly ash powder conveying equipment is a specialized system designed for the efficient and reliable transport of high-alumina fly ash, a byproduct commonly generated in coal-fired power plants. This equipment plays a crucial role in industrial processes where the handling of such powders is essential for maintaining operational efficiency and safety. The design and functionality of these systems are tailored to meet the unique challenges associated with high-alumina fly ash, including its abrasive nature, potential for dust generation, and the need for precise control over material flow.
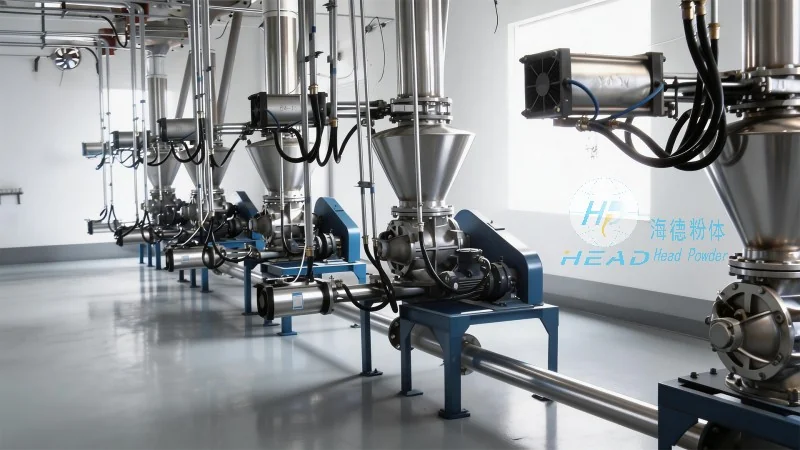
The core principle of high-alumina fly ash powder conveying equipment revolves around the use of positive pressure or negative pressure systems to move the material through a network of pipes. Positive pressure systems, such as pneumatic conveyors, utilize compressed air to push the fly ash through the pipeline, while negative pressure systems, like vacuum conveyors, use suction to draw the material. The choice between these systems depends on factors like the distance of transport, the volume of material, and the specific characteristics of the fly ash. In high-alumina applications, the equipment must be constructed from materials resistant to corrosion and abrasion, such as stainless steel or specialized alloys, to ensure long-term durability and performance.
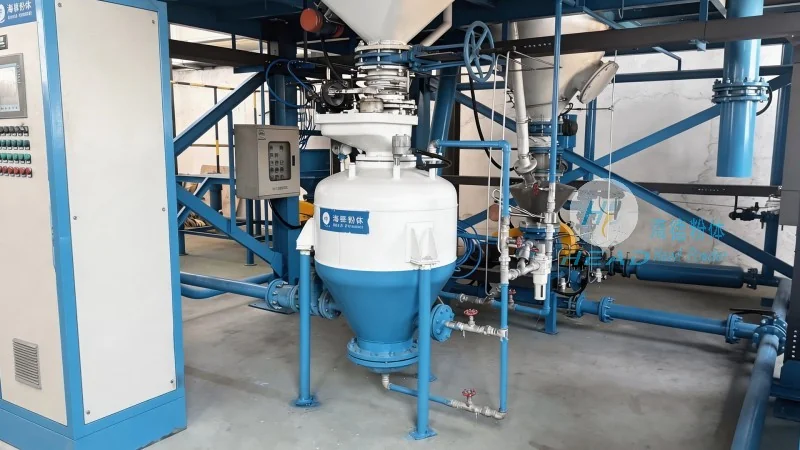
High-alumina fly ash powder conveying equipment typically consists of several key components that work in tandem to achieve effective material transport. These include the hopper or feed hopper, which serves as the initial collection point for the fly ash; the conveyor itself, which may be a pneumatic or mechanical system; and the control valves and regulators that manage the flow rate and pressure. The hopper is often equipped with a sealing mechanism to prevent dust leakage and maintain a stable feeding environment. The conveyor system may incorporate features like cyclone separators or filters to separate any entrained air or fine particles, ensuring that the material is delivered in a clean and controlled manner. Additionally, the system may include a dust collection unit to comply with environmental regulations and protect the surrounding environment from particulate emissions.
The working scene characteristics of high-alumina fly ash powder conveying equipment are shaped by the diverse industrial environments where they are deployed. These systems are commonly used in power generation facilities, cement plants, and other industrial sites where fly ash is a byproduct of combustion processes. The equipment must be able to handle varying particle sizes and moisture content, as these factors can impact the flow characteristics of the material. In power plants, for example, the conveying equipment may be integrated into the ash handling system, working in conjunction with other components like ash silos and storage tanks. The working scene may also involve long-distance transport, requiring the system to maintain consistent pressure and flow rates over extended periods. The equipment is designed to operate in harsh conditions, including high temperatures and abrasive environments, making it suitable for continuous industrial use. Furthermore, the system may need to accommodate changes in material feed rates, such as during start-up or shutdown procedures, which necessitates flexible control mechanisms to prevent system overload or blockages.
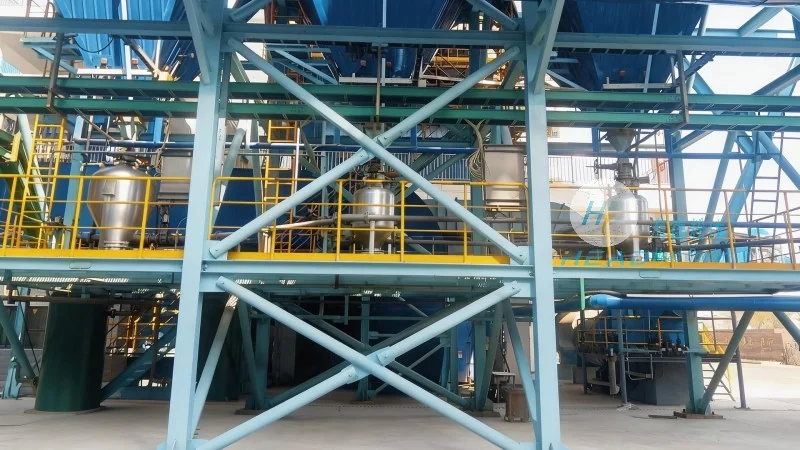
Implementing high-alumina fly ash powder conveying equipment offers several advantages that contribute to improved operational efficiency and cost-effectiveness. One of the primary benefits is the reduction in labor costs associated with manual handling of fly ash, as the automated system minimizes the need for human intervention in the material transport process. Additionally, the equipment helps to improve safety by reducing exposure to dust and minimizing the risk of accidents associated with manual handling. The precise control over material flow also contributes to better process consistency, ensuring that the fly ash is delivered to its intended destination in a uniform manner. From an environmental perspective, the system helps to minimize dust emissions and comply with regulatory standards, thereby reducing the environmental impact of the industrial operation. The durability of the equipment, particularly when constructed from corrosion-resistant materials, leads to lower maintenance costs and longer service life, providing a favorable return on investment for industrial facilities.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top