Food processing industries rely on efficient and hygienic material handling solutions to maintain product quality and operational efficiency. Among the various technologies available, food pneumatic conveying systems have emerged as a preferred choice for transporting bulk food products. This article explores the fundamental principles behind these systems and highlights key application scenarios that demonstrate their versatility and effectiveness in the food industry.
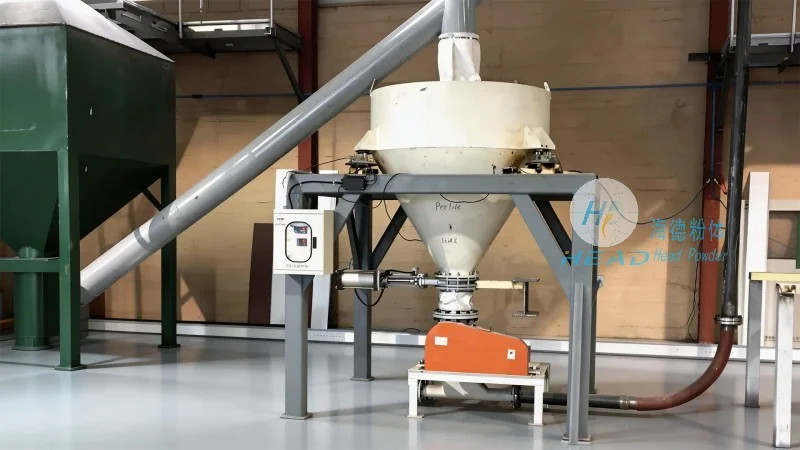
The operation of a food pneumatic conveying system is based on the principle of transporting solid materials through a pipeline using a moving gas stream, typically air or a mixture of air and other gases. Unlike mechanical conveying methods that rely on physical contact or gravity, pneumatic systems utilize pressure differentials to move materials. The system typically consists of a hopper for material storage, a conveyor line, a control unit, and a discharge point. The process begins when the material is fed into the hopper, where it is then drawn into the conveyor line by the pressure difference created by the moving air. This method allows for the continuous and controlled movement of food products without direct contact with machinery, which is crucial for maintaining hygiene standards in food processing.
Several critical components work together to ensure the smooth operation of a food pneumatic conveying system. The hopper serves as the initial storage and feeding unit, where bulk food materials are collected before being introduced into the system. The conveyor line, often made of stainless steel to meet sanitary requirements, is the main pathway for material transport. The control unit, equipped with sensors and valves, regulates the air flow and pressure to maintain optimal conveying conditions. Additionally, filters and cyclones are integrated to separate the conveyed material from the air stream, ensuring that only clean air is released and that the material is not contaminated. These components are designed to be easy to clean and maintain, which is essential for compliance with food safety regulations.
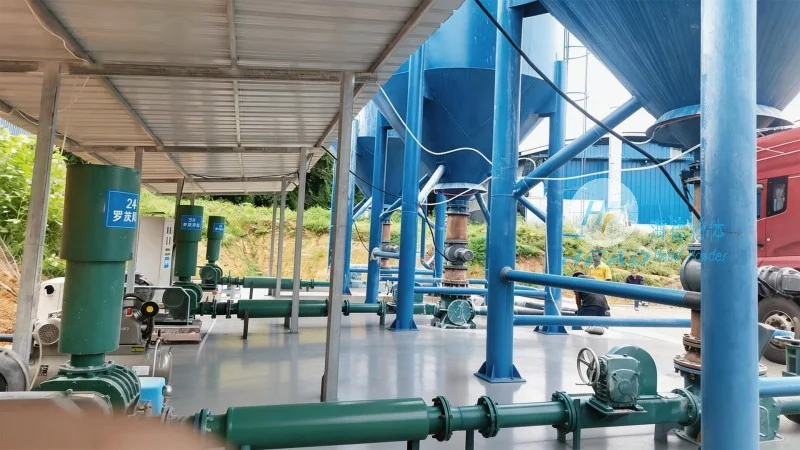
Food pneumatic conveying systems are widely used across various sectors of the food industry due to their adaptability and efficiency. In the bakery industry, these systems are commonly employed to transport flour, sugar, and other dry ingredients from storage to production lines. The ability to handle fine powders without caking or segregation makes them ideal for maintaining product consistency. In the snack food industry, they are used to convey ingredients like nuts, seeds, and spices, ensuring uniform mixing and preventing contamination. The dairy industry also benefits from pneumatic conveying systems when handling powders such as milk powder or whey protein, as they can maintain product integrity and prevent moisture absorption. Another significant application is in the confectionery industry, where systems are used to transport sugar, cocoa, and other sweeteners, allowing for precise dosing and reducing the risk of product damage.
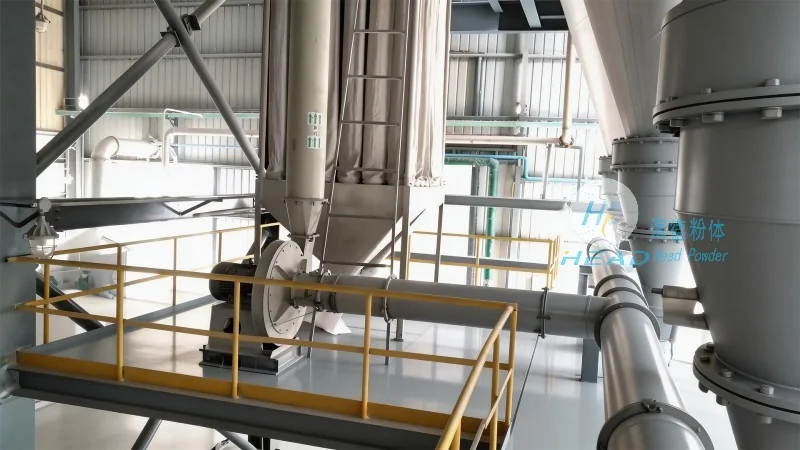
Compared to traditional mechanical conveying methods, food pneumatic conveying systems offer several advantages that make them a preferred choice for many food processing facilities. One of the primary benefits is the elimination of direct contact between the product and the conveying equipment, which significantly reduces the risk of contamination and ensures product purity. This is particularly important for food products that require strict hygiene standards. Additionally, pneumatic systems can handle a wide range of materials, from fine powders to granules, without the need for adjustments. They also offer flexibility in terms of layout, as the conveyor lines can be easily reconfigured to accommodate changes in production processes. Furthermore, these systems are generally more energy-efficient than mechanical alternatives, as they require less power to operate and can handle longer distances with minimal loss of material. The ability to maintain consistent flow rates and prevent material degradation also contributes to improved product quality and reduced waste.
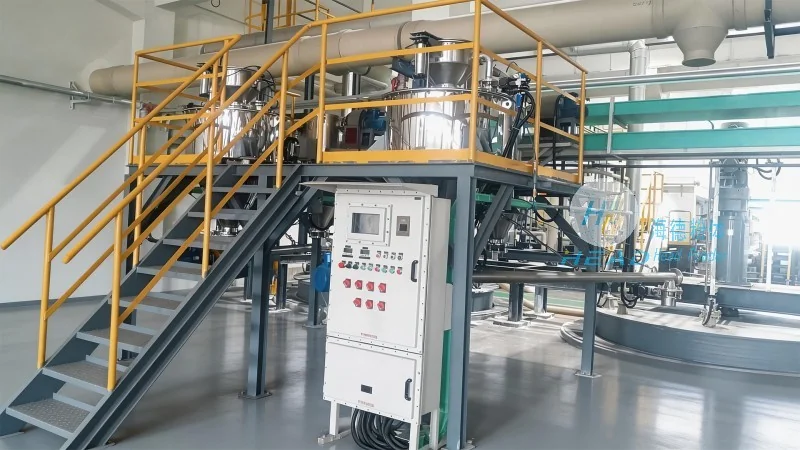
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of food processing equipment, recently implemented a pneumatic conveying system in a large-scale bakery facility. The system was designed to transport 10 tons of flour per hour from storage silos to the production line. The project involved integrating the system with existing equipment and ensuring compliance with food safety regulations. The results were significant: the system reduced material handling time by 30% and improved product consistency by eliminating segregation. The plant also reported a decrease in labor costs due to the automated feeding process. This case study highlights the practical benefits of pneumatic conveying systems in real-world applications and demonstrates the expertise of companies like Shandong HeadPowder in providing tailored solutions for the food industry.
Food pneumatic conveying systems represent a sophisticated and effective solution for material handling in the food industry. By leveraging the principles of air pressure and flow, these systems offer superior hygiene, efficiency, and flexibility compared to traditional methods. As the food industry continues to evolve, the demand for advanced material handling technologies will likely increase, driving further innovation in pneumatic conveying systems. Companies like Shandong HeadPowder Engineering Co., Ltd. play a crucial role in developing and implementing these solutions, ensuring that food processing facilities can meet the highest standards of quality and safety. The continued adoption of pneumatic conveying systems will undoubtedly contribute to the overall efficiency and sustainability of the food industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top