Intelligent bag-opening pneumatic conveying systems represent a sophisticated solution in material handling, merging advanced automation with traditional pneumatic transport technologies. This technology is designed to streamline the process of transferring bulk materials from sealed bags into processing or storage systems, enhancing efficiency and reducing labor costs. The system integrates intelligent bag opening mechanisms with pneumatic conveying infrastructure, enabling seamless material flow from the point of origin to the destination.
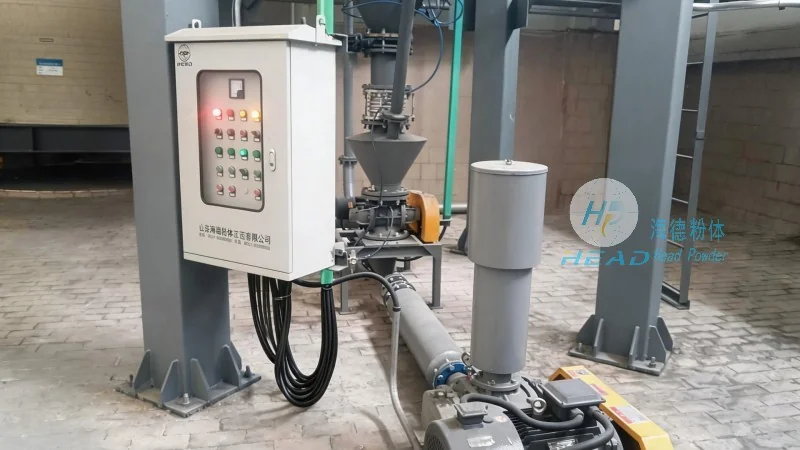
The fundamental principle of pneumatic conveying involves using compressed air to transport dry bulk materials through a pipeline system. In the context of intelligent bag-opening systems, this process is enhanced by automated bag opening, which eliminates the need for manual intervention. The system typically consists of several key components: a bag opening unit, a hopper or feeder, a conveying pipeline, and a receiving container or processing unit. The compressed air is introduced into the bag, causing it to rupture or open, and the material is then drawn into the conveying line by the air flow. This creates a consistent and controlled flow of material, ensuring minimal loss and contamination.
Key technical aspects include the selection of appropriate air pressure and flow rates, which are critical for maintaining material velocity and preventing blockages. The intelligent bag opening mechanism may use mechanical, pneumatic, or even ultrasonic methods to open the bag, depending on the material properties and bag type. For instance, mechanical cutters are suitable for rigid or thick bags, while pneumatic actuators are effective for lighter, flexible bags. The system also incorporates sensors and controls to monitor the opening process and adjust air pressure as needed, ensuring optimal performance.
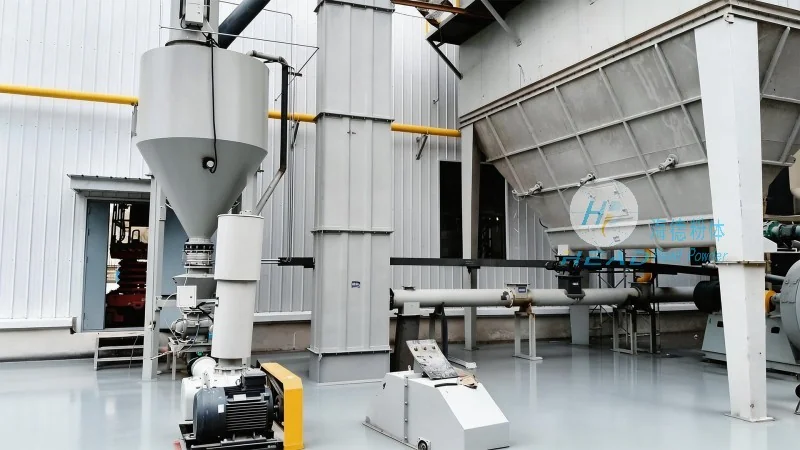
Intelligent bag-opening pneumatic conveying systems are widely applied across various industries due to their adaptability and efficiency. In the pharmaceutical sector, these systems are used to handle sensitive powders and granules, ensuring sterile and contamination-free transfer. The automated bag opening prevents cross-contamination and maintains the integrity of the material, which is crucial for pharmaceutical products. Similarly, in the food industry, the systems are employed to transfer ingredients such as flour, sugar, and spices, maintaining hygiene standards and preventing product degradation.
In the chemical industry, the technology is utilized for handling a variety of powders and granules, including fine chemicals and bulk chemicals. The intelligent bag opening ensures safe and efficient transfer, reducing the risk of dust explosions and material loss. The systems are also suitable for industrial applications in the mining and construction sectors, where large volumes of bulk materials like cement, sand, and gravel are transported from storage to processing sites. The ability to handle different material types and bag sizes makes the system versatile for diverse industrial needs.
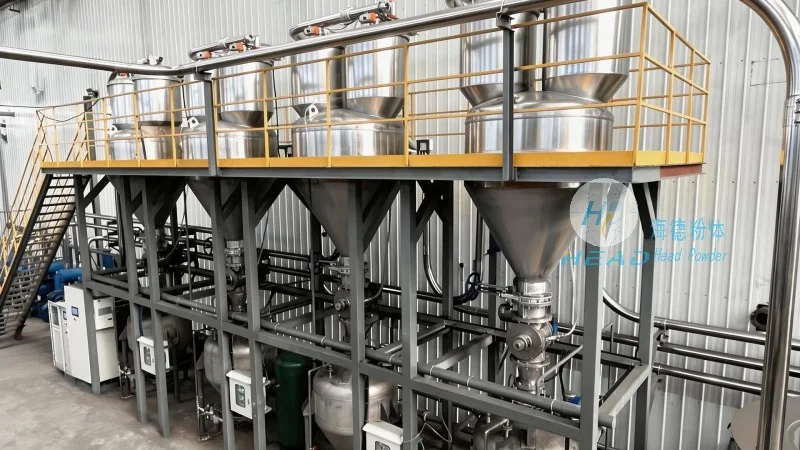
Implementing an intelligent bag-opening pneumatic conveying system offers several advantages over traditional manual or semi-automated methods. Firstly, it significantly reduces labor costs by automating the bag opening and material transfer process. This eliminates the need for manual handling, which is not only labor-intensive but also poses health and safety risks, such as dust inhalation and physical strain. Secondly, the system enhances material handling efficiency by providing a continuous and controlled flow of material, reducing downtime and increasing production throughput.
Another key benefit is the improvement in material quality and consistency. By preventing material spillage and contamination during the transfer process, the system ensures that the material reaching the processing stage is of high quality. This is particularly important in industries where product purity and consistency are critical, such as pharmaceuticals and food processing. Additionally, the system reduces operational costs by minimizing energy consumption and maintenance requirements. The automated controls and sensors help in optimizing air pressure and flow rates, leading to energy savings and longer equipment lifespan.
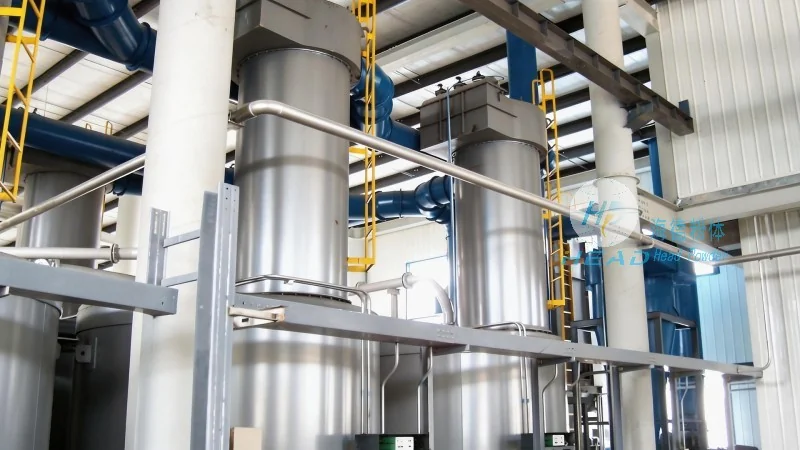
HeadPowder, as a leading provider of material handling solutions, specializes in designing and manufacturing intelligent bag-opening pneumatic conveying systems. With a strong presence in China, particularly in Shandong province, the company has established itself as a trusted partner for industries seeking efficient and reliable material transfer solutions. The company's headquarters is located in Shandong, China, where it leverages advanced technology and engineering expertise to develop innovative solutions tailored to the specific needs of its clients.
HeadPowder's commitment to quality and customer satisfaction is reflected in its comprehensive product range and after-sales support services. The company offers customized solutions that integrate the latest technological advancements, ensuring that clients receive systems that are not only efficient but also compliant with industry standards and regulations. By focusing on research and development, HeadPowder continuously improves its products to meet evolving industry demands and provide sustainable solutions for material handling challenges.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top