For industries dealing with calcium carbonate powder, selecting the right material handling system is crucial for operational efficiency and environmental compliance. Pneumatic conveying systems offer a superior alternative to traditional methods, providing not only enhanced productivity but also reduced environmental impact. This article explores the benefits and applications of calcium carbonate powder pneumatic conveying, highlighting how Shandong HeadPowder Engineering Co., Ltd. delivers innovative solutions tailored to meet these demands.
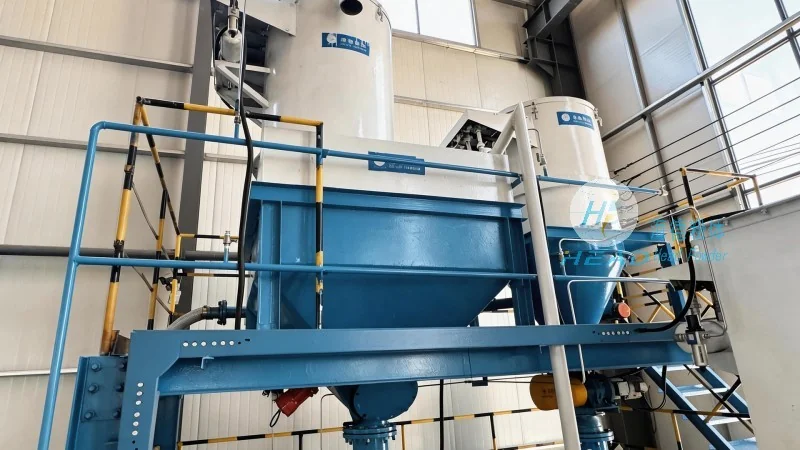
Pneumatic conveying systems utilize air or gas to transport bulk materials like calcium carbonate powder through a network of pipes. Unlike mechanical systems that rely on belts or buckets, pneumatic conveyors offer a more flexible and efficient approach to material movement. The process involves generating airflow within the pipeline, which draws the powder particles into the system and transports them to the desired destination. This method is particularly advantageous for calcium carbonate powder due to its fine particle size and sensitivity to handling, as it minimizes product degradation and contamination.
Implementing a pneumatic conveying system for calcium carbonate powder brings several key benefits that enhance overall operational performance. First, it significantly improves material handling efficiency by reducing downtime associated with manual or mechanical transfer. The automated process ensures consistent flow rates and minimal interruptions, leading to higher throughput and better productivity. Additionally, pneumatic systems are designed to be compact and adaptable, allowing for easy integration into existing production lines without major structural modifications. This flexibility makes them suitable for various industrial settings, from small-scale operations to large-scale manufacturing facilities.
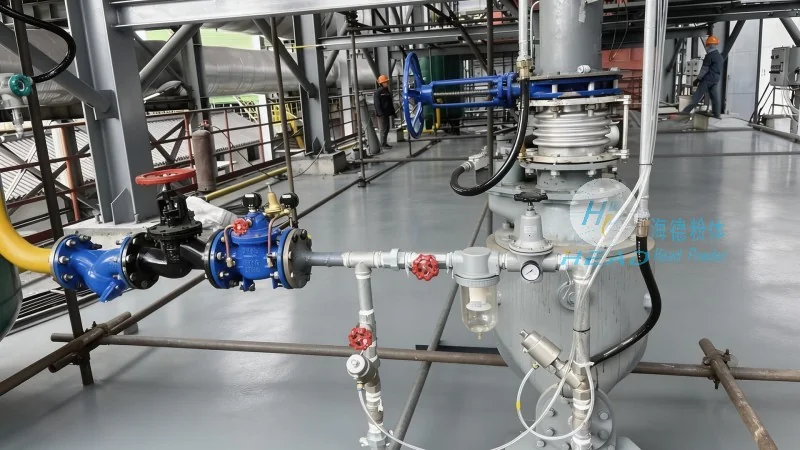
Another critical advantage is the environmental friendliness of pneumatic conveying. Unlike traditional methods that may involve dust generation and emissions, pneumatic systems are enclosed, preventing dust from escaping into the environment. This not only complies with environmental regulations but also improves workplace safety by reducing the risk of respiratory issues among workers. Furthermore, the energy efficiency of modern pneumatic systems contributes to lower operational costs and a smaller carbon footprint, aligning with sustainability goals in the industry.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, specializes in providing advanced pneumatic conveying solutions for calcium carbonate powder and other bulk materials. With a strong commitment to innovation and customer satisfaction, HeadPowder offers tailored systems that address the unique challenges faced by each client. The company’s expertise lies in designing and manufacturing high-quality pneumatic conveying equipment that meets the specific requirements of the calcium carbonate industry, ensuring optimal performance and reliability.
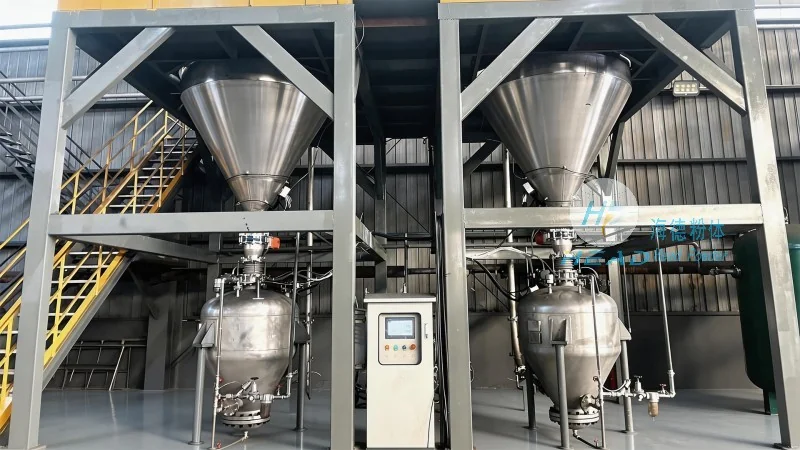
HeadPowder’s approach to pneumatic conveying involves a comprehensive understanding of the material’s properties, such as particle size distribution, moisture content, and flow characteristics. By analyzing these factors, the company can recommend the most suitable conveying method—whether it be pressure or vacuum systems—based on the application and operational needs. This customized approach ensures that the system is not only efficient but also cost-effective, minimizing waste and maximizing resource utilization.
The versatility of calcium carbonate powder pneumatic conveying is evident in its widespread application across various industries. In the paper and plastic manufacturing sectors, calcium carbonate is used as a filler and reinforcement material, and pneumatic systems efficiently transport it from storage to processing units. Similarly, in the construction industry, where calcium carbonate is used in cement and concrete production, pneumatic conveyors ensure smooth material transfer, reducing labor costs and improving production speed. The system’s ability to handle fine powders without clogging or degradation makes it ideal for these applications, contributing to higher product quality and consistency.
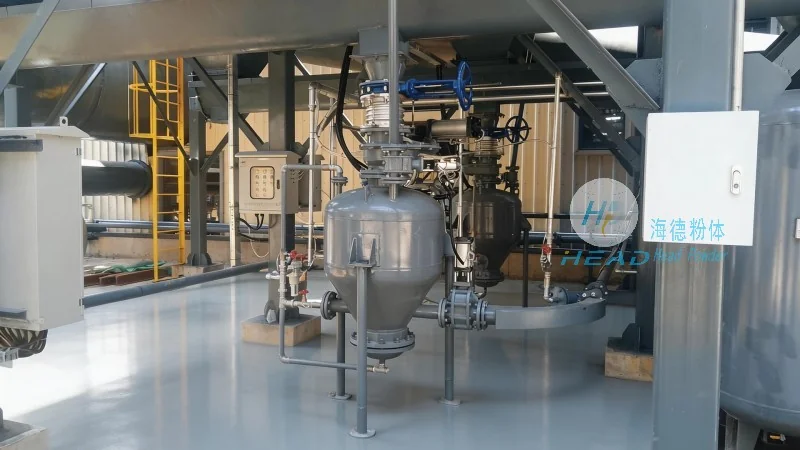
In the food and pharmaceutical industries, where purity and hygiene are paramount, pneumatic conveying systems are preferred for their enclosed design and ability to maintain product integrity. HeadPowder’s solutions are designed to meet stringent sanitary standards, ensuring that calcium carbonate powder remains free from contaminants during transport. This is particularly important in applications where the powder is used as an ingredient in food products or as a filler in pharmaceutical formulations, where any impurity could affect the final product’s quality and safety.
Calcium carbonate powder pneumatic conveying represents a significant advancement in material handling technology, offering a combination of efficiency, environmental responsibility, and adaptability. By leveraging the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., industries can implement systems that not only improve operational performance but also align with modern sustainability goals. The benefits of reduced downtime, lower environmental impact, and customized solutions make pneumatic conveying an attractive choice for businesses looking to optimize their calcium carbonate powder handling processes. As the demand for efficient and eco-friendly material handling solutions continues to grow, pneumatic conveying systems remain a key component in the calcium carbonate industry, driving innovation and productivity forward.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top