Fertilizer pneumatic conveying systems are essential in modern agricultural and industrial operations, providing efficient and reliable methods for transporting bulk materials like fertilizers. The technology involves using air pressure or vacuum to move materials through a pipeline network, eliminating the need for traditional mechanical conveyors. This approach not only enhances operational efficiency but also reduces labor costs and minimizes material handling risks.
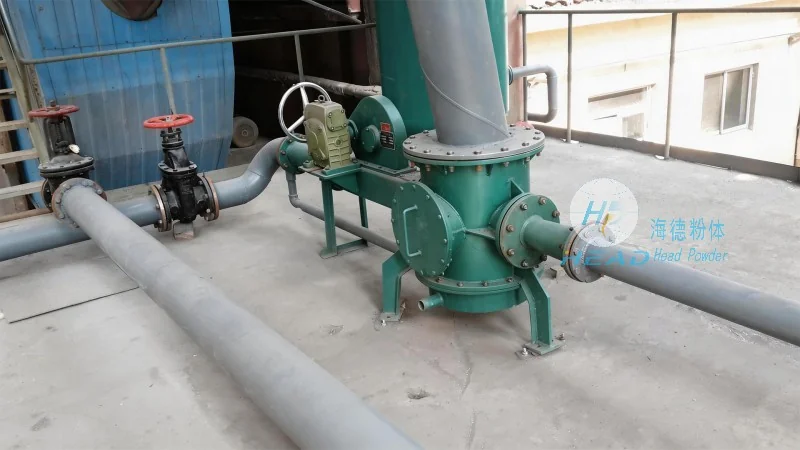
The fundamental principle of pneumatic conveying is the use of air as a medium to transport bulk solids. There are two main types: dilute-phase and dense-phase. Dilute-phase systems use high-velocity air to suspend particles, while dense-phase systems use lower velocities with higher air-to-material ratios to ensure stable flow. The choice between these depends on the material characteristics, such as particle size, density, and moisture content. For fertilizers, which often have varying compositions, the system design must account for these variables to maintain consistent performance.
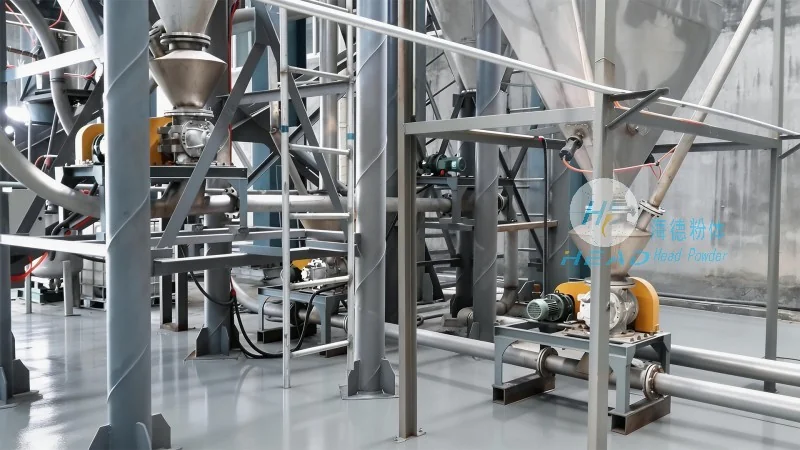
The working scene characteristics of fertilizer pneumatic conveying systems are tailored to specific operational needs. In agricultural settings, these systems are used in farms and fertilizer distribution centers to move raw materials from storage to processing units. The systems are designed to handle large volumes of material, often with high throughput rates, ensuring timely delivery to fields. Industrial applications, such as in chemical plants or manufacturing facilities, utilize these systems for internal material transport, integrating with other production processes. The flexibility of pneumatic conveying allows for integration into existing infrastructure, reducing the need for major construction or layout changes.
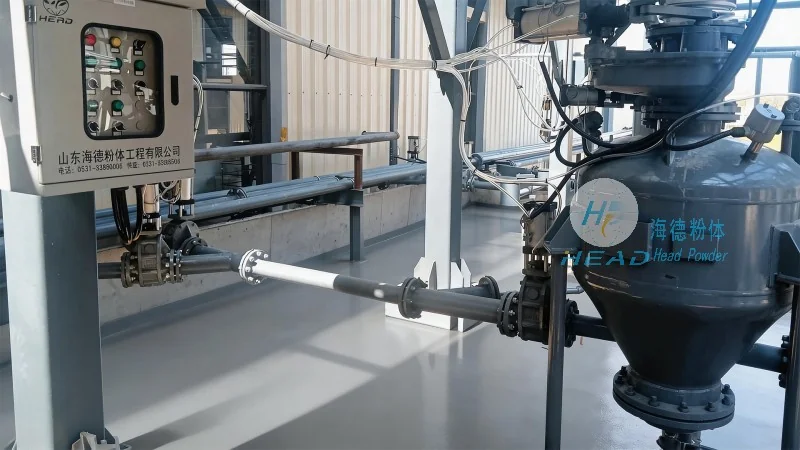
HeadPowder, a leading manufacturer in the field, offers advanced pneumatic conveying solutions tailored to the unique demands of fertilizer handling. Their systems are engineered with precision to ensure optimal performance. Key features include adjustable air pressure controls, which allow operators to fine-tune the conveying process based on material properties. The use of high-quality materials in construction ensures durability and resistance to corrosion, critical for handling fertilizers that may contain acidic or alkaline components. Additionally, the systems are designed for easy maintenance, with accessible components that simplify routine checks and repairs.
In practical applications, fertilizer pneumatic conveying systems demonstrate significant advantages in operational efficiency. For example, in a large-scale fertilizer plant, the system can transport thousands of tons of material per day with minimal downtime. The ability to handle various fertilizer types, from granular to powdered, makes these systems versatile. The reduced need for manual handling also enhances safety, as operators are less exposed to heavy lifting and material exposure. Furthermore, the systems contribute to environmental sustainability by minimizing dust emissions and material loss during transport, aligning with modern industrial standards.
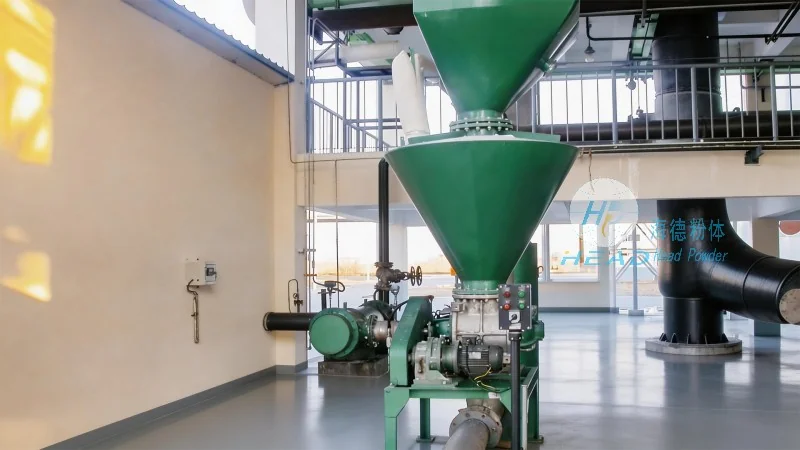
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a reputable company based in Shandong, China. Specializing in the design, manufacturing, and installation of pneumatic conveying systems, the company has established itself as a trusted partner in the agricultural and industrial sectors. With a focus on innovation and customer satisfaction, HeadPowder provides tailored solutions that meet the specific needs of clients. The company’s commitment to quality and reliability has earned it a strong reputation in the market, making it a preferred choice for businesses seeking efficient material handling solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top