White carbon black, a critical industrial material, often requires efficient and reliable transport methods to move it from production sites to processing or packaging areas. Pneumatic conveying stands out as a preferred solution for handling white carbon black due to its ability to transport powders like this material in a controlled, dust-free environment. This article delves into the fundamental principles of white carbon black pneumatic conveying and explores the key characteristics of its working scenes, providing insights into how this technology optimizes material handling in industrial applications. The information is provided by Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions specializing in white carbon black processing and transport systems.
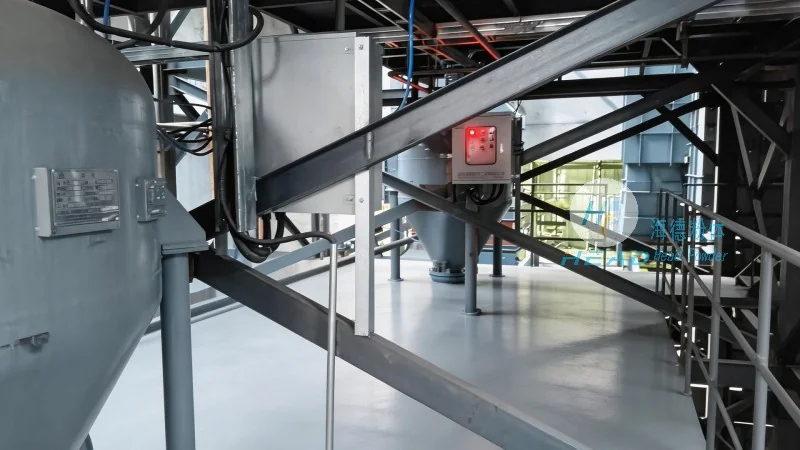
Pneumatic conveying operates on the principle of transporting solid particles, such as white carbon black, using a gas stream, typically air or other gases. The process involves creating a flow of gas that carries the powder through a pipeline. There are two primary types of pneumatic conveying systems: pressure and vacuum systems. In pressure systems, compressed air is introduced at the material feed point, generating a positive pressure that propels the white carbon black through the pipeline. Conversely, vacuum systems use a vacuum pump to create a negative pressure, drawing the material from the source and pulling it toward the destination. The choice between these systems depends on factors like the distance to be covered, the material's properties, and the required flow rate. For white carbon black, which is a fine powder with a high density and potential for agglomeration, pressure systems are often favored as they provide better control over particle movement and reduce the risk of blockages. The conveying process involves several key components, including a hopper or feeder to supply the white carbon black, a pipeline network to transport it, and a receiver or silo to collect the material at the end point. The gas flow rate and pressure are carefully regulated to ensure the white carbon black particles are suspended and transported efficiently without excessive wear on the equipment or degradation of the material.
The working scenes where white carbon black pneumatic conveying is applied vary widely across different industries, each presenting unique challenges and requirements. In the chemical and rubber industries, for instance, white carbon black is commonly used as a filler in rubber compounds and plastic products. Here, pneumatic conveying is essential for moving the material from storage silos to mixing equipment or production lines. The working scene typically involves large-scale production facilities with multiple processing units, requiring continuous and high-volume material transport. The environment in these settings is often characterized by strict cleanliness standards to prevent contamination of the white carbon black, which is sensitive to moisture and other impurities. Pneumatic conveying systems are designed to maintain a dust-free environment, using sealed pipelines and filtration systems to ensure the material remains pure throughout the transport process. Another key working scene is in the pharmaceutical and food industries, where white carbon black is used as an additive or filler in various products. In these sectors, the working scene demands even higher levels of hygiene and safety, as the material may come into contact with end products that are consumed or used in medical applications. The pneumatic conveying systems used here are often equipped with additional features such as air filtration, particle size control, and material drying to meet stringent regulatory requirements. Additionally, in the construction and coating industries, white carbon black is used as a pigment or additive in paints and coatings. The working scene in this context involves smaller-scale operations, often with shorter transport distances, but still requires efficient and reliable transport to ensure consistent product quality. The characteristics of the working scene here include lower material flow rates and the need for flexible conveying solutions that can adapt to varying production schedules.
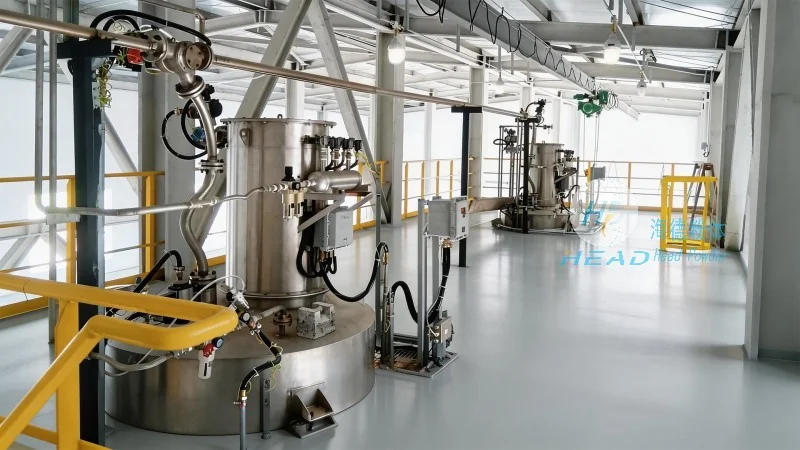
The effectiveness of white carbon black pneumatic conveying is influenced by several critical factors that must be carefully considered during system design and operation. Particle size and density are among the most important properties of white carbon black, as they directly impact the gas flow requirements and the risk of blockages. Fine white carbon black particles, which are common in many applications, require higher gas velocities to remain suspended in the pipeline, increasing energy consumption but ensuring efficient transport. Conversely, larger particles may settle more quickly, leading to reduced conveying efficiency and potential system downtime. The moisture content of the white carbon black is another critical factor, as high moisture levels can cause agglomeration, making the material more difficult to transport. Pneumatic conveying systems often include drying stages or moisture control mechanisms to maintain optimal material properties. The pipeline design, including diameter, length, and bends, also plays a significant role in conveying performance. Longer pipelines or those with numerous bends increase pressure drop and energy consumption, while larger diameter pipelines reduce friction losses but may require more space and higher material costs. The choice of materials for the pipeline and equipment, such as stainless steel or special alloys, is essential to prevent corrosion and wear from the abrasive white carbon black particles. Regular maintenance and monitoring of the system are also crucial to ensure consistent performance and prevent issues like clogging or equipment failure. By addressing these factors, manufacturers can optimize the pneumatic conveying system for white carbon black, achieving efficient, reliable, and cost-effective material transport.
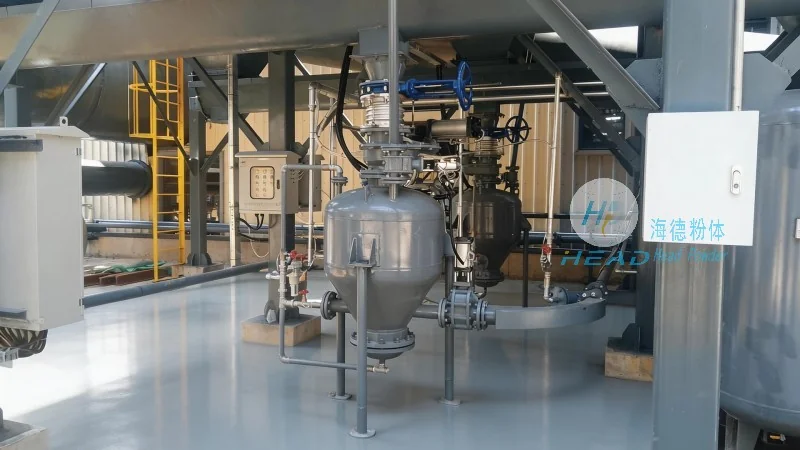
White carbon black pneumatic conveying finds extensive applications across various industries, offering numerous benefits that enhance operational efficiency and product quality. In the rubber industry, for example, pneumatic conveying is used to transport white carbon black to mixing machines, where it is blended with rubber compounds to improve the mechanical properties of the final product. The benefits of this method include reduced labor costs, as automated systems handle the material transport, and improved product consistency, as the material is delivered in a controlled manner without manual handling. In the chemical industry, pneumatic conveying is used to move white carbon black from storage to reaction vessels or processing units, where it serves as a reactant or additive. The benefits here include faster processing times and reduced exposure of workers to the material, improving workplace safety. The pharmaceutical industry also relies on pneumatic conveying for handling white carbon black in the production of medications and supplements. The benefits include maintaining a sterile environment, preventing contamination, and ensuring the material is delivered in a consistent particle size, which is critical for product efficacy. In the food industry, where white carbon black is used as a food additive, pneumatic conveying helps maintain the material's purity and prevents cross-contamination with other ingredients. The benefits include improved product safety and compliance with regulatory standards. Overall, the applications of white carbon black pneumatic conveying are diverse, and the benefits extend beyond material transport to include cost savings, improved safety, and enhanced product quality. By leveraging this technology, industries can achieve more efficient and reliable operations, meeting the demands of modern manufacturing.
In conclusion, white carbon black pneumatic conveying is a sophisticated and effective method for transporting this critical industrial material. The principles of pneumatic conveying, combined with tailored working scene characteristics, enable efficient and reliable material handling across various industries. The key factors influencing performance, such as particle properties, pipeline design, and system maintenance, must be carefully managed to ensure optimal results. The applications and benefits of this technology highlight its importance in modern industrial operations, from chemical and rubber production to pharmaceutical and food processing. As industries continue to seek more efficient and sustainable material transport solutions, white carbon black pneumatic conveying remains a valuable and versatile option. By understanding its principles and working scene characteristics, manufacturers can optimize their material handling processes, improving productivity and product quality while maintaining safety and compliance standards.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top