HeadPowder, a leading provider of industrial material handling solutions, specializes in advanced pneumatic conveying systems designed for the efficient transport of activated carbon granular materials. This article explores the working principle and key features of such systems, highlighting their applications and benefits in various industrial settings.
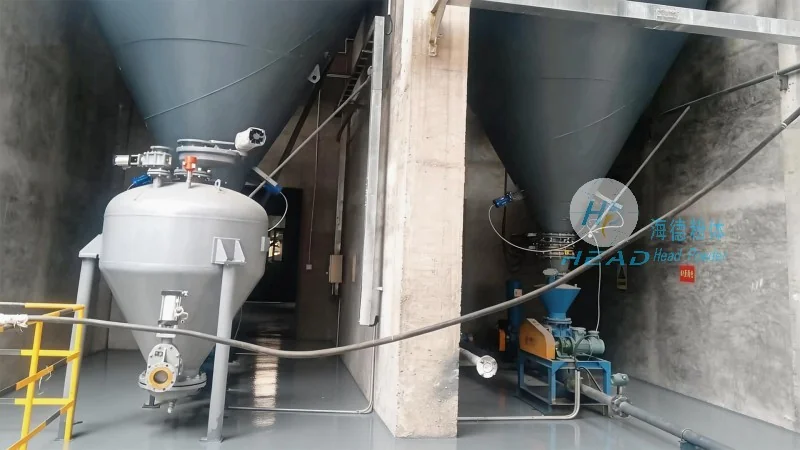
Activated carbon granular material pneumatic conveying systems are essential in industries requiring the safe and efficient transport of activated carbon, a critical adsorbent used in water treatment, air purification, and chemical processing. These systems utilize air or gas as the conveying medium to move granular materials through pipelines, eliminating the need for traditional mechanical conveying methods like belt conveyors or screw conveyors. The technology offers significant advantages in terms of hygiene, contamination control, and operational flexibility.
The core working principle of activated carbon granular material pneumatic conveying systems involves the use of a pressure or vacuum source to generate airflow within a pipeline. The system typically consists of a hopper, a feeder, a conveying line, and a receiver. The process begins with the activated carbon granules being fed into the hopper from a storage silo. The feeder then controls the flow rate of the material into the conveying line. As the material enters the pipeline, the airflow, either under positive pressure (pressure conveying) or negative pressure (vacuum conveying), propels the granules forward. The velocity of the air must be sufficient to overcome the gravitational and frictional forces acting on the particles, ensuring stable and continuous transport. The receiver at the end of the line collects the conveyed material, completing the cycle.
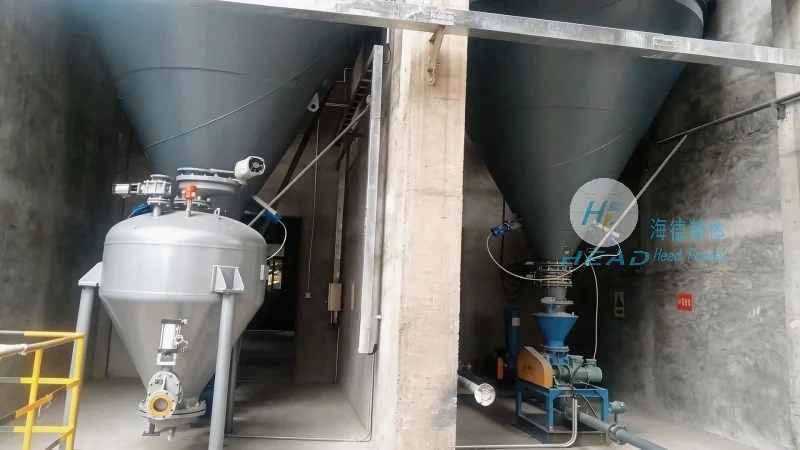
Activated carbon granular material pneumatic conveying systems offer several distinct features and advantages that make them ideal for industrial applications:
These systems are capable of transporting large volumes of activated carbon granules at high speeds, often achieving throughput rates that exceed those of traditional mechanical conveyors. The ability to handle high capacities without the need for multiple transfer points reduces operational downtime and increases overall productivity.
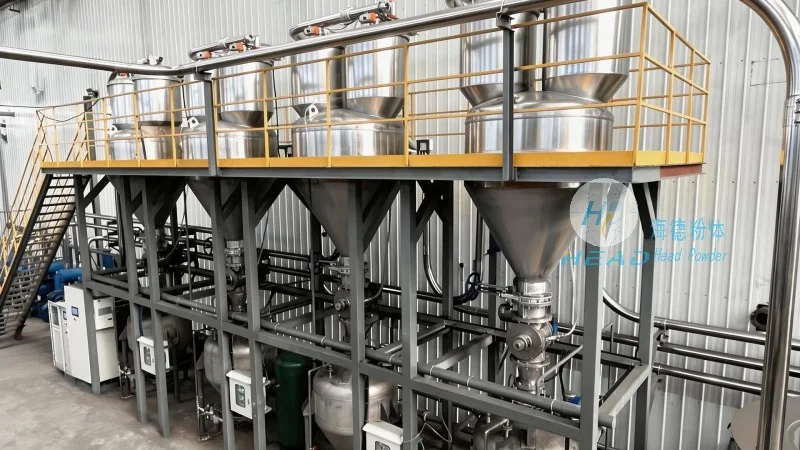
Pneumatic conveying systems are enclosed, preventing dust and particles from escaping into the environment. This is particularly important for activated carbon, which is used in applications where purity and contamination control are critical, such as in pharmaceutical and food processing industries. The enclosed design also ensures that the material remains free from external contaminants, maintaining its adsorption properties.
The modular design of pneumatic conveying systems allows for easy integration into existing production lines and facilities. The conveying lines can be configured in various shapes and directions, enabling the system to adapt to different plant layouts and space constraints. This flexibility also facilitates the addition of new processing stages or the expansion of production capacity without major structural modifications.
Compared to mechanical conveyors, pneumatic systems have fewer moving parts, which reduces the risk of wear and tear and lowers maintenance requirements. The enclosed design minimizes the need for cleaning and maintenance, as there are no exposed components that can accumulate dust or debris. Additionally, the energy efficiency of modern pneumatic conveying systems contributes to lower operational costs over time.
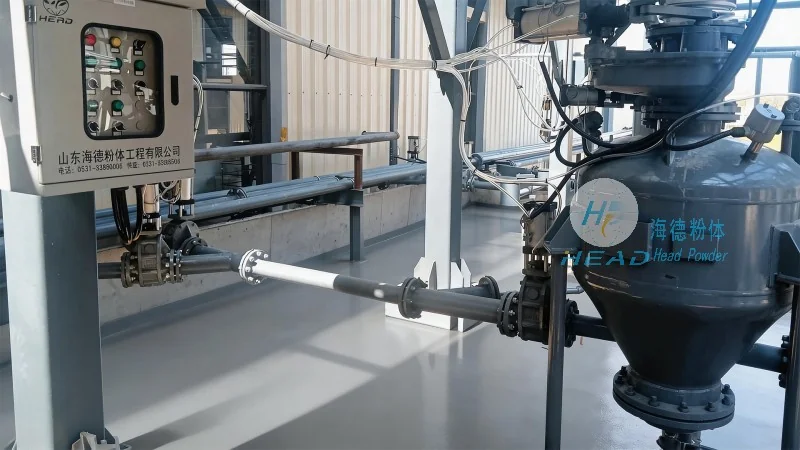
Activated carbon granular material pneumatic conveying systems are widely used in various industries where the transport of activated carbon is essential. These include water treatment plants, where activated carbon is used for removing impurities and contaminants from drinking water and industrial wastewater; air purification systems, such as in industrial facilities and chemical plants, to filter and purify air; and chemical processing industries, where activated carbon is used as a catalyst or adsorbent in various chemical reactions and processes.
Activated carbon granular material pneumatic conveying systems, provided by companies like Shandong HeadPowder Engineering Co., Ltd., represent a sophisticated and efficient solution for the transport of activated carbon. By leveraging the principles of pneumatic conveying, these systems offer high efficiency, hygienic operation, and flexibility, making them a preferred choice for industries requiring reliable and cost-effective material handling solutions. The continued advancement of technology in this field ensures that such systems will remain a vital component of modern industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top